എക്സിക്യൂട്ടീവ് സമ്മറി
Packaging bulky rectangular block products—ranging from furniture components and acoustic foam billets to high-density mattress panels—presents persistent line bottlenecks when done manually. Hand wrapping invariably yields inconsistent film overlap, loose tail ends, trapped air pockets, and uneven package integrity across work shifts. This automated line eliminates manual variance through a continuous four-stage sequence: heavy-duty roller conveyor infeed, synchronized multi-axis film application, integrated top-press stabilization, and a calibrated hot-air shrink tunnel. Designed specifically for rigid, semi-rigid, and compressible rectangular items, the system applies uniform tension and balanced thermal exposure across all faces to output high-integrity, pallet-ready blocks. Project-specific parameters, machine dimensions, and film specifications are tailored to match targeted block sizing and throughput requirements.
ഉള്ളടക്ക പട്ടിക
- ബ്ലോക്ക് ഉൽപ്പന്നങ്ങൾ പാക്ക് ചെയ്യാൻ ബുദ്ധിമുട്ടായിരിക്കുന്നത് എന്തുകൊണ്ട്?
- ലൈൻ എങ്ങനെ പോകുന്നു
- റോളർ കൺവെയർ വഴി ഇൻഫീഡ് ചെയ്യുക
- ഫിലിം പ്രയോഗിക്കുന്നു
- സ്റ്റേഷൻ അമർത്തി ചുരുക്കുക
- ചൂടാക്കിയ ഷ്രിങ്ക് ടണൽ
- സാധാരണ കോൺഫിഗറേഷൻ
- വീഡിയോ എന്താണ് കാണിക്കുന്നത്
- തിരഞ്ഞെടുക്കൽ ചെക്ക്ലിസ്റ്റ്
- പ്രവർത്തനവും സുരക്ഷയും
- എഞ്ചിനീയറിംഗ് പതിവ് ചോദ്യങ്ങൾ
- അടുത്ത പടി
- അനുബന്ധ വായന
- ഉറവിടങ്ങളും മാനദണ്ഡങ്ങളും
ബ്ലോക്ക് ഉൽപ്പന്നങ്ങൾ പാക്ക് ചെയ്യാൻ ബുദ്ധിമുട്ടായിരിക്കുന്നത് എന്തുകൊണ്ട്?
Furniture assemblies, engineered foam blocks, insulation slabs, and mattress cores are bulky, heavy, and awkward to handle. Many feature soft, compressible edges combined with broad surface areas. When wrapped manually using handheld stretch film dispensers or stationary heat guns:
- Excessive operator dependency: Film tension varies widely across operators and work shifts. One package might have excessive edge tension that crushes structural foam corners, while the next has loose film tails that snag on transfer conveyors.
- Trapped air and bulk volume: Large rectangular products trap substantial air within the wrapping boundary. Without mechanical top-pressing during sealing, the trapped volume prevents tight shrink wrap, resulting in ballooned packages that shift during stacking.
- Transport scuffing and moisture ingress: Loose film slips during long-distance logistics. Friction against trailer walls or wooden pallets creates surface scuffing on delicate painted surfaces or fabric upholstery, while unsealed seams allow dust and moisture to degrade core materials.
The automated block packaging line eliminates these inconsistencies by enforcing repeatable mechanical feeding, controlled pneumatic pre-pressing, and precise thermal air-distribution around every product.
ലൈൻ എങ്ങനെ പോകുന്നു
The automated system routes each rectangular block continuously through four dedicated workstations without requiring manual intervention during the main packing cycle:
- ഇൻഫീഡ് ട്രാൻസ്ഫർ: The incoming block aligns onto a motorized live-roller bed, indexed by optical sensors for square, centered presentation.
- Film Enclosure: Low-friction feed carriages lay polyethylene (PE) or polyolefin (POF) film cleanly over the top, bottom, and lateral faces with regulated unwind tension.
- Pneumatic Press & Seal: An overhead pneumatic platen compresses the block to evacuate internal air while a hot-knife sealing bar trims and joins the film perimeter.
- Thermal Shrink Tunnel: High-velocity recirculating air heats the film uniformly to shrink tension, locking tightly over every flat surface and corner edge.
Because machine parameters are preset in the central PLC, each cycle delivers identical structural containment, cycle time, and aesthetic finish regardless of production shifts.
റോളർ കൺവെയർ വഴി ഇൻഫീഡ് ചെയ്യുക
The infeed section utilizes heavy-duty powered roller conveyors configured to handle payloads ranging from lightweight expanded polystyrene (EPS) to high-density wooden cabinets weighing up to 250 kg.
- റോളർ നിർമ്മാണം: Zinc-plated or polyurethane-sleeved carbon steel rollers prevent marring on pre-finished furniture panels while providing high frictional drive for consistent tracking.
- Positive Indexing: Integrated photoelectric gate sensors detect the leading edge of the block to regulate conveyor speeds (typically 5 to 15 m/min via variable-frequency drive), ensuring synchronized handoff to the downstream film wrapping station.
- Centering Guides: Adjustable side-guide rollers align off-center products with the machine center line, avoiding asymmetrical film distribution.
ഫിലിം പ്രയോഗിക്കുന്നു
At the film station, roll-fed shrink film is applied around the advancing block. The mechanical carriage feeds film smoothly over the top, leading, and trailing faces, establishing the primary envelope:
- Tension-Controlled Unwind: Magnetic particle or pneumatic friction brakes maintain consistent web tension across the entire roll diameter, preventing film wrinkling or tears along sharp corners.
- Full-Enclosure Coverage: The cross-sealing and vertical feed system places enough film slack around oversized blocks to accommodate height variations while avoiding excessive waste margins.
- Base Foundation for Shrinking: Uniform lateral film tension ensures that when the package enters the heating zone, the shrink percentage translates directly into structural clamping force rather than irregular, twisted seam lines.
സ്റ്റേഷൻ അമർത്തി ചുരുക്കുക
Immediately following the film placement, the product enters an integrated press station. This assembly stabilizes compressible products and pre-tacks the film boundary:
- Pneumatic Top Platen: A guided overhead pressure plate descends with adjustable pneumatic force (0.2 to 0.5 MPa). For compressible blocks like polyurethane foam or mattress cores, this press evacuates trapped air pockets and flattens uneven crowns.
- Tension Stabilization: By pressing the film flush against the horizontal panels before and during perimeter sealing, the station prevents thermal ballooning inside the heating tunnel.
- Taut Package Execution: The press ensures the film remains fully taut across all faces, eliminating baggy wrinkles and forming tight, balanced seals along the neutral center axis of the block.
ചൂടാക്കിയ ഷ്രിങ്ക് ടണൽ
After perimeter sealing and stabilization, the package enters the recirculating hot-air shrink tunnel. This chamber supplies the thermal energy required to activate the film’s bidirectional memory:
- Dual-Directional Airflow: Blower turbines force heated air through adjustable side and bottom nozzles, delivering balanced thermal convection around all six faces of the block simultaneously.
- Precise Temperature Regulation: Digital PID controllers maintain internal air temperature within ±2 °C (typically set between 130 °C and 180 °C, depending on whether 40–80 µm PE or heavy-duty POF is specified).
- Controlled Dwell Time: Mesh conveyor or silicone-sleeved roller chains advance the product through the tunnel at a continuous pace, giving the film adequate time to draw tight over structural edges without burning or puncturing soft foam substrates.
The block emerges from the cooling tunnel discharge fully encapsulated, dimensionally rigid, and ready for immediate stacking or automated robotic palletizing.
സാധാരണ കോൺഫിഗറേഷൻ
The table below outlines common engineering parameters and operational ranges for our rectangular block shrink packaging installations:
| സിസ്റ്റം പാരാമീറ്റർ | സാധാരണ എഞ്ചിനീയറിംഗ് ശ്രേണി | പ്രവർത്തനപരമായ ഉദ്ദേശ്യം |
|---|---|---|
| അനുയോജ്യമായ ഉൽപ്പന്നങ്ങൾ | Mattresses, foam blocks, furniture, panels | Rectangular geometries with flat surfaces |
| Max Block Width | 600 mm – 1600 mm (project-matched) | Determines sealing jaw width and tunnel clearance |
| Max Block Height | 100 മില്ലീമീറ്റർ - 600 മില്ലീമീറ്റർ | Sets overhead platen stroke and tunnel chamber height |
| കൺവെയർ സ്പീഡ് | 5 – 15 m/min (variable speed) | Synchronizes throughput with plant production flow |
| ഫിലിം മെറ്റീരിയൽ | PE flat film / POF shrink film (40–100 µm) | Heavy-duty puncture resistance and moisture barrier |
| ടണൽ താപനില | 120 °C – 190 °C (PID adjustable) | Delivers balanced multi-face shrink ratio |
| Overhead Press Force | 500 N – 3500 N (pneumatic, regulated) | De-airs compressible foam and locks film stability |
| വൈദ്യുത വിതരണം | 380 V / 415 V, 3-ഫേസ്, 50/60 Hz | Main system drive and tunnel heating power |
| എയർ ഉപഭോഗം | 0.5 – 0.7 MPa, 150 – 300 NL/min | Powers pneumatic platen cylinders and seal cutters |
വീഡിയോ എന്താണ് കാണിക്കുന്നത്
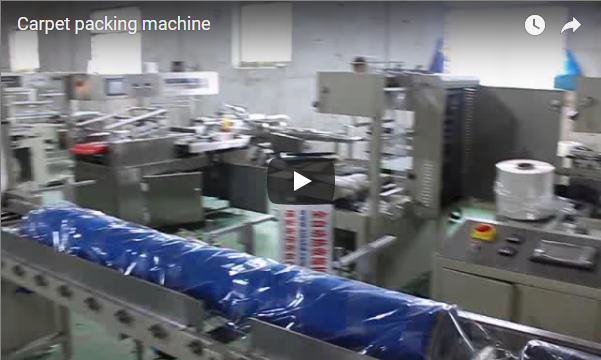
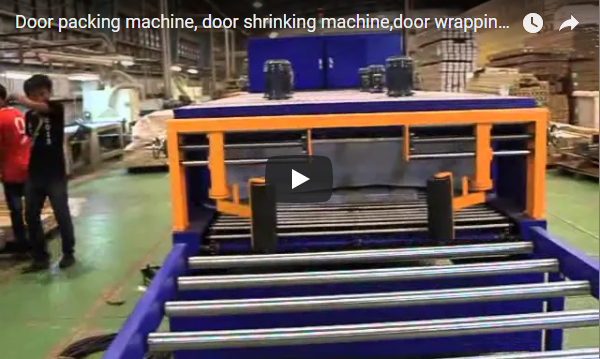
The accompanying demonstration video showcases a complete automatic shrink packaging line configured for large rectangular block components:
- Automatic Conveyance & Registration: Demonstrates how rectangular items travel smoothly on the live roller bed and pause precisely at the sealing zone.
- Top-Press Downstroke: Illustrates the overhead pneumatic press plate depressing the top face of the block, firmly holding it flat while the heated impulse sealing bar cuts and seals the film envelope.
- Tunnel Shrinking Action: Shows the continuous transition into the heated tunnel chamber, highlighting the immediate contraction of the film as recirculated convective air pulls the loose covering into a taut, glass-clear outer barrier.
- Discharge Finish: Concludes with the finished block moving onto the exit conveyor, showing uniform, puncture-resistant edge wrap and secure seam integrity on every corner.
തിരഞ്ഞെടുക്കൽ ചെക്ക്ലിസ്റ്റ്
Use this engineering checklist when scoping an automated block shrink line for your production facility:
| മൂല്യനിർണ്ണയ ഇനം | സ്ഥിരീകരിക്കേണ്ട പാരാമീറ്റർ | എഞ്ചിനീയറിംഗ് പരിഗണന |
|---|---|---|
| Block Dimensions (L × W × H) | Minimum and maximum values (mm) | Dictates tunnel aperture size and platen cylinder stroke |
| Compressibility & Rigidity | Rigid board vs. flexible open-cell foam | Determines required pneumatic press cylinder bore and pressure range |
| ഉൽപ്പന്ന ഭാര പരിധി | Minimum to maximum unit mass (kg) | Confirms conveyor roller pitch, shaft diameter, and gearmotor kW |
| ഫിലിം കെമിസ്ട്രി & ഗേജ് | PE, POF, or barrier films (thickness in µm) | Dictates heating element wattage, tunnel length, and seal-wire coatings |
| Target Output Rate | Blocks per minute / hour | Determines conveyor drive velocity and tunnel dwell time |
| Plant Power & Utilities | Operating voltage, phase, pneumatic line flow | Ensures full compatibility with existing factory infrastructure |
പ്രവർത്തനവും സുരക്ഷയും
The packaging line is operated via a centralized Siemens or Delta PLC touchscreen HMI. Standard recipe storage allows operators to switch between different block heights and lengths with single-touch automatic adjustments.
- യന്ത്ര സുരക്ഷാ മാനദണ്ഡങ്ങൾ: Built in strict compliance with ISO 12100:2010 and EN 415-4/10 standards for packaging machinery.
- ചുറ്റളവ് സംരക്ഷണവും ഇന്റർലോക്കുകളും: Transparent polycarbonate access panels and perimeter wire mesh prevent operator contact with heated tunnel components and moving sealing jaws.
- സുരക്ഷാ ലൈറ്റ് കർട്ടനുകൾ: Optical curtains (Category 4, PL e per EN ISO 13849-1) monitor infeed and outfeed openings; breaking the optical beam immediately cuts pneumatic and drive power to hazardous moving assemblies.
- അടിയന്തര സ്റ്റോപ്പ് പ്രോട്ടോക്കോൾ: Hardwired E-stop pushbuttons are placed at the primary HMI station, sealing station, and tunnel exit to trigger instantaneous fail-safe pneumatic venting and mechanical braking.
എഞ്ചിനീയറിംഗ് പതിവ് ചോദ്യങ്ങൾ
Q: Can this line handle both rigid furniture panels and soft, compressible foam blocks? A: Yes. The pneumatic top-press station includes a precision pressure regulator and variable stroke limiters. For rigid panels, it acts as a light clamp (0.1–0.2 MPa) to prevent product movement during sealing; for soft foam or mattress cores, pressure can be increased (up to 0.5 MPa) to evacuate internal air before heating.
Q: Why is an overhead press station necessary prior to the heat tunnel? A: Large rectangular surfaces trap substantial air inside the sealed film envelope. If an unpressed, air-filled package enters the heated tunnel, the expanding hot air resists film contraction, producing large loose pockets and ballooning. Pre-pressing ensures the film remains fully taut and the package remains compact.
Q: What film materials are compatible with this system? A: The system supports both Low-Density Polyethylene (LDPE, 40 to 100 µm) for heavy-duty, scuff-resistant protection and Polyolefin (POF, 19 to 35 µm) for high-clarity retail presentations.
Q: How does the tunnel prevent soft products from melting or deforming? A: The shrink tunnel utilizes high-velocity air circulation rather than static radiant heat. Adjustable louvers direct hot air along the outer film boundaries rather than concentrating heat on the product core. In addition, an automatic outfeed conveyor ejects packages immediately if downstream line stoppages occur.
ചോദ്യം: എന്ത് പതിവ് അറ്റകുറ്റപ്പണികൾ ആവശ്യമാണ്? A: Daily inspections include cleaning the Teflon coating on the sealing jaws and wiping photo-eye sensors. Weekly tasks involve inspecting pneumatic cylinder seals, checking drive chain tension, and cleaning the tunnel intake air filters to ensure unimpeded air circulation.
അടുത്ത പടി
- ഉൽപ്പന്ന സ്പെസിഫിക്കേഷനുകൾ സമർപ്പിക്കുക: Email your exact block dimensional matrix (minimum and maximum L × W × H), unit weights, and daily throughput targets to info@fhopepack.com.
- Engineering Review & 2D/3D Layout: Our mechanical design team will generate a customized packaging line proposal and plant layout drawing within 48 hours.
- ഫാക്ടറി സ്വീകാര്യതാ പരിശോധന (FAT): Ship sample blocks to our technical center for film trial evaluation, seam-integrity burst testing, and complete cycle-time verification.
അനുബന്ധ വായന
- പാനലിലും വാതിലിലും ഓട്ടോമാറ്റിക് ഫിലിം സീലിംഗ് മെഷീൻ
- പ്ലേറ്റുകൾക്കായുള്ള ഓട്ടോമാറ്റിക് ഷ്രിങ്ക് പാക്കേജിംഗ് മെഷീൻ
- ഓട്ടോമാറ്റിക് പാനൽ ഷ്രിങ്ക് പാക്കിംഗ് മെഷീൻ
- FHOPE പാക്കിംഗ് മെഷിനറി ഉൽപ്പന്ന ലൈനുകൾ
ഉറവിടങ്ങളും മാനദണ്ഡങ്ങളും
- ISO 12100:2010 യന്ത്രങ്ങളുടെ സുരക്ഷ — രൂപകൽപ്പനയ്ക്കുള്ള പൊതു തത്വങ്ങൾ — അപകടസാധ്യത വിലയിരുത്തലും അപകടസാധ്യത കുറയ്ക്കലും
- EN 415-4: Safety of packaging machines — Palletisers and depalletisers, formers, and shrink wrappers
- EN 415-10:2014 പാക്കേജിംഗ് മെഷീനുകളുടെ സുരക്ഷ - പൊതുവായ ആവശ്യകതകൾ
- EN ISO 13849-1:2023 യന്ത്രങ്ങളുടെ സുരക്ഷ — നിയന്ത്രണ സംവിധാനങ്ങളുടെ സുരക്ഷയുമായി ബന്ധപ്പെട്ട ഭാഗങ്ങൾ
FHOPE automatic block packaging and shrinking line technical specification document. Tailored layout and machine parameters confirmed per project application.
അവസാനം അവലോകനം ചെയ്തത്: 2026-10-10