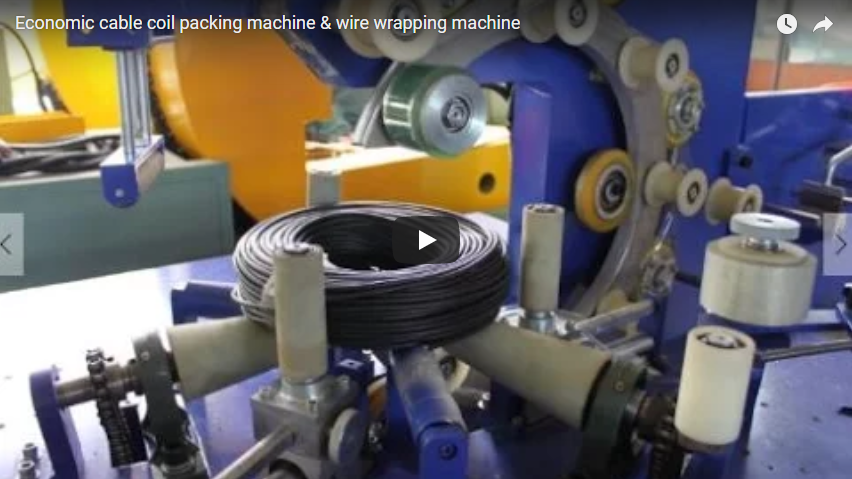
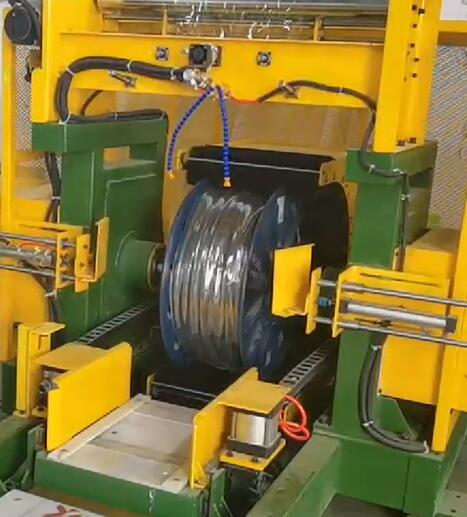
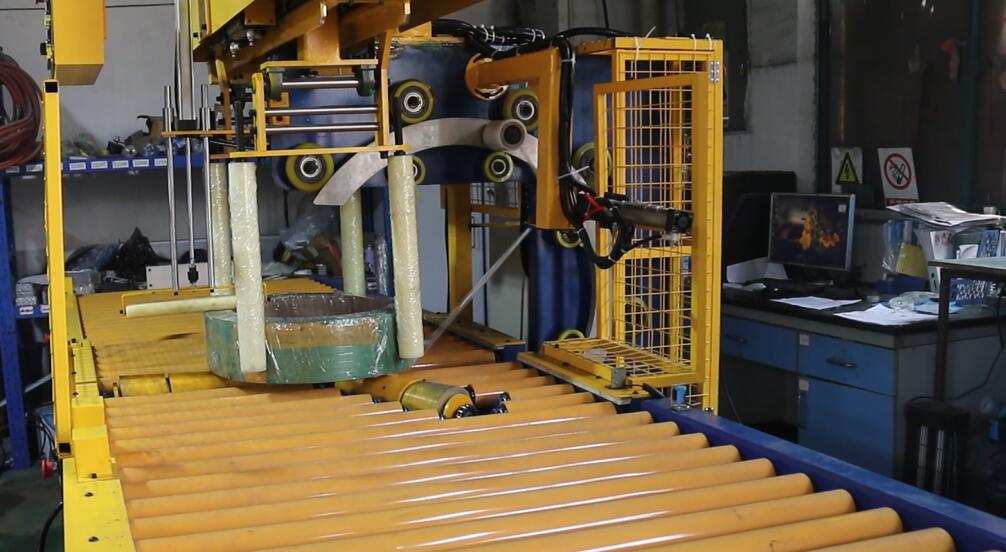
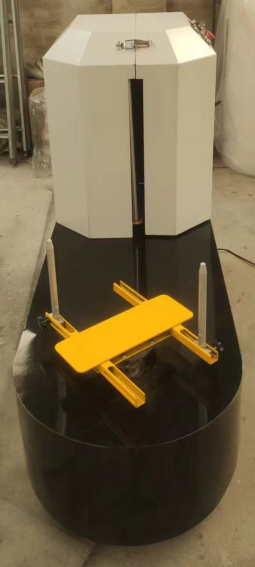
Kopsavilkums Mūsu horizontālā kabeļu ruļļu iepakošanas mašīna tin ruļļus, kas novietoti pret debesīm, sākot no 90 mm iekšējais diametrs. It handles wire and cable coils weighing 2–30 kg with an outer diameter (OD) of 150–400 mm, achieving a cycle time of 18–30 s uz spoli. Four synchronized electric centring arms align the coil precisely under the vertical wrapping ring, while an overhead pneumatic press-down roller secures the package during orbital rotation. Stored PLC recipes allow a single operator to execute rapid size changeovers without tooling adjustments.
Saturs
- Kāpēc maza ID diametra kabeļu spoles ir grūti ietīt
- Kā darbojas mūsu horizontālā kabeļu spoļu iepakošanas mašīna
- Maza ID kabeļu spoļu iepakošanas mašīnas specifikācijas
- Cikla laiks un gredzena ātrums: ātra pārbaude
- Pārslēgšanās starp kabeļu izmēriem
- Kabeļu un vadu spoļu iepakojuma materiāls
- Vadības ierīces un drošība
- Maza ID kabeļu ruļļu iepakošanas iekārtas izvēles kontrolsaraksts
- Inženierijas bieži uzdotie jautājumi
- Nākamais solis
- Saistītā lasāmviela
- Avoti
Kāpēc maza ID diametra kabeļu spoles ir grūti ietīt
On an eye-through orbital wrapper, the rotating ring and its carriage-mounted film roll must traverse the open coil center on every cycle. A narrow eye leaves minimal physical clearance between the inner ring face, the film dispenser, and the coil inner wall.
Building wire (such as THHN/THWN), automotive harness wire, communication cables, and flexible hydraulic hoses are routinely packaged in compact coils with an inner diameter (ID) under 100 mm. Conventional ring wrappers frequently suffer orbital collisions or film tear due to oversized film carriage assemblies.
We engineered the FPCA-100 specifically to solve this physical clearance bottleneck. Featuring a low-profile orbital shuttle and offset film-dispenser geometry, the machine wraps coils with an inner diameter down to 90 mm, while accommodating larger coils up to 250 mm iekšējais diametrs on the identical workstation.
Kā darbojas mūsu horizontālā kabeļu spoļu iepakošanas mašīna
The coil rests horizontally (eye to sky) on heavy-duty motorized supporting rollers, while a vertical ring orbits through the center eye to apply protective film radially.
The loading and wrapping sequence runs predictably: the operator loads the bare coil onto the cradle rollers, the motorized radial arms center the coil along the ring centerline, the overhead press-down device clamps the workpiece to prevent tilt, and the orbital ring executes the wrapping sequence. The machine integrates five primary engineered assemblies:
- Atbalsta veltņi. Dual polyurethane-coated (PU) drive rollers rotate the coil 360° continuously about its vertical axis without scuffing delicate outer jackets.
- Centrējošās sviras. Four electric radial arms adjust synchronously to the coil outer diameter, locking the physical geometric center to the ring centerplane.
- Nospiešanas ierīce. A top-mounted pneumatic roller applies regulated clamping force, holding the coil flat against rotational chatter and acceleration torque.
- Ietīšanas gredzens. High-traction PU friction-drive wheels drive an aluminum orbital ring carrying stretch film, woven tape, or PVC material.
- Rotary encoder. Optical encoders track roller surface displacement and ring positioning, maintaining an exact wrapping overlap pitch throughout the batch.
Automatic film clamp-and-cut mechanisms eliminate manual intervention during wrapping cycles. The operator solely manages station loading and unloading.
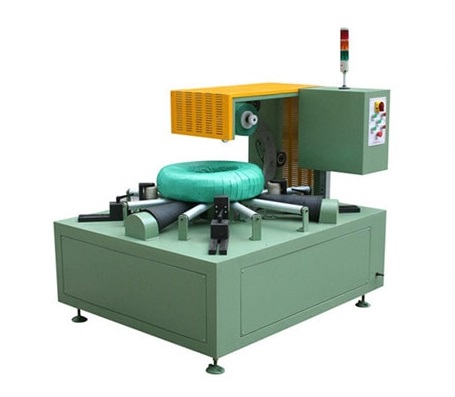
Maza ID kabeļu spoļu iepakošanas mašīnas specifikācijas
| Parametrs | Standarta specifikācija | Inženiertehniskās piezīmes |
|---|---|---|
| Spoles iekšējais diametrs (ID) | 90–250 mm | Minimum clearance profile on film dispenser |
| Spoles ārējais diametrs (OD) | 150–400 mm | Covered by synchronized centring stroke |
| Spoles platums/augstums | 50–180 mm | Regulated via pneumatic hold-down stroke |
| Spoles svara diapazons | 2-30 kg | Continuous support rating on PU rollers |
| Gredzena rotācijas ātrums | 10–120 apgr./min | Inverter-controlled (VFD) stepless regulation |
| Iepakojuma cikla laiks | 18–30 s uz spoli | Size, wrap layers, and overlap dependent |
| Pārklāšanās attiecība | 20% līdz 90% | Programmable via HMI touchscreen |
| Instalēta jauda | 1.8 kW | AC 380 V / 415 V / 480 V (50/60 Hz, 3-Phase) |
| Pneimatiskā padeve | 0.5–0.7 MPa | Clean, dry industrial compressed air |
Cikla laiks un gredzena ātrums: ātra pārbaude
The orbital ring speed, coil peripheral drive ratio, and programmed overlap determine the total cycle duration. The advance rate per ring turn governs overall outer layer density:
- Effective turns per cycle. Operating at a ring speed of 120 r/min, the machine completes 2 orbital revolutions per second. Accounting for ramp-up, ramp-down, and automatic film cutoff, an average 25-second active cycle delivers approximately 40 to 45 steady-state wrap turns.
- Outer circumference displacement. A 400 mm OD coil presents an outer perimeter of
π × 400 mm ≈ 1,257 mm. - Linear advance per orbital turn. At 45 effective turns per cycle, outer linear advance equals
1,257 mm ÷ 45 turns ≈ 28 mmper ring revolution. To ensure seamless weatherproofing and bundle cohesion, the applied film width must exceed this advance rate by the target overlap margin. - Inner diameter overlap behavior. At the 90 mm eye, the inner circumference is only
π × 90 mm ≈ 283 mm. Over the identical 45 turns, the inner surface advances merely283 mm ÷ 45 turns ≈ 6.3 mmper revolution.
Because inner advance is inherently four times tighter than the perimeter, overlap calculations must always be based on the maximum outer diameter (OD). If the outer diameter achieves a 30% overlap, the inner eye will naturally experience high-density multi-ply reinforcement. Smaller coils (e.g., 200 mm OD) require fewer turns and regularly complete in 18 to 20 seconds.
Pārslēgšanās starp kabeļu izmēriem
Wiring production lines frequently change stock keeping units (SKUs) across shifts. The FPCA-100 streamlines product changeover down to under 60 seconds through three core features:
- Stored PLC recipes. The operator selects the cable part number on the Siemens/Delta HMI. Pre-programmed parameters immediately load ring speed, roller RPM, tension, and overlap percentage.
- Electric motorized centring. Four radial arms reposition symmetrically via an electric lead-screw drive to the pre-set OD/ID geometry, eliminating manual hand-wheel adjustments.
- Encoder-based feedback. Closed-loop encoder monitoring ensures immediate synchronization between coil rotation and ring position without physical trial runs.
This automated recipe architecture eliminates operator guesswork and ensures consistent package integrity across shift changes.
Kabeļu un vadu spoļu iepakojuma materiāls
The wrapping assembly accommodates a wide spectrum of packaging films depending on transport demands:
- LLDPE elastīgā plēve: 15–35 µm thickness, standard width 50–100 mm. Ideal for general dustproofing, optical clarity, and moisture barrier protection.
- PVC / PE Stretch Tape: Applied for rigid bundling and enhanced friction resistance against inter-coil abrasion.
- Woven Polypropylene (PP) / Crepe Paper: Used when heavy mechanical puncture protection or export shipping resistance is required.
Surface overlap can be set between 20% and 90% directly from the touchscreen to match specific logistics handling requirements.
Vadības ierīces un drošība
Operator safety and machine longevity are prioritized through integrated electrical and mechanical interlocks:
- Drive Protection: Inverters feature thermal overload and overcurrent trips. Any system jam triggers an instantaneous controlled stop accompanied by an audible stack-light alarm and visual fault diagnostics on the HMI.
- Mechanical Guarding: The orbital ring and friction drive assembly are enclosed within safety sheet-metal panels with perimeter access interlocking.
- Atbilstība starptautiskajiem standartiem: Electrical cabinets conform to CE low-voltage and machinery directives. Risk assessment adheres to ISO 12100: 2010, while machine safety architectures comply with LV 415-10: 2014 (Safety of packaging machines).
Maza ID kabeļu ruļļu iepakošanas iekārtas izvēles kontrolsaraksts
Before confirming equipment sizing, audit the following coil and facility parameters:
- Minimālais spoles ID: Confirm the absolute smallest inner core diameter is ≥ 90 mm.
- Maximum Coil Envelope: Verify that maximum coil outer diameter is ≤ 400 mm and width/height is ≤ 180 mm.
- Svara ietilpība: Ensure coil weights fall within the 2–30 kg design threshold.
- Throughput Goal: Calculate required coils per hour against the machine’s 18–30 second cycle time (approx. 90–150 coils/hr at 80% operational efficiency).
- Iepakojuma materiāls: Select material type (LLDPE, PVC, or composite paper) and confirm roll core dimensions.
- Integration Mode: Determine whether the station operates as a stand-alone off-line packaging bench or integrates directly into an automated coiling and binding line.
Inženierijas bieži uzdotie jautājumi
Q: What is the smallest coil inner diameter the FPCA-100 can wrap? A: The physical lower threshold is 90 mm ID. The machine covers a broad working envelope from 90 mm up to 250 mm ID without replacing the primary ring structure.
Q: What is the true production throughput per hour? A: The wrapping cycle takes 18 to 30 seconds. In practical manual loading conditions, an operator typically finishes 90 to 120 coils per hour. When linked with an upstream automated coil delivery conveyor, throughput approaches 120 to 140 coils per hour.
Q: How does the machine prevent lightweight coils (2–5 kg) from jumping out during wrapping? A: A top-mounted, soft-PU-coated pneumatic press-down roller descends onto the coil top before the orbital ring accelerates, holding the coil firmly against the driven cradle rollers.
Q: Can one machine handle diverse wire gauges and batch sizes? A: Yes. As long as dimensional profiles sit within 90–250 mm ID and 150–400 mm OD, the operator simply calls up the corresponding pre-stored recipe on the HMI screen.
Q: What equipment options exist for coils exceeding 400 mm OD? A: Large coil profiles shift to higher-capacity models within the same horizontal design platform:
- FPCA-200: Coil OD 250–500 mm, weight capacity 2–50 kg.
- FPCA-300: Coil OD 400–900 mm, weight capacity 20–200 kg.
Nākamais solis
To integrate an optimized coil packaging system into your wire production floor:
- Submit Product Dimensions: Send coil minimum/maximum ID, OD, height, package weights, and target line output to info@fhopepack.com.
- Receive 48-Hour Engineering Proposal: Our mechanical design team will deliver a customized equipment layout, cycle-time simulation, and overlap schedule.
- Line Integration Planning: Schedule a technical teleconference or factory visit to coordinate conveyor transitions and coiler handshakes.
Saistītā lasāmviela
- FPCA-100 Horizontal Cable Coil Packing Machine
- FPCA-200 kabeļu spoļu iesaiņošanas mašīna
- FPCA-300 Heavy-Duty Cable Coil Wrapping Machine
- Video: Economic Cable Coil Packing & Wire Wrapping Machine
Avoti
- Equipment Specifications & Kinematic Data: Fhopepack FPCA-100 Product Specification Page
- Safety & Design Norms: ISO 12100:2010 Mašīnu drošība
- Packaging Machinery Safety Standards: EN 415-10:2014 General Requirements
Pēdējoreiz pārskatīts: 2026-10-03