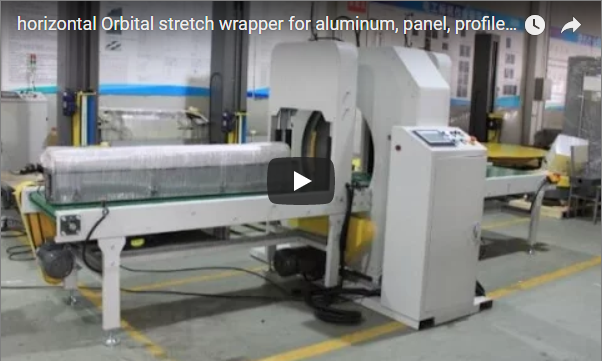
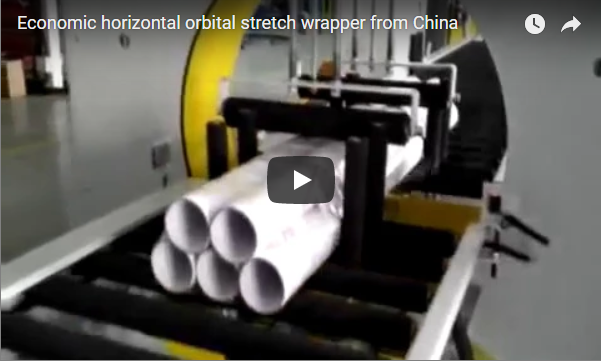
Santrauka Our horizontal ring orbital stretch wrappers secure industrial loads using pneumatic top press-down assemblies while the rotary ring applies stretch film in a continuous spiral. This positive clamping allows short goods from 800 mm in length to traverse the central conveyor ring gap smoothly without tipping, pivoting, or yawing under dynamic film tension. The compact E600 handles bundles and profiles within a 200–600 mm OD envelope, while the heavy-duty E1400 accommodates wide panels and bulk items up to 1,400 mm wide and 1,000 mm high. Selection between the two models depends strictly on package width and structural rigidity rather than payload weight alone.
Kodėl reikia laikyti krovinius
In an inline horizontal ring orbital wrapper, the payload advances from a powered infeed roller conveyor, traverses the rotating ring chamber, and transfers onto the outfeed conveyor. A physical mechanical gap between the infeed and outfeed beds is mandatory to allow the orbital ring and film carriage to revolve 360° continuously around and beneath the passing product.
When unsecured goods cross this cantilever transfer zone, dynamic film tension and conveyor discontinuity induce three distinct mechanical failure modes:
- Relative shifting: loose multi-piece bundles — extrusions, conduit, battens — take continuous tangential shear from the unwinding film. Without overhead constraint the inner layers slide and the pack falls apart.
- Conveyor slip: light or low-friction loads do not generate enough grip on powered steel rollers, so film tension drags them backwards and the overlap goes uneven.
- Lateral yaw and vibration: off-centre or top-heavy packs wander as they cross the ring throat.
By applying continuous downward force via overhead pneumatic press-down assemblies, the wrapper generates predictable normal friction on the driven roller bed, neutralizing dynamic unbalance and guaranteeing straight, stable throughput across the split-conveyor gap.
Kaip veikia prispaudimo įtaisai
| Parametras / funkcija | E600 | E1400 |
|---|---|---|
| Mechaninė struktūra | Dual overhead guided pneumatic vertical cylinders (infeed & outfeed) | Heavy-duty portal bridge press-down with auxiliary stability rollers |
| Kontaktinis paviršius | Non-marking vulcanized polyurethane (PU) rollers | Product-specific polyurethane, synthetic rubber, or engineering nylon |
| Lateral stabilization | Rankiniu būdu reguliuojami dvipusiai apsauginiai kreiptuvai | Integrated heavy-duty lateral side guides (manual or motorized) |
| Pneumatinis tiekimas | 5–8 kgf/cm² (regulated working pressure 0.2–0.6 MPa) | 5–8 kgf/cm² (regulated working pressure 0.2–0.6 MPa) |
| Judesio seka | Optical entrance/exit sensor tracking via integrated PLC | Multi-point photoelectric sensor array with automatic edge detection |
The vertical press-down assembly functions as an active mechanical clamp during the wrapping sequence:
- Anti-dispersion clamping: the infeed top cylinder brings non-marring polyurethane rollers down onto the pack before it enters the throat. Pressure is calibrated on site to the wall thickness and rigidity, so multi-piece packs compact without crushing.
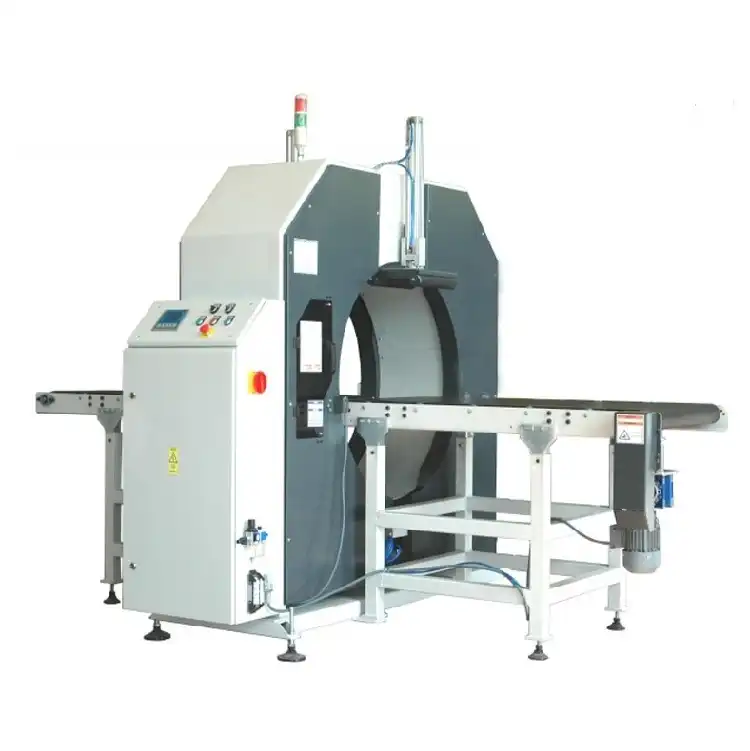
E600 or E1400: Platform boundary criteria
The primary selection boundary between the E600 and E1400 platforms is package cross-sectional width and structural rigidity, rather than total payload weight alone. A lightweight, wide panel cannot physically pass through the E600 ring, whereas a dense, heavy metal bar fits standard E600 geometry.
| Parametras | E600 Standard Platform | E1400 Heavy-Duty Platform | Engineering Boundary Focus |
|---|---|---|---|
| Load profile capacity | Bundle OD: 200–600 mm (or square equivalent) | Plotis: 300–1,400 mm; Aukštis: 50–1,000 mm | Width envelope defines ring diameter |
| Permissible load length | >800 mm (shorter profiles require custom bridges) | 1,000 – 3,000 mm | Minimum length dictated by conveyor gap |
| Rated payload weight | 20-200 kg | Derived from the bed and drive rating; confirmed per project | Heavy frames require reinforced drives |
| Konvejerio linijinis greitis | 3–12 m/min. (valdomas keitikliu) | Set by the VFD to match the ring speed | Matches upstream production line rates |
| Orbitinio žiedo greitis | Set by the VFD; working range confirmed per project | 10–60 aps./min | Governed by carriage rotational inertia |
| Connected drive power | Apie 4.5 kW | Approximately 4.5 kW (standard line configuration) | Main drive, conveyor, and hydraulic/pneumatics |
| Elektros komunalinis | 380 V, 3 fazis | 380 V, 3-phase (voltage and frequency confirmed at quotation) | Factory supply alignment |
| Conveyor dimensions | Infeed/outfeed beds: 2,000 × 800 mm each | Infeed/outfeed beds: 2,000 mm length each | Roller width sized to load stability |
| Film material compatibility | LLDPE film, paper roll, HDPE woven roll | LLDPE film, PE film, heavy paper, PVC wrap | Consumable tensile requirements |
| Plėvelės ritinėlio matmenys | Width: 150–300 mm; OD: 100–250 mm; ID: 50 mm | Width: 300 or 500 mm; OD: 200–300 mm; ID: 50 mm | Wide film required for high linear speeds |
| Persidengimo reguliavimas | 10–90% (programmable via HMI) | 10–90% (programmable via HMI) | Coordinated ring r/min and conveyor m/min |
Envelope sizing verification: The diagonal dimension of rectangular packages must never exceed the ring working envelope:
Diagonal = √(Width² + Height²)
- Pavyzdys 1: A bundle measuring 400 mm (W) × 300 mm (H) yields
√(400² + 300²) = 500 mm. Because 500 mm is safely within the 200–600 mm OD envelope, it is targeted for the E600. - Pavyzdys 2: A panel stack measuring 1,200 mm (W) × 200 mm (H) weighs only 60 kg (within E600 weight capacity), but its diagonal is
√(1,200² + 200²) = 1,216.5 mm. This product cannot fit the E600 and requires the E1400 platform due to its 1,400 mm width throat.
Time per load and throughput calculation
Cycle time is linear transit plus the dwell for ring spin-up, tail cut and edge reinforcement:
Total Time per Load ≈ (Load Length ÷ Conveyor Linear Speed) + (Reinforcement Wraps × Single Ring Rotation Time) + Mechanical Overhead
kur:
Conveyor Linear Speedis set by the VFD; the E600 documented range is 3–12 m/min.Single Ring Rotation Timeis60 ÷ Ring r/min(e.g., at 60 r/min, each turn requires 1.0 s; at 80 r/min, each turn requires 0.75 s).Mechanical Overheadcovers cylinder press stroke, film clamp release, and automatic cutting dwell (typically 3–6 seconds total).
Representative calculation for a 1,500 mm (1.5 m) bundle on an E600:
- Conveyor speed: 6 m/min (transit duration =
1.5 ÷ 6 = 0.25 min = 15 s). - Ring speed: 60 r/min (1.0 s per revolution).
- Reinforcement: 2 extra wraps on head, 2 extra wraps on tail (4 wraps total = 4.0 s).
- Mechanical overhead (clamp, cut, pneumatic response): 4.0 s.
- Estimated cycle time:
15 s + 4.0 s + 4.0 s = 23 s per load. That is the machine-only figure: 3,600 ÷ 23 ≈ 156 loads/h at continuous running, before loading, unloading and reel changes are added.
Partial wraps and delay-controlled reinforcement
Both wrapping platforms feature programmable logic controllers (PLC) that permit continuous spiral wrapping, selective multi-point banding, or reinforced head-and-tail wrapping.
- Head delay function: Delays the start of forward conveyor travel while the orbital ring rotates in place, applying multiple overlapping film layers to the leading 100–300 mm of the bundle.
- End delay function: Stops conveyor advance as the trailing edge approaches the ring, allowing the ring to apply supplementary retention wraps around the tail before the automatic cut-and-clamp unit triggers.
Kompromisas: head and end delays protect the edges that take the handling knocks, but the conveyor dwells while the ring turns, so every added edge wrap lengthens the cycle. Fix the reinforcement zones and layer counts at quotation against your cycle-time target.
Utilities and safety specifications
| Utility & Operational Parameter | E600 standartas | E1400 standartas |
|---|---|---|
| Connected power demand | Apie 4.5 kW | Apie 4.5 kW |
| Main voltage options | 380 V, 3 fazis | 380 V, 3-phase (voltage and frequency confirmed at quotation) |
| Pneumatinis tiekimas | 5–8 kgf/cm² (0.5–0.8 MPa) dry, filtered air | 5–8 kgf/cm² (0.5–0.8 MPa) dry, filtered air |
| Base footprint (L × W × H) | Apytiksliai 5,200 × 1,800 × 1,800 mm | Layout determined by conveyor bed lengths |
Safety system engineering:
- Perimetro apsauga: Sukurta taip, kad atitiktų ISO 12100: 2010 (Rizikos vertinimas ir mažinimas) ir EN 415-10: 2014 (Safety of Packaging Machines). Enclosed wire-mesh fencing and electro-sensitive interlocking safety switches cut power to rotary drives if access doors open.
- Pneumatic safety dump: Fast-acting dump valves exhaust cylinder line pressure upon Emergency Stop actuation (Category 0/1 per LT-60204 1), preventing unintended downward clamp movement during operator intervention.
- Soft start and stop: Variable frequency drives regulate ring acceleration and braking ramps to eliminate mechanical shock on the drive ring belt and internal ring bearings.
Selection checklist for orbital wrappers
Review these project parameters to finalize equipment sizing:
- 1. Load cross-section: Measure maximum product width and height to verify
√(W² + H²)clearance within ring opening boundaries. - 2. Minimum product length: Confirm if any standard load length falls below 800 mm (E600) or 1,000 mm (E1400) to determine if specialized bridge rollers are required.
- 3. Material rigidity and assembly: Determine whether payloads are rigid monolithic profiles or loose multi-piece bundles that require anti-dispersion top and side guiding.
- 4. Surface sensitivity: Specify whether soft polyurethane, neoprene, or silicone sleeves are required on press-down rollers to eliminate marking on painted, anodized, or polished surfaces.
- 5. Required film overlap: Establish target film overlap (10% to 90%) to calculate optimal conveyor linear speed and ring rotational speed pairings.
- 6. Film roll parameters: Match film carriage core dimensions (standard ID 50 mm) and roll outer diameter (100–250 mm or 200–300 mm) to stock material specs.
- 7. Factory utilities: Confirm local electrical supply (380V 50Hz, 380V 60Hz, or other 3-phase feeds) and dry pneumatic air supply between 5 and 8 kgf/cm².
Inžinerijos DUK
Q: Why is the E1400 required for a lightweight bundle measuring 1,100 mm wide and 100 mm high? A: Machine sizing is dictated by physical pass-through diagonal clearance rather than weight capacity. A 1,100 × 100 mm product yields a diagonal of approximately 1,105 mm. This exceeds the maximum 600 mm OD boundary of the E600 ring, necessitating the larger frame of the E1400 regardless of low payload weight.
Q: How does the press-down system prevent crushing fragile thin-walled profiles? A: Clamping cylinders are supplied via dedicated precision pneumatic pressure regulators. Operators adjust clamping pressure between 0.2 and 0.6 MPa (from an incoming line pressure of 5–8 kgf/cm²) to ensure sufficient holding friction without deflecting thin-walled aluminum or hollow plastic extrusions.
Q: Can the conveyor run continuously during head and tail reinforcement wrapping? A: Continuous movement during reinforcement would spread the film over a longer zone. For tight localized reinforcing bands, the PLC executes a temporary conveyor crawl or dwell while the ring completes the pre-set reinforcement revolutions, after which forward conveyor travel resumes at production speed.
Q: What is the primary difference in film carriage specifications between the E600 and E1400? A: The E600 carriage handles film roll widths of 150–300 mm with an outer roll diameter of 100–250 mm. The heavy-duty E1400 uses wider 300 mm or 500 mm rolls with outer diameters up to 300 mm, enabling faster surface coverage on wide structural loads.
Kitas žingsnis
To finalize your automated packaging layout:
- Provide profile specifications: Send your maximum/minimum load cross-sections, bundle weights, and target parts-per-hour to our engineering team at info@fhopepack.com.
- Receive 24–48 hour application review: Our engineering team will return a customized proposal complete with ring diameter verification, pneumatic clamping layout, and estimated cycle times.
- Line layout integration: Finalize infeed/outfeed conveyor heights, transfer logic, and perimeter safety layouts directly with our project integration team.
Šaltiniai
- Industrial wrapper specifications: E600 Product Page bei E1400 Product Page
- International safety compliance standards: ISO 12100: 2010 (Safety of Machinery – General Principles for Design) and EN 415-10: 2014 (Packaging Machines Safety – General Requirements)
- Operational reference demonstration: Horizontal orbital ring stretch wrapper video
Paskutinį kartą peržiūrėta: 2026-11-05