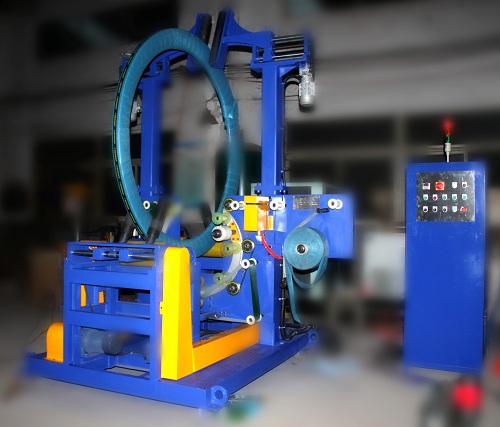
Effectus summary A two-stage line splits the job in two. Stage one wraps each coil through the eye on a ring wrapper; stage two moves the wrapped coils with an overhead gantry to build stacks. This clip of about one minute shows both stages on our lines. You see a blue ring wrapper with a gantry stacker, a white gantry with a yellow gripper head, and a second ring wrapping a narrow coil.
Table of Contents
- In brevi respondere
- Quod fragmentum ostendit
- Stage one: the ring wrapper
- Stage two: the overhead gantry
- What sets the line pace
- Coil range for conveyor-fed lines
- Index selectionis pro linea duarum phasium
- Moderationes et salus
- Quaestiones Frequentes de Ingeniaria
- tunc step
- Related reading
- sources
In brevi respondere
- A coil arrives flat on a powered roller conveyor.
- A ring wrapper passes film through the eye while rollers turn the coil, sealing it all round.
- The wrapped coil moves on to an overhead gantry.
- The gantry picks the coil and sets it down on a stack, or on the next station.
- The finished stack leaves the line on rollers or by forklift.
Quod fragmentum ostendit
| Tempus fragmenti | Scene |
|---|---|
| 0-12 s | A coil lies flat on yellow rollers in a blue vertical ring, which winds clear film through the eye |
| 12-40 s | A blue gantry over the conveyor lowers its gripper arms to a wrapped coil and sets it down |
| 45-55 s | A white gantry with a yellow gripper head travels over a roller platform with yellow fixtures |
| ultimae secundae | A narrow coil sits in another ring wrapper on green rollers while an operator in an orange hard hat works beside it |
Times come from frames taken about every 3 s, so each boundary is approximate. The clip is a montage, so the scenes come from more than one line.
Stage one: the ring wrapper
The ring carries the film roll and passes through the coil eye on every turn. Rollers under the coil turn it slowly, so each pass overlaps the last. When the coil has made one full turn, film covers the outer face, the bore and both sides.
On our coil packing lines, PLC/HMI programs set centring, tension and overlap per coil type. Film, paper or woven wrap can be used, and the same line can add PET or steel strapping and an ERP/MES label.
Stage two: the overhead gantry
Once the coil is wrapped, the line has to move it without damaging the new wrap. An overhead gantry does this from above, so no forklift or crane enters the line.
- The gripper arms close on the outer edge of the coil, as on the blue gantry in the clip.
- The carriage lifts the coil straight up, travels, and lowers it on the stack.
- The stack grows eye to sky, up to 6 coils per stack on our automatic coil packing line.
The white gantry later in the clip shows a different head: a yellow gripper unit that works over a roller platform. The head is designed to the coil range and the way coils are picked, so it changes from project to project.
What sets the line pace
A two-stage line runs at the pace of its slowest station. In most lines that is either the ring wrapper, which needs a full coil turn, or the gantry, which makes a lift and travel per coil.
| If the slowest station is | Correctio typica |
|---|---|
| anulus fascia | fewer wraps or lower overlap, where the shipment allows |
| gantry stacker | shorter travel, by placing stack positions close to the conveyor |
| outfeed | a buffer conveyor, so the stack can wait for the forklift |
This is why we ask for coils per hour on the first drawing: it decides the ring speed, gantry travel and buffer length together.
Coil range for conveyor-fed lines
Ex tabula nostra exemplarium involucri ferrei spiralis:
| model | Coil ID | Coil OD | Coil latitudo | Pondus maximum spirae |
|---|---|---|---|---|
| FPCA-1000 | 508 / mm 610 | 700 1600 mm, | 20 400 mm, | 2000 kg |
| FPCA-1200 | 508 610 mm, | 800 1400 mm, | 20 500 mm, | 2500 kg |
These are the conveyor-loaded models for automatic lines. The table is a starting point, not a full list; each line is built to the coil range of the project, so the figures can change.
Index selectionis pro linea duarum phasium
- Coils per hour, including peaks.
- Intervallum inter diametri interioris, exterioris, latitudinis et ponderis spirae.
- Wrap material, overlap and strapping.
- Stack height and stack pattern.
- Space for stack positions and buffer conveyors.
- Labels and data needed for your ERP/MES.
Moderationes et salus
Normae quae valent a foro destinationis pendent. Pro mercatibus CE, ISO 12100 modum aestimationis periculi statuit et EN 415-10 requisita generalia pro machinis involucris tractat, quae custodias et ordinationem sistendi in casu necessitatis statuit.
The ring and the gantry are both moving hazards above and around the coil. Guarding and stop circuits are fixed in the risk assessment for each layout.
Quaestiones Frequentes de Ingeniaria
Q: Why use two stages instead of one machine? A: Because wrapping and stacking can then run at the same time on different coils, and each machine stays simpler.
Q: How many coils go in a stack? A: Up to 6 coils per stack on our automatic coil packing line, depending on coil weight and handling.
Q: How does the gantry avoid damaging the fresh wrap? A: Its gripper arms close only on the outer edge and lift the coil straight up, so no forks or slings touch the wrapped faces.
Q: Which coil widths suit a conveyor-fed line? A: Our FPCA-1000 covers 20–400 mm and the FPCA-1200 covers 20–500 mm.
Q: Can the line label each coil? A: Yes. ERP/MES labelling is an option on our coil packing lines.
Q: What decides the line speed? A: The slowest station, usually the ring wrapper or the gantry. Your target coils per hour fixes the cycle time each station must meet.
tunc step
Lineam convasationis spirarum bipartitam tribus gradibus designamus:
- Delineationem tuam submitte with coils per hour, coil range and stack pattern, to info@fhopepack.com.
- Accipe propositionem intra horas quadraginta octo, with the wrapper, gantry and buffer layout.
- Inspectionem loci reserva so we confirm floor space, stack positions and forklift routes.
Related reading
- Linea Involuendi et Stratificandi Spirales Extensas Scissurae: Anulus Per Oculum ad Stratificatorem Porticum
- Linea Implendendarum Spirarum Cuprearum Duorum Graduum: Involutio Per Oculos, Deinde Stratificatio in Trabes Ligneas
- Linea Impacationis Foliorum Ferreorum a Coniunctione ad Congeriem: Quinque Mensurae Reditus Investitionis et Formula Reditus
- Linea automatica fasciculorum spiralium
sources
- Machina in actu: video in YouTube (about one minute)
- Up to 6 coils per stack, eye to sky, PLC/HMI centring, tension and overlap, wrap, strap and ERP/MES label options: Linea automatica fasciculorum spiralium
- Valores FPCA-1000 et FPCA-1200: Ferro coil involuti machina
- Ambitus normarum: ISO 12100:2010; LAT-415 10: 2014
- Tempus propositionis: admonitio ad agendum (CTA) ab domestico probata (propositio intra horas 48)
Ultima recensio: 2026-10-06