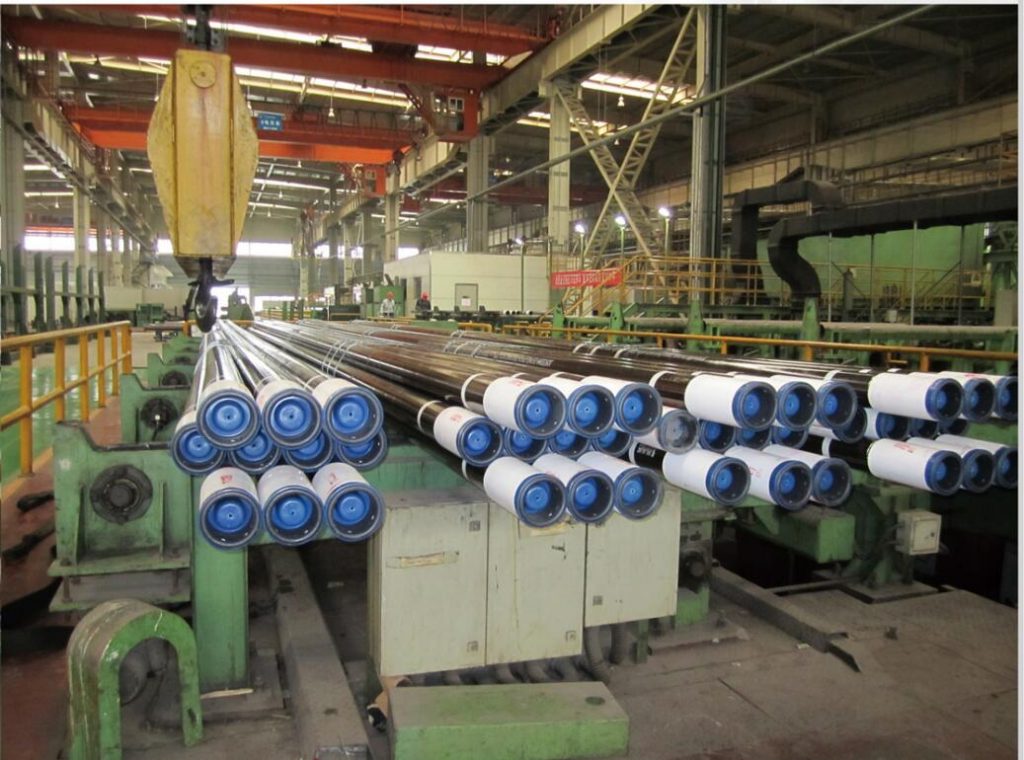
개요
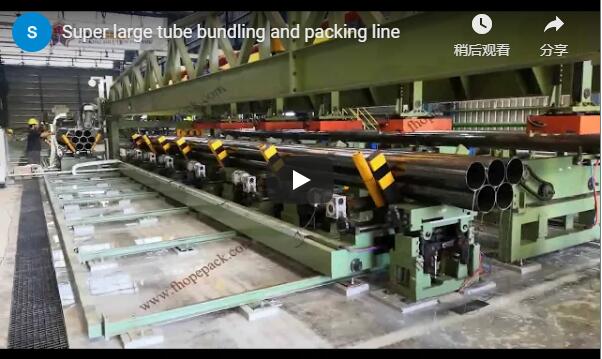
In high-speed ERW and precision tube mills, finishing throughput often outpaces manual bundling crews. Unsynchronized off-line packaging results in neck-down delays, irregular layer counts, and loose bundles that deform or lose tension during overhead crane handling. The automated steel tube bundle stacking and strapping line automates the entire downstream sequence: inline tube indexing, layer sorting, hexagonal or square bundle nesting, longitudinal anti-abrasion kraft paper wrapping, and automated high-tension strapping with PET or heavy-duty 25 mm / 32 mm steel strap. This technical guide outlines operational kinematics, bundle geometry formulas, strapping specifications, and mill integration criteria.
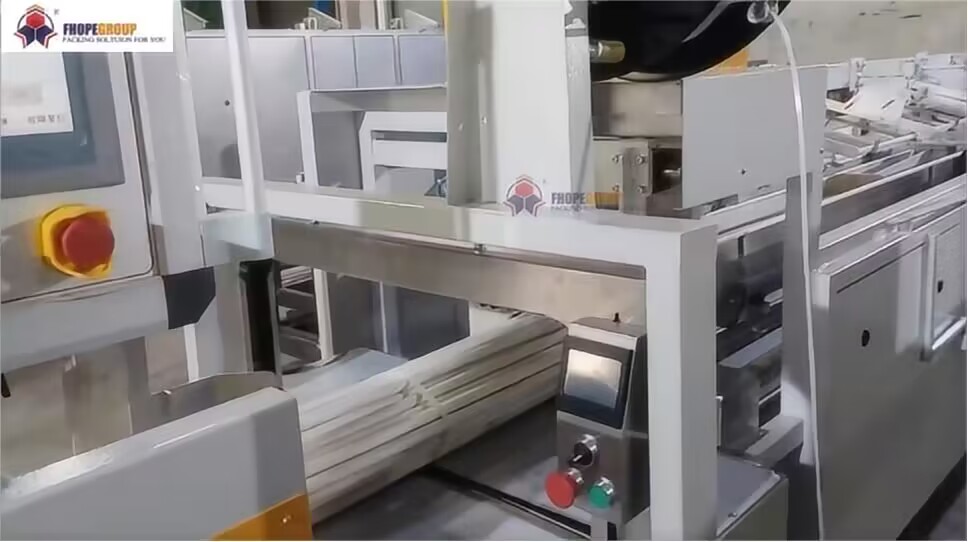
Configured specifically for bare, oiled, or powder-coated conduit and structural tubing, this automated packaging system integrates overhead pick-and-place gantries, pneumatic layer-forming guides, and synchronized side-containment cradles. By indexing individual pipes into predetermined packing arrays before applying tension-controlled strap bands, the line eliminates surface marring and guarantees structural integrity for intermodal transit and heavy crane hoisting.
차례
- 튜브 묶음 작업을 자동화해야 하는 이유는 무엇일까요?
- 라인 작동 방식
- 묶음 세기 수학
- 스트랩 데이터
- 선택 체크리스트
- 안전
- 엔지니어링 FAQ
- 다음 단계
- 관련 독서
- 지우면 좋을거같음 . SM
튜브 묶음 작업을 자동화해야 하는 이유는 무엇일까요?
Modern continuous tube mills run at linear discharge rates that quickly overwhelm manual stacking crews. Manual bundle building causes three primary production issues:
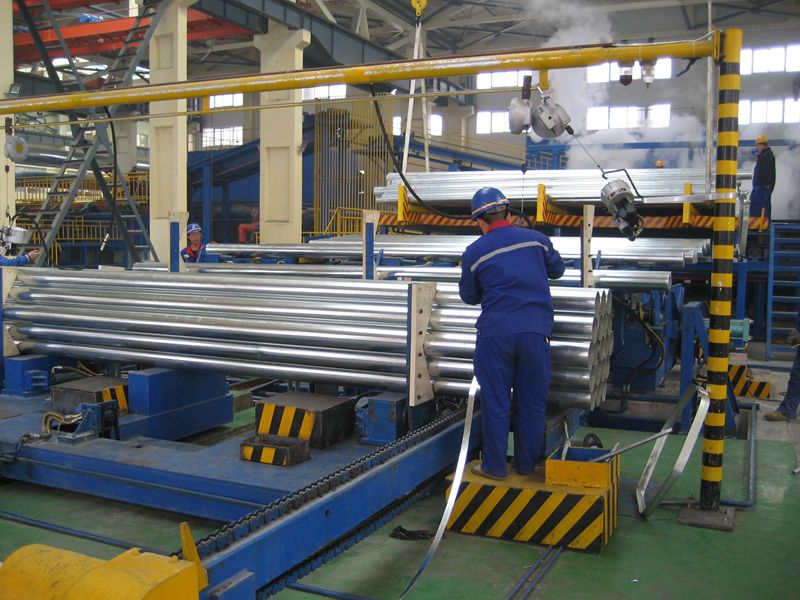
- Count Discrepancies and Inconsistent Geometry: Manual tallying frequently causes shipping errors. Misaligned tubes create uneven bundle faces and trapezoidal skewing that fails to nest securely inside standard flatbed trucks or open-top shipping containers.
- Dynamic Shifting During Crane Lifts: In loose, manually strapped bundles, individual tubes slip axially under crane sling hooks. This slippage concentrates shear stress on outer straps, leading to strap bursting, bundle collapse, and bent pipe ends.
- Coating Scratches and Rejection Rates: Painted, zinc-galvanized, or powder-coated tubes dragged across manual stacking beds suffer abrasive surface damage. Automated handling eliminates metal-to-metal impact by employing polymer-lined stops, driven polyurethane-coated rollers, and automated protective barrier wrapping.
라인 작동 방식
The automated bundling line links continuous cut-off saw discharge tables to downstream strapping heads through seven sequential engineering stages:
- Run-Out and Defect Rejection: Cut-to-length tubes enter the packaging station over motorized V-roller conveyors. Integrated optical sensors verify straightness and length tolerances; out-of-spec products automatically divert to a designated offline reject table.
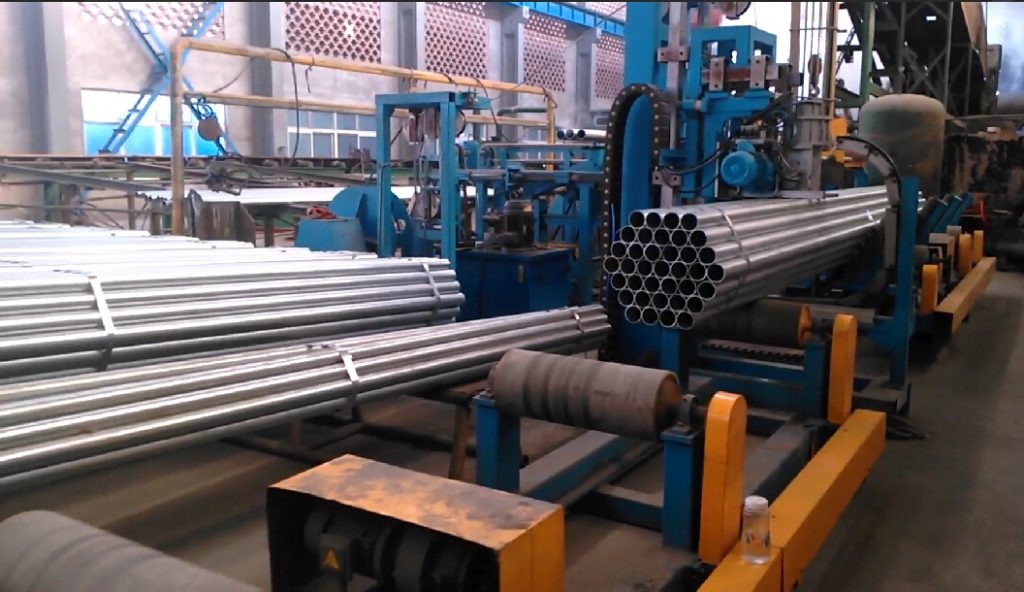
- Indexing, Singulation, and Counting: A mechanical walking beam or pneumatic lift-and-index arm separates individual tubes from the accumulation table. High-speed optical barrier sensors log each unit into the PLC counter to eliminate tally discrepancies.
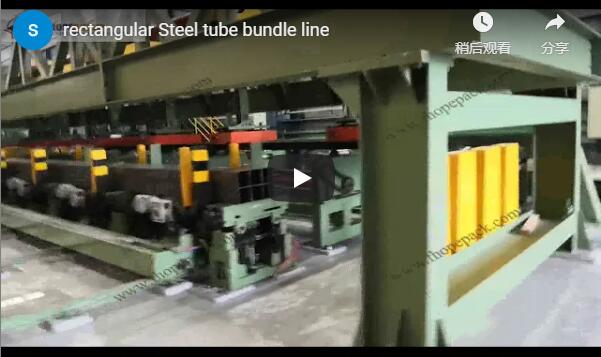
- End-Alignment and Orientation: An alignment roller bed drives all tubes against a rigid mechanical stop, matching bundle end-faces within ±5 mm. For rectangular or square hollow sections (HSS), a 90° axial turning mechanism reorients profiles into proper stacking layers.
- Layer Formation and Nesting: An overhead Cartesian transfer gantry equipped with electromagnets or pneumatic row-grippers lifts full rows into the forming cradle. Dual-hinged side containment arms progressively open as layers accumulate, guiding round tubes into an interlocking hexagonal close-packed grid.
- Protective Wrapping (Surface Defense): For coated, galvanized, or high-finish tubes, a roll-fed unwinder dispenses 120–180 GSM extensible kraft paper or multi-layer anti-corrosion barrier film lengthwise around the perimeter of the assembled bundle prior to banding.
- 원주형 스트래핑: The bundle indexes axially through an automated strapping machine. Depending on total package tonnage, high-tension polyester (PET) strapping (friction-welded) or 25 mm / 32 mm heavy-duty steel strapping (punch-notched or sealless locked) is tensioned at 5 to 7 programmed pitch intervals.
- Outfeed, Weighing, and Crane Staging: Completed bundles advance to the outfeed roller line where inline load cells capture gross weight, an automated applicator prints thermal tracking barcode labels, and padded cradle run-outs hold bundles for overhead gantry hoist removal.
묶음 세기 수학
Hexagonal bundle structures use close-packing geometry to maximize stacking density and minimize shifting during transit.
Hexagonal Bundle Formula
For a symmetric hexagonal cross-section with n tubes along each outer side, total tube count N follows the centered hexagonal number sequence:
N = 3n × (n - 1) + 1 (equivalently: N = 3n² - 3n + 1)
Square and Rectangular Bundle Formula
For square and rectangular hollow sections (HSS):
N = Tubes_per_row × Number_of_layers
Total Bundle Mass Calculation
Before finalizing strap sizing and crane rigging:
Bundle_Weight (kg) = N × Tube_Length (m) × Unit_Mass (kg/m)
Structural Envelope Estimation
The cross-sectional envelope determines strap feed chute clearance and warehouse rack fitting:
Bundle_Width (approx.) ≈ (2n - 1) × OD_tube
실제 공학 사례:
A hexagonal bundle containing 6 tubes per side (n = 6):
N = 3 × 6 × (6 - 1) + 1 = 91튜브.- At a 6.0 m cut length and a unit weight of 2.0 kg/m:
Total Bundle Weight = 91 × 6.0 m × 2.0 kg/m = 1,092 kg.
| Tubes per Side (n) | Tubes in Hexagonal Bundle (N) | Theoretical Bundle Width (× OD) | 일반적인 응용 프로그램 |
|---|---|---|---|
| 3 | 19 | 5 × 외경 | Small-batch conduit, hydraulic tubing |
| 4 | 37 | 7 × 외경 | 정밀 기계 튜브 |
| 5 | 61 | 9 × 외경 | Standard ERW structural pipe |
| 6 | 91 | 11 × 외경 | High-volume industrial distribution bundles |
| 7 | 127 | 13 × 외경 | Light-wall steel conduit / EMT conduit |
스트랩 데이터
Strapping specifications must resist dynamic surge forces during flatbed transport and single-point overhead sling lifting:
| 엔지니어링 매개변수 | Heavy Bare Tube Bundles | Coated / Conduit Bundles |
|---|---|---|
| 스트랩 소재 | High-tensile cold-rolled steel | Industrial-grade Polyester (PET) |
| 코일 와인딩 | Ribbon wound or oscillate wound | Jumbo mill-wound coreless/drum |
| 스트랩 너비 | 25.0mm 또는 32.0mm | 19.0mm에서 32.0mm |
| 스트랩 두께 | 0.80 mm to 1.00 mm (±0.04 mm) | 1.00 mm to 1.27 mm (±0.05 mm) |
| 폭 포용력 | ± 0.127 mm | ± 0.200 mm |
| Maximum Camber | < 8 mm per 2,000 mm length | Negligible / elastic recovery |
| Joint / Joint Sealing Method | Triple-notch sealless / seal-crimp | High-frequency friction weld joint |
| Joint Strength Efficiency | ≥ 80% of strap tensile rating | ≥ 85% of strap tensile rating |
| Applied Tension Range | 4,500 N to 8,500 N adjustable | 1,500 N to 4,500 N adjustable |
| Typical Bands per 6m Bundle | 5 to 7 bands | 5 to 6 bands |
Note: Critical line cycle times, conveyor bed widths, and radial cradle geometry are verified against factory mill layouts during the technical proposal phase.
선택 체크리스트
To configure an automated stacking and strapping line matching your mill output, verify the following mechanical criteria:
- Tube Profile & Dimensions: Outside diameter (OD) or cross-section dimensions (W × H for square/rectangular HSS), wall thickness range (WT), and steel grade.
- Length Envelopes: Minimum and maximum finished cut lengths (e.g., 4,000 mm to 12,000 mm).
- 번들 구성: Required bundle cross-sections (hexagonal, square, rectangular, flat master packs) and target piece count schedules per layer.
- Surface Finish & Protective Media: Bare carbon steel, pickling oiled, galvanized, or powder-coated/painted finish; requirement for longitudinal extensible kraft paper, corrugated board liners, or PE stretch film wraps.
- Mill Throughput Requirements: Mill speed in linear meters per minute (m/min) and cut-piece discharge rate (tubes per minute) at minimum tube length.
- Strapping Pitch & Fastening: Number of strap placements along bundle length, required minimum distance from bundle ends, and strap material preference (PET vs. high-tensile steel).
안전
FHOPE bundle handling, transfer, and strapping stations adhere strictly to European and International safety machinery directives:
- EN ISO 12100:2010: Risk assessment and risk reduction for industrial machinery integration.
- EN 415-10: Safety requirements for automated packaging machines, bundling systems, and associated conveying equipment.
- EN 60204-1: Electrical safety, grounding continuity, and functional arc-flash prevention for machinery industrial control panels.
- Hazard Containment: The stacking gantry and automatic strapping ring zone are enclosed within 2.0 m perimeter safety fencing with dual-channel category 4 interlocked access gates, safety light curtains at infeed/outfeed apertures, and distributed E-stop actuators complying with OSHA LOTO procedures.
엔지니어링 FAQ
Q: Can a single automated line process both round and rectangular profiles? A: Yes. The line uses swappable forming cradle inserts and an automated 90° profile rotator. The PLC recipe changes pneumatic stop pitches, switching seamlessly between hexagonal round-tube nesting and flat-layer square tube stacking.
Q: Why wrap kraft paper directly under the strapping path? A: Direct metal strap contact under 6,000 N tension can bite through powder coatings or mill varnishes during transit, creating localized paint failure and rust points. Extensible kraft paper absorbs friction, distributes edge-compression forces, and shields surfaces from shop airborne grime.
Q: Can tube piece counts be adjusted dynamically between mill production runs? A: Yes. Operators select pre-configured recipes on the industrial HMI touchscreen. The control system adjusts layer pick arrays, side-forming arm width, and strapping pitches without mechanical tool changes.
Q: How do we select between PET and high-tensile steel strapping? A: PET strapping offers superior retained elastic tension, making it ideal for bundles that settle or shrink slightly during warehouse transit, as well as coated pipes requiring non-abrasive banding. High-tensile steel strapping is required for heavy structural tube bundles exceeding 3,000 kg or hot-rolled pipes with sharp perimeter edges.
다음 단계
- 제분소 데이터 제출: Send pipe dimensional ranges, profile drawings, target bundle weights, and mill discharge rates to
info@fhopepack.com. - Review Layout Drawing: Our mechanical team delivers a customized line layout drawing within 48 hours, highlighting infeed transfers, strapping positions, and perimeter safety zones.
- 공식 견적서: Receive a comprehensive technical proposal including cycle-time simulations, utility consumption matrices, and commercial terms.
관련 독서
지우면 좋을거같음 . SM
- FHOPEPACK Engineering Technical Documentation: Automatic Packing Line for Steel Tube Bundles; Steel Tube Bundle Strapping Series.
- International Organization for Standardization: EN ISO 12100:2010 (Safety of Machinery — General Principles for Design).
- European Committee for Standardization: EN 415-10 (Safety of Packaging Machines — Part 10: General Requirements).
- International Electrotechnical Commission: EN 60204-1 (Safety of Machinery — Electrical Equipment of Machines).
최종 검토일: 2026년 10월 20일