תקציר מנהלים High-throughput cable packaging requires precision length monitoring, stable bundle integrity, and moisture-resistant barrier sealing in a continuous automated flow. Our turnkey production line synchronizes three core operations into a closed loop: a servo-driven coiler with dual pneumatic pinch rollers that winds wire onto an auto-collapsing mandrel, a heavy-duty radial strapping head that secures the inner loops under controlled tension, and a high-convection heat shrink tunnel that seals the coil in puncture-resistant polymer film. Key parameters—such as traverse pitch, winding turns, strap tension, and shrink film width—are dynamically governed by cable outer diameter (OD), target cut length, ו גיאומטריית סליל. Each packaging line is custom-engineered to integrate seamlessly with continuous extrusion or off-spool payoff operations.
תוכן העניינים
- Process Architecture: In-Line Operation Analysis
- How the Coiling, Strapping, and Shrink Line Works
- Turns and Layer Kinematics per Coil
- Shrink Film Sizing and Thermal Tunnel Dynamics
- System Controls, Interlocks, and CE Safety Standards
- רשימת בדיקה לבחירת הנדסה
- שאלות נפוצות בנושא הנדסה
- Next Step: Turnkey System Integration
- קריאה קשורה
- Sources and Operational Standards
Process Architecture: In-Line Operation Analysis
The automatic packaging line executes high-speed spool-to-coil conversion without requiring intermediate manual handling:
- Continuous Infeed and Meter Counting: Insulated cable enters from an active payoff or continuous extruder through a dual-wheel pneumatic capstan. An incremental optical rotary encoder monitors linear displacement with a cut-length precision of ± 0.2% prior to pneumatic guillotine cutting.
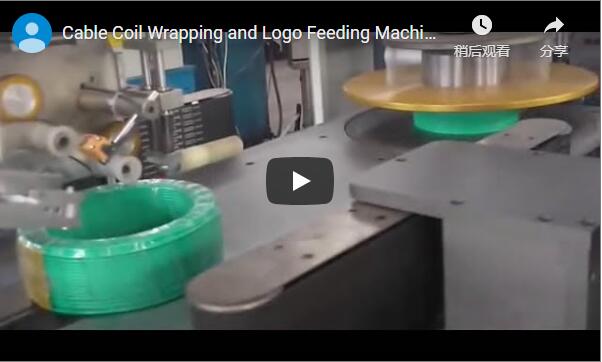
- Servo-Synchronized Traversing and Mandrel Winding: The green single-core conductor is guided into an auto-clamping slot on a 4-jaw collapsible mandrel. A ball-screw linear traverse actuator tracks rotation angle to lay tight, layer-by-layer wraps, eliminating wire crisscrossing and diameter bulge.
- Mandrel Collapse and Transfer: Upon reaching the target length, the mandrel collapses radially to relieve hoop stress, while a motorized transfer arm offloads the raw coil onto the strapping index table.
- Radial Index Strapping: The coil is indexed under an automated arch-track strapping head that applies polypropylene (PP) strapping through the eye-of-coil with adjustable tension (50–350 N) and thermal-weld joint bonding.
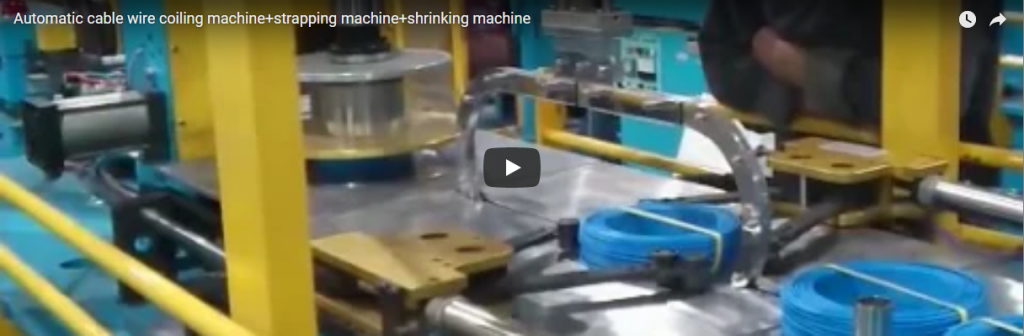
- Continuous Envelope Sealing and Shrink Tunneling: The stabilized coil travels via a low-friction roller conveyor through an automatic L-sealer film envelope station into a dual-zone hot-air recirculating shrink tunnel (160–210 °C), discharging a waterproof, tamper-evident bundle directly to the packing area.
How the Coiling, Strapping, and Shrink Line Works
| תַחֲנָה | מנגנון ליבה | פונקציה תפעולית | Critical Engineering Parameter |
|---|---|---|---|
| Pinch-Feed Coiler | Servo capstan + Collapsible 4-jaw mandrel | Meters length, clamps cable end, and winds coil under programmed tension | Linear speed: 50–300 m/min; Length accuracy: ± 0.2% |
| יחידת העברה | Pneumatic pusher + Transfer lifter | Collapses mandrel arms and transfers coil to strapping bed | Cycle time: 2.5–4.0 s; Stroke: 300–600 mm |
| יחידת רצועות | PP strapping head + Rotary table | Applies 2 or 4 radial PP straps through the core to secure the winding form | Strap tension: 50–350 N; Thermal weld efficiency: ≥ 85% |
| כווץ מעטפת | L-type thermal sealer + High-convection tunnel | Encloses coil in PE/POF film and shrinks it into a skin-tight protective package | Tunnel temperature: 160–210 °C; Airflow: Adjustable laminar |
| מסוע יציאה | Motorized stainless steel roller bed | Accumulates cooled, stabilized coils for automated robotic palletizing | Load capacity: 50 kg/m; Conveyor speed: 0.1–0.5 m/s |
Radial strapping prior to thermal shrink-wrapping is a mandatory physical sequence: it preserves mechanical coil integrity and internal winding stress during transfer, preventing loose coil expansion inside the shrink chamber. For operations requiring stretch-film wrapping rather than heat-shrink containment, consult our מכונת אריזת סליל כבלים כלכלית.
Turns and Layer Kinematics per Coil
While the machine’s PLC cuts cable based strictly on direct linear displacement (encoder counting), calculating turns per coil determines the required mandrel speed curve and traverse gearing.
The required winding turns are defined by total target length L, קוטר פנימי ID, outer diameter OD, and mean coil diameter D_mean:
D_mean = (ID + OD) / 2
Length per turn = π × D_mean
Total turns ≈ L / (π × D_mean)
Worked Calculation for a 100 m Finished Cable Coil
| פרמטר | ערך | Engineering Verification / Calculation Formula |
|---|---|---|
| Target Coil ID | 180 מ"מ | Mandrel collapsed diameter: 170 mm; expanded diameter: 180 mm |
| Target Coil OD | 260 מ"מ | Radial build-up: (OD - ID) / 2 = 40 mm |
Mean Diameter (D_mean) |
220 מ"מ | (180 mm + 260 mm) / 2 |
| Average Developed Length per Turn | 0.691 מ | π × 0.220 m |
| Total Required Turns | ~145 turns | 100 m / 0.691 m ≈ 144.7 turns |
| Radial Layers (for 4 mm cable OD) | שכבות 10 | 40 mm build-up / 4.0 mm cable OD |
| Turns per Traverse Layer | ~14–15 turns | Traverse stroke: 60 mm width |
Because instantaneous coil diameter expands progressively from 180 mm to 260 mm, the main spindle drive continuously reduces RPM via PLC vector control to maintain a constant line speed and avoid cable elongation.
Shrink Film Sizing and Thermal Tunnel Dynamics
The shrink film (Polyolefin POF or LDPE) must fully envelop the coil geometry, providing overlap for end-seal integrity and thermal contraction.
The required flat film width W_film for center-folded shrink film is governed by coil geometry and a safety clearance allowance:
W_film ≥ OD + Height + 2 × C_seal
איפה:
OD= Finished coil outer diameterHeight= Axial height of the coil packC_seal= Sealing margin and machine tracking allowance (typically 30–50 mm per side)
Sizing Specification for 260 mm OD × 100 mm Height Coil
| פרמטר גודל | ערך | Design Constraint / Rationale |
|---|---|---|
Coil Outer Diameter (OD) |
260 מ"מ | Measured finished build-up |
Coil Height (H) |
100 מ"מ | Traverse width setting |
Sealing Allowance (C_seal) |
30 מ"מ לכל צד | Accommodates L-bar sealing clamp radius and material tolerance |
| Minimum Center-Fold Film Width | 420 מ"מ | 260 mm + 100 mm + (2 × 30 mm) = 420 mm |
| עובי סרט מינימלי | 25–45 מיקרומטר | LDPE/POF puncture resistance against sharp cut cable ends |
| Tunnel Shrink Factor Allowance | 20% ל 35% | Free biaxial thermal contraction inside the heated chamber |
Selecting excessive film width causes plastic dog-ears and uneven material accumulation, while undersized film leads to blown-open seams. The packaging line’s heat tunnel uses bottom-directed and lateral air knives to guarantee uniform shrink tension across the core opening.
System Controls, Interlocks, and CE Safety Standards
Operating a multi-station line combining rotating winding mandrels, high-tension strapping swords, and heated thermal zones requires comprehensive risk reduction protocols:
- שמירה פיזית על ההיקף: The coiler, index conveyor, and strapping head are enclosed in yellow safety perimeter fencing (2,000 mm height) compliant with ISO 14120.
- Access Control & Safety Interlocks: Dual-channel safety gate interlocks (ISO 14119) and Type 4 optical safety light curtains instantly cut off hazardous motion upon perimeter breach via Category 4 / PL e safety relays.
- Thermal Hazard Isolation: The heat tunnel features double-layer rock-wool insulation (shell skin temperature remains below 45 °C) and an automatic conveyor purging cycle that evacuates remaining coils during emergency stops to prevent product combustion.
- LOTO Isolation Points: Centralized pneumatic dump valves and pad-lockable main electrical disconnects ensure compliance with OSHA 29 CFR 1910.147 for safe servicing of cutter blades and strapping heads.
- תאימות סטנדרטית: The line is built to comply with:
- ISO 12100: 2010: Safety of machinery — General principles for design and risk assessment.
- EN 415-10: 2014בטיחות מכונות אריזה - דרישות כלליות.
- EN-60204 1ציוד חשמלי של מכונות תעשייתיות.
רשימת בדיקה לבחירת הנדסה
Provide the following electrical, physical, and process data to finalize machine sizing:
- Conductor and Cable Specifications: Cable type (flexible BV/BVR, solid NYY, network cable), overall OD range (min/max mm), minimum permissible bend radius.
- Coil Packaging Dimensions: Target length per coil (e.g., 50 m, 100 m), inner core diameter (ID), maximum allowed outer diameter (OD), and coil package height.
- דרישות פלט: Required throughput in coils per minute (PPM) or units per hour (UPH).
- מפרט חסון: 2-point radial tie or 4-point cross-strapping; strap type (PP core 9 mm or 12 mm width).
- Film and Packaging Barrier: Polyolefin (POF) or Low-Density Polyethylene (LDPE), film gauge (microns), labeling/sticker application requirements.
- תשתית המתקנים: Plant footprint limits (L × W × H), primary power supply (e.g., 380V/480V 3-phase 50/60 Hz), dry compressed air supply (0.6–0.8 MPa, clean/dry).
שאלות נפוצות בנושא הנדסה
Q: Why is radial strapping required before the coil enters the shrink tunnel? A: Cable windings possess inherent mechanical spring-back memory. If unstrapped coils are exposed to shrink tunnel heating, the cable’s internal hoop stress will cause coils to flare and loosen before the polymer film achieves its full clamping strength. Radial PP straps hold the winding turns tightly compressed, enabling the film to shrink smoothly against a dimensionally stable surface.
Q: Does the system track cut-length via mandrel rotation turns or independent measurement? A: The system uses an independent precision dual-wheel measuring encoder riding directly on the cable jacket. Counting winding turns alone introduces cumulative length discrepancies caused by shifting layer diameters and varying radial compaction. The direct-contact encoder maintains length accuracy within ± 0.2%.
Q: How does the collapsible mandrel release the wound coil without damaging jacket insulation? A: The coiling head employs four radial segments actuated by an internal pneumatic/hydraulic toggle link. When winding is complete, the segments retract inward by 10–15 mm. This sudden reduction in circumference fully breaks the contact friction between the inner cable layer and the steel mandrel, allowing a mechanical pusher to slide the coil off cleanly without surface scratching.
Q: Can the line run without strapping for light-gauge building wires? A: Yes. The PLC features a recipe-driven station bypass mode. For light wire gauges where shrink film alone provides adequate retail bundle containment, the index table transfers coils directly into the L-sealer and shrink tunnel, bypassing the strapping head to increase line throughput.
Next Step: Turnkey System Integration
Integrate an automated coiling, strapping, and shrink-wrapping system into your line through our standardized three-stage project workflow:
- Line Integration and Layout Review: Submit your product spectrum, cable outer diameters, and plant layout drawings to info@fhopepack.com.
- הצעה טכנית (בתוך 48 שעות): Our packaging engineering team provides a full 3D layout, functional cycle time analysis, utility consumption matrix, and commercial proposal.
- מבחן קבלת מפעל (FAT): Ship sample cable reels to our testing facility for real-world validation of winding tension, strapping reliability, and film shrinkage prior to site delivery.
קריאה קשורה
- קו אריזה סליל אוטומטי
- Video: Automatic Steel Wire Coiler for Wire Winding and Strapping
- Video: Double Wall Corrugated Hose Coiling and Strapping Machine
- Video: Cable Coil Packing Machine for Small-ID Wire Coils
Sources and Operational Standards
- Technical Specifications: FHOPE Engineering Division, Cable Automation Line Group (Release 2026.03)
- הדגמת מכונה: Cable Packaging Systems on FHOPEpack
- Machine Safety Directives: ISO 12100:2010 — Risk Assessment
- מפרט טכני של מכונות אריזה: EN 415-10:2014 — Safety of Packaging Machines
- Electrical Safety: IEC 60204-1 (Safety of Machinery – Electrical Equipment of Machines)
נבדק לאחרונה: 04-10-2026