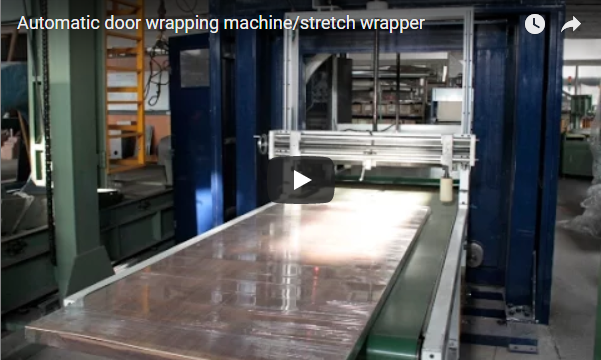
תקציר מנהלים Our aluminum profile wrapping line feeds timber spacer blocks to the top and bottom of each bundle, then spiral wraps the bundle with stretch film. The PLC sets the number of blocks from the bundle length. The line takes bundles from 70 to 300 mm high, 450 mm wide and 5,650 to 6,500 mm long, and one operator feeds the profiles.
תוכן העניינים
- איך הקו עובד
- Bundle size window
- Planning the spacer blocks
- Wrapping the bundle
- Ring speed, line speed and overlap
- שירותים ובטיחות
- רשימת בדיקה לבחירה
- שאלות נפוצות בנושא הנדסה
- שלב הבא
- קריאה קשורה
- מקורות
איך הקו עובד
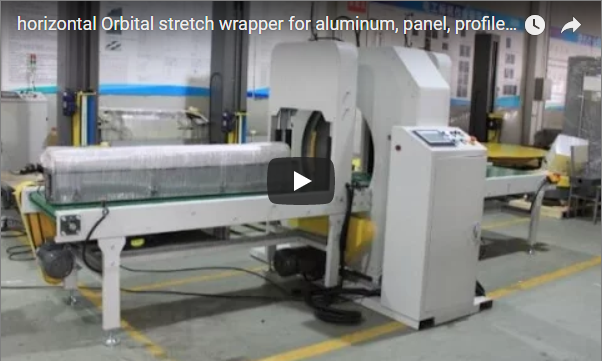
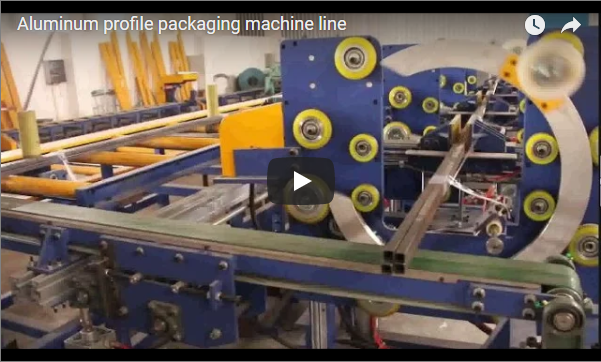
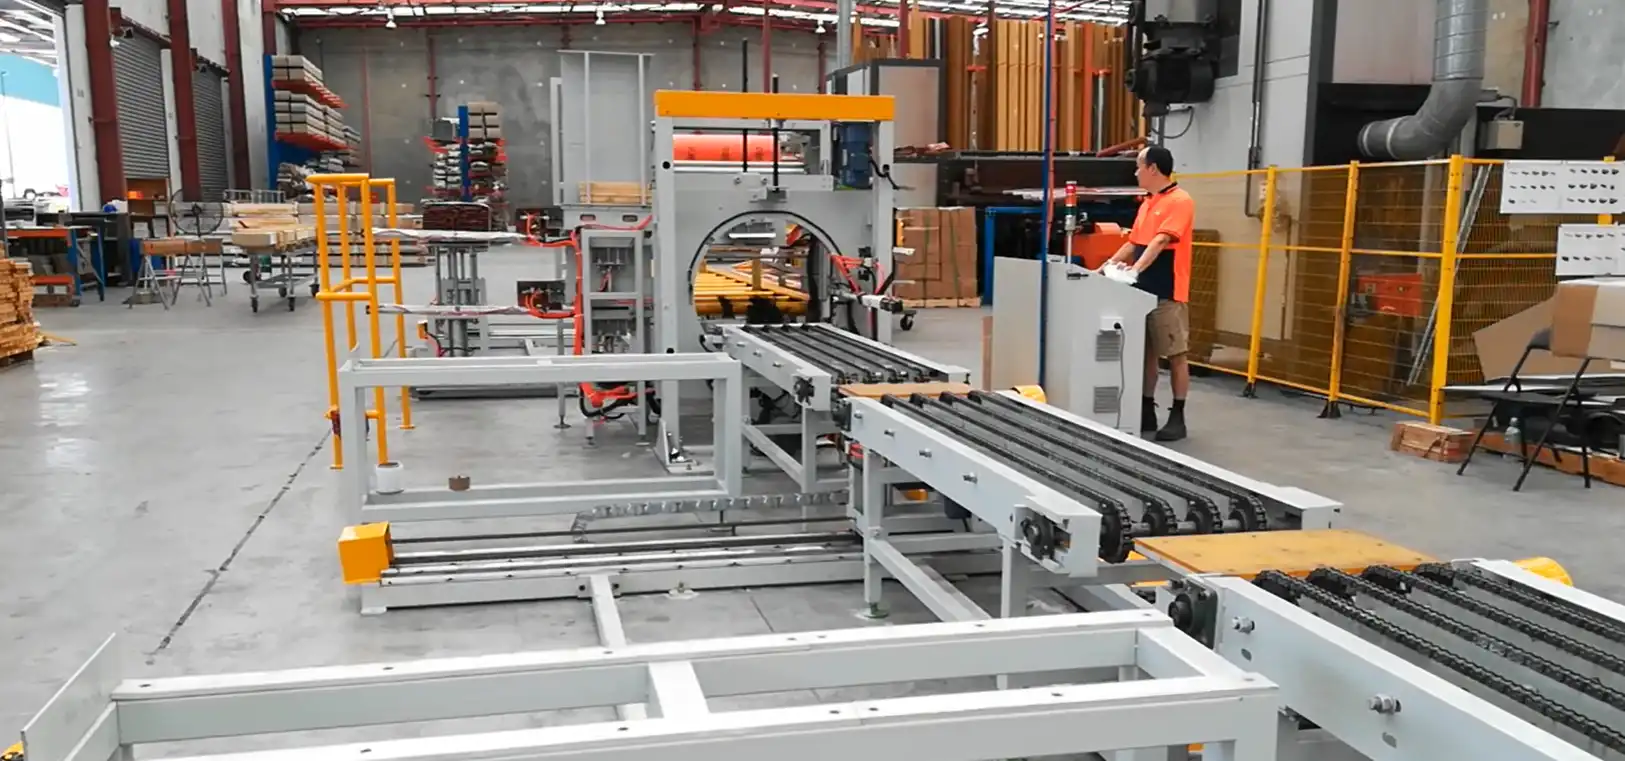
In this video, our line wraps flat aluminum profile bundles in blue stretch film. The bundles run on a conveyor through the ring of the horizontal wrapper. The line has three stations:
- Infeed roller table. Powered rollers carry the bundle. Centering rollers keep the profiles in the middle of the table before the wrapper.
- Spacer feeder. The feeder places timber blocks on the top and bottom of the bundle. Photocells detect the bundle, and the PLC controls each step.
- Spiral wrapper. The ring starts automatically and wraps the bundle and blocks together with stretch film.
Bundle size window
| פרמטר | טווח |
|---|---|
| גובה הצרור | 70–300 מ"מ |
| רוחב הצרור | 450 mm (specified width for this line) |
| אורך החבילה | 5,650–6,500 מ"מ |
We build three standard lengths: 5,650 mm, 6,000 mm and 6,500 mm. The top feeding height adjusts to the bundle height. The rollers in the wrapper open and close automatically, so bundles of different sizes pass through without stopping the machine.
Planning the spacer blocks
The blocks keep space between stacked bundles for forklift tines and slings, and protect the profiles. The PLC sets the number of blocks from the selected bundle length and the set block quantity. A simple way to plan:
- Choose the spacing. For example, an illustrative spacing of 1,500 mm.
- Count the positions. For a 6,000 mm bundle: 6,000 ÷ 1,500 + 1 = 5 positions along the length.
- Count the blocks. With blocks on the top and bottom, that is 5 × 2 = 10 blocks per bundle.
The blocks are stored at the side of the machine and fed automatically. An automatic device integrated with the wrapper applies blocks under the bundle during wrapping, at the final stage. The finished bundle is stable and compact.
Wrapping the bundle
- סרט צילום. The spiral wrapper uses 25 micron stretch film.
- חומרים. Our aluminum wrappers can also apply PE, knit belt or VCI paper.
- חֲפִיפָה. Adjustable from 10% to 90%, to save material or seal the pack.
- Speeds. Inverters change the wrapping and conveying speed. The ring runs at 30–60 r/min.
- גְזִירָה. The blade cuts the material at the end of each cycle.
- Fault stop. If the film tears, the machine stops and alarms.
Changing a film roll takes less than one minute.
Ring speed, line speed and overlap
The bundle moves through the ring while the ring turns. How far it moves in one turn sets the overlap. Our aluminum wrapper has a wrapping speed of 2–16 m/min and a ring speed of 30–60 r/min:
- Fastest setting. At 16 m/min and 60 r/min, the bundle moves 16,000 ÷ 60 = about 267 mm per turn.
- Slowest setting. At 2 m/min and 30 r/min, it moves 2,000 ÷ 30 = about 67 mm per turn.
Compare this advance with the width of your film on the bundle. If the advance is close to the film width, the overlap is low. For a high overlap, we run a slower line speed or a faster ring. We set both with you from your film, the overlap you need and your bundles per hour.
שירותים ובטיחות
| שירות | דרישה |
|---|---|
| כוח | AC 380 V, 50 Hz (or to your requirement), wrapper 4.8 kW |
| אוויר | 6–8 בר |
| מַפעִיל | 1 person, for bundle infeed |
| פקדים | PLC and HMI, auto and manual modes, errors on indicator and touch screen |
התקנים החלים תלויים בשוק היעד. עבור שווקי CE, ISO 12100 קובע את שיטת הערכת הסיכונים ו-EN 415-10 קובע דרישות כלליות למכונות אריזה.
Selection checklist for an aluminum spacer feeding line
- Bundle height, width and length range.
- Block size, spacing and top and bottom placement.
- Wrapping material: stretch film, PE, knit belt or VCI paper.
- Target overlap and bundles per hour.
- Link to the upstream stacker and the downstream strapping or storage.
- Power and compressed air at the line.
שאלות נפוצות בנושא הנדסה
Q: What bundle sizes does the line take? A: 70–300 mm high, 450 mm wide and 5,650–6,500 mm long.
Q: How many spacer blocks does a bundle get? A: The PLC sets it from the bundle length and the block quantity you choose. At an illustrative 1,500 mm spacing, a 6,000 mm bundle gets 10 blocks, top and bottom.
Q: Does the feeder place blocks under the bundle too? A: Yes. Blocks go on the top and bottom, and a device integrated with the wrapper applies blocks under the bundle during wrapping, at the final stage.
Q: How do line speed and ring speed affect the overlap? A: The bundle advance per ring turn sets it. At 16 m/min and 60 r/min, the advance is about 267 mm per turn. At 2 m/min and 30 r/min, it is about 67 mm, which gives a much higher overlap.
Q: How many operators are needed? A: One person, to feed the profile bundles.
שלב הבא
We plan your spacer feeding line in three steps:
- שלח את שרטוט הפריסה שלך with bundle sizes, block spacing and bundles per hour to info@fhopepack.com.
- קבלו הצעה תוך 48 שעות, with feeder, wrapper and roller tables.
- הזמן סקר באתר to fit the line to your extrusion plant.
קריאה קשורה
- קו אריזה בפרופיל אלומיניום עם הזנת עצים
- מכונת עטיפה בפרופיל אלומיניום
- עטיפת מתיחה אופקית אוטומטית
- עטיפה אופקית חצי אוטומטית
- התאם אישית את העטיפה האורביטלית
מקורות
- Bundle sizes, timber feeder, roller tables, film, air, operator: aluminum profile packing line with timber feeding page
- Wrapper materials, overlap, speeds, power, controls: דף מכונת עטיפת פרופילי אלומיניום
- קו בפעולה: our aluminum horizontal wrapping machine with spacer feeder video on YouTube
- היקף התקנים: ISO 12100: 2010, EN 415-10: 2014
נבדק לאחרונה: 03-10-2026