Sintesi
How a coil wrapping machine works for steel packing comes down to two motions. A ring carries the material through the coil eye and round the section, while carrier rollers turn the coil slowly on its own axis. The ratio between the two sets the overlap. On our FPW-300, steel coils of 600–1,200 mm OD and up to 1,000 kg roll in, are wrapped in paper or film, and roll out.
Sommario
- The two motions of a coil wrapping machine
- Main parts of our ring wrapper
- How one steel coil is wrapped
- The speed ratio that sets overlap
- Worked example: setting the rollers for 30% overlap
- FPW-300 data for steel coils
- Lista di controllo per la selezione
- Sicurezza: EN 415-10 e ISO 12100
- FAQ di ingegneria
- Passo successivo
- Lettura correlata
- fonti
The two motions of a coil wrapping machine
A steel coil has a hole through the middle, so the wrap has to go through it. The machine does this with a ring that passes through the eye. As the ring turns, the roll of paper or film mounted on it travels through the eye, round the outside and back, laying one band across the coil section.
At the same time the carrier rollers turn the coil slowly. Each band lands a little further round, and after one full turn of the coil the whole surface is covered.
Main parts of our ring wrapper
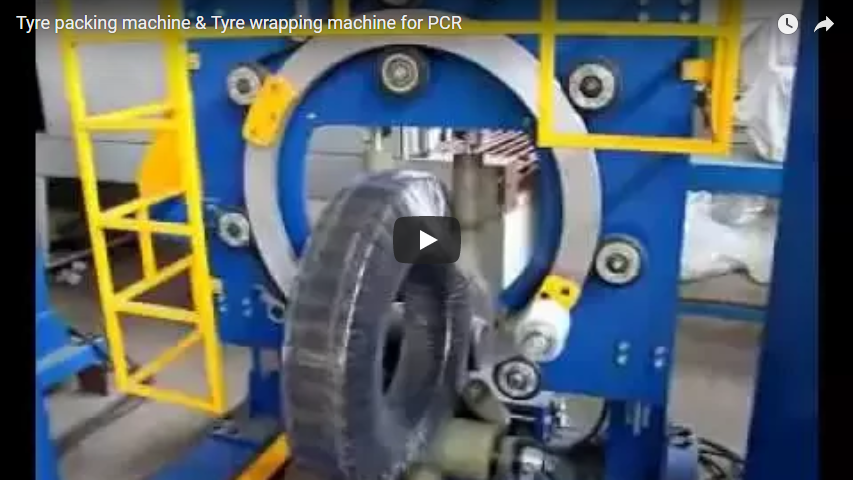
- Anello di confezionamento. Blue and vertical, with an opening segment so it can pass into the coil eye and close again before wrapping. It carries the material roll and its tension brake. The opening drive is confirmed per machine.
- Carrier rollers. Yellow-coated rollers in the blue base, driven to turn the coil.
- Guide arms. Yellow arms that steady the coil on the rollers.
- Guardia. Yellow mesh guard round the ring area.
- Armadio di controllo. Beside the machine, with buttons, indicator lights and the one-key automatic start.
How one steel coil is wrapped
- Roll in. The operator rolls the coil onto the carrier rollers, eye in line with the ring.
- Allacciare. The material end is fixed to the coil.
- Inizio. The operator returns to the cabinet and starts the automatic cycle.
- Avvolgere. The ring wraps while the rollers turn the coil through one full turn.
- Cut and roll out. The material is cut, the coil is tipped off the rollers and rolled away.
Rolling in and out suits lighter coils. Heavier coils are loaded by crane or by a powered conveyor.
The speed ratio that sets overlap
Let n be the ring speed in wraps per minute and N the number of wraps needed to cover the coil once. Then:
- The coil must make one turn while the ring makes N wraps.
- The carrier roller surface speed at the coil OD is v = a × n, where a is the advance per wrap at the OD.
- The wrapping time is t = N ÷ n.
So overlap is not set on the ring; it is set by how fast the rollers turn the coil against the ring. Our controls let both speeds, the material tension and the overlap be adjusted.
Worked example: setting the rollers for 30% overlap
Illustrative steel coil: ID 508 mm, OD 1,000 mm, width 250 mm, 100 mm paper, 30% overlap wanted at the OD.
| step | Calcolo | Risultato |
|---|---|---|
| Avanzamento per avvolgimento a OD | a = 100 × (1 − 0.3) | 70 mm |
| Avvolgimenti per bobina | N = π × 1,000 ÷ 70 | ≈ 45 |
| Advance at the ID | π × 508 ÷ 45 | ≈ 35 mm, so ≈ 65% overlap |
| Roller surface speed | v = 0.070 m × n | 0.07 × n (m/min, n in wraps/min) |
| Paper per coil | 45 × 2 × (246 + 250) millimetri | 44.6 m |
| Tempo di confezionamento | t = 45 ÷ n | (45 ÷ n) minutes |
Risultato. For 30% at the outside, the rollers must move the coil surface 70 mm for every ring wrap. Whatever ring speed is chosen, the roller speed follows it in that ratio, and the coil needs about 45 wraps and 45 m of paper. Doubling the ring speed halves the time only if the rollers double too.
FPW-300 data for steel coils
From our FPW-300 steel coil wrapping machine page: coil ID 508–610 mm, OD 600–1,200 mm, width 100–300 mm, weight 20–1,000 kg. Materials are PVC, LLDPE, PE, paper and HDPE on 50 mm cores, roll OD 100–450 mm and width 100–150 mm. Overlap is adjustable from 10% to 90%. Power is 1.5 kW at 380 V 50 Hz 3-phase, air 4–6 bar. The mainframe height adjusts to centre the ring on the coil, and the rollers carry a protective coating.
Lista di controllo per la selezione
- Diametro interno, diametro esterno, larghezza e peso della bobina.
- Loading: rolling, crane or conveyor.
- Material: paper, film or both.
- Overlap wanted at the OD.
- Bobine per turno.
- Voltaggio.
Sicurezza: EN 415-10 e ISO 12100
The wrapper is built to EN 415-10 and its risk assessment follows ISO 12100. The ring passing through the eye and the turning rollers are the hazards. The mesh guard closes the ring area, and the operator starts the cycle only from the cabinet, outside the guard. Tie-on and roll-off are done with the machine stopped, and the E-stop and error light are on the cabinet.
FAQ di ingegneria
Q: Why does the coil need to turn? A: The ring lays one band at a time across the section; the coil turning brings fresh surface under the ring until it is covered.
Q: What sets the overlap? A: The ratio of roller speed to ring speed. The ring speed sets the time, and the roller speed follows it.
Q: Can it wrap paper and film? A: Yes, PVC, LLDPE, PE, HDPE and paper are all used.
Q: Which standard applies? A: We work to EN 415-10 for this wrapper and document the ISO 12100 risk assessment in the CE file.
Passo successivo
- Send coil ID, OD, width and weight a info@fhopepack.com.
- Prepariamo the wrap count, material and loading method.
- Rispondiamo entro 24 ore con un layout e un preventivo.
Lettura correlata
- FPW-300 steel coil wrapping machine (product)
- Macchina avvolgitrice di carta e film in acciaio
- Steel coil and copper coil packaging machine for eye-through film wrapping
- How to load and unload a coil on a coil wrapping machine
fonti
- FHOPE FPW-300 steel coil wrapping machine product page
- Our ring wrapper shown above
- Worked example: formula and illustrative figures
- Norme: EN 415-10; ISO12100:2010
Ultimo aggiornamento: 18/10/2026