**Sintesi esecutiva**
>
> An automated steel wire rewinding and binding line takes a coil from the drawing area, rewinds the wire into a heavier, tidier coil and ties it with steel wire through the coil eye. Automated guided vehicles carry the coils between stations, so nobody lifts or pushes a coil by hand. Our equivalent solution pairs our steel wire winding machine (360 m/min, φ2–φ4 mm wire, 50–1,000 kg coils) with a wire-twist binding unit. Below we size the rewinding time, the binding wire per coil and the AGV layout.
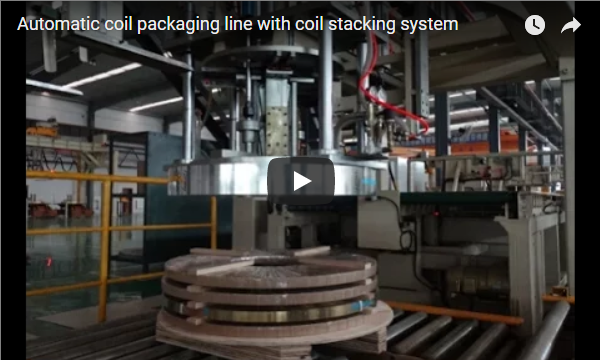
A low, round AGV carries a large silver coil of steel wire between the machines and stops under a grey gantry frame. Arms lower over the coil, and the wire runs out through a set of guides and rollers into the binding station, where it is shaped and cut. A control panel with a screen and a red emergency stop stands beside the frame, and the line starts only when the AGV is in position.
Sommario
- Why rewind and bind automatically
- Line flow, station by station
- Rewinding: speed and coil weight
- Rewinding time per coil
- Binding through the eye with steel wire
- Binding wire per coil
- AGV transport and docking
- Lista di controllo per la selezione
- Sicurezza
- FAQ di ingegneria
- Passo successivo
- Lettura correlata
- fonti
Why rewind and bind automatically
Wire from the drawing machine often comes off in small coils with many joints. Customers downstream want fewer, heavier coils, because every joint is a stop on their own line. Rewinding joins the wire into one larger coil, and binding holds its shape for lifting and shipping. Both steps are repetitive, heavy and close to moving wire, which is why they are the first to automate.
Line flow, station by station
1. **Supply:** the AGV brings the source coil to the pay-off position and docks under the frame.
2. **Rewinding:** the wire is pulled through guides and rollers and wound onto the reel, with the pay-off tension held steady so the wraps lie tight.
3. **Shifting:** the finished coil moves to the binding position.
4. **Binding:** wire is fed through the coil eye, wrapped round the coil section and twisted closed.
5. **Stacking:** a crane picks the bound coil and moves it to the storage area.
The PLC links the stations, so each step waits for the one before it to report done.
Rewinding: speed and coil weight
Our steel wire winding machine is an elephant-trunk type winder with the reel set eye to sky. The trunk connecting plate leads to a vertical doffing rack, which lets the coil build to a higher weight with fewer joints.
| Parametro | Valore |
| :--- | :--- |
| Winding reel diameter | φ560 mm |
| Winding speed | 360 m/min |
| Wire diameter | φ2–φ4 mm |
| Finished coil weight | 50–1,000 kg |
| Binding material | steel wire, PET or PP, by coil weight |
Heavier coils are bound with steel wire, lighter ones can use PET or PP strap.
Rewinding time per coil
Wire mass per metre = 7,850 kg/m³ × π × (d ÷ 2)², where 7,850 kg/m³ is the density of steel. Rewinding time = coil weight ÷ mass per metre ÷ winding speed.
| Wire | Mass per metre | Length in 1,000 kg | Time at 360 m/min |
| :--- | :--- | :--- | :--- |
| φ4 mm | ≈ 0.0987 kg/m | ≈ 10,100 m | ≈ 28 min |
| φ2 mm | ≈ 0.0247 kg/m | ≈ 40,500 m | ≈ 112 min |
Thin wire takes four times as long for the same coil weight. Binding takes the same time whatever the wire size, so on thin wire one binding unit can serve more winders than on thick wire.
Binding through the eye with steel wire
The binding unit has two main devices: wire feeding and wire twisting. The feeder pushes the binding wire through the coil eye and round the outside of the coil section. The twister then grips both ends and twists them closed.
There are two layouts for two ties per coil:
- **Two twisting devices:** both ties are made at once, for the shortest binding cycle.
- **One twisting device and a rotating table:** one tie is made, the table turns the coil, and the second tie is made. It costs less and suits a slower winder.
Steel wire as binding material saves strap cost, since the same wire family is already on site.
Binding wire per coil
Loop length = 2 × (radial width + coil height) + twist allowance, where radial width = (coil OD − coil ID) ÷ 2. The coil ID follows the φ560 mm reel. Take a coil 900 mm OD and 400 mm high, with a 100 mm twist allowance (example):
| Verifica | Calcolo | Risultato |
| :--- | :--- | :--- |
| Radial width | (900 − 560) ÷ 2 | 170 mm |
| Loop length | 2 × (170 + 400) + 100 | 1,240 mm |
| Two ties per coil | 2 × 1,240 | 2,480 mm |
Send your coil sizes, and the tie count, twist length and binding cycle time are confirmed at quote. The AGV payload and docking tolerance are confirmed at quote too.
AGV transport and docking
AGVs replace the forklift or crane run between drawing, rewinding and binding. Each AGV carries one coil on a flat round platform and follows a set path through the shop. Docking accuracy matters most: the AGV must stop under the frame so the pay-off arms meet the coil without striking it.
The station interlock waits for the AGV's in-position signal before the arms move. The number of AGVs depends on the travel distance and the rewinding time per coil, and is confirmed at quote.
Lista di controllo per la selezione
1. Wire diameter range and steel grade.
2. Source coil weight and size.
3. Finished coil weight, OD and height.
4. Binding material and number of ties per coil.
5. Coils per shift.
6. Shop layout, travel distances and the AGV paths.
Sicurezza
The line is designed to EN ISO 12100:2010 for risk assessment, EN 415-10 for general packaging machine safety, EN 60204-1 for the electrical equipment and ISO 3691-4 for the driverless AGVs. The running wire, the rotating reel and the twisting head are the main hazards. The gantry frame guards the moving parts, the control panel carries an emergency stop, and the AGV paths are marked and fitted with obstacle sensors. Fencing and CE documents are agreed per project.
FAQ di ingegneria
Q: What wire sizes does the winder take?
A: φ2–φ4 mm wire, rewound at up to 360 m/min.
Q: How heavy can the finished coil be?
A: 50–1,000 kg, set by the reel and the doffing rack.
Q: Steel wire or PET strap for binding?
A: Steel wire for heavier coils, PET or PP for lighter coils.
Q: Can one binding unit serve several winders?
A: Yes. Even on φ4 mm wire a 1,000 kg coil takes about 28 min to rewind, far longer than a binding cycle, so one binding unit and AGV transport can serve several winders.
Q: Do I need AGVs?
A: No. A crane or roller conveyor can link the stations; AGVs suit shops with long or changing travel paths.
Passo successivo
1. **Send your wire sizes, coil weights and coils per shift** to info@fhopepack.com.
2. **We size** the winders, the binding layout and the transport.
3. **Rispondiamo entro 24 ore** con una proposta e un preventivo.
Lettura correlata
- [High-speed steel wire rewinding packing machine](https://www.fhopepack.com/videos/high-speed-steel-wire-rewinding-packing-machine/)
- [Automatic wire coil rewinding and tying machine](https://www.fhopepack.com/videos/automatic-wire-coil-rewinding-and-tying-machine-video/)
- [How to do steel wire compacting and strapping automatically](https://www.fhopepack.com/videos/how-to-do-steel-wire-compacting-and-strapping-automatically/)
- [Steel wire coil rewinding and automatic packing](https://www.fhopepack.com/videos/how-to-do-steel-wire-coil-rewinding-and-automatic-packing-by-fhopepack-machine/)
- [Automatic steel wire coil winding and strapping machine](https://www.fhopepack.com/videos/automatic-steel-wire-coil-winding-and-strapping-machine/)
- [Wire rod compactor (product)](https://www.fhopepack.com/Steel-wire-strapping-machine/wire-rod-compactor.html)
fonti
- FHOPE product page: automatic steel wire winding and binding machine
-ENISO 12100:2010; EN 415-10; EN 60204-1; ISO 3691-4
- The rewinding and binding line shown above
Ultimo aggiornamento: 19/10/2026