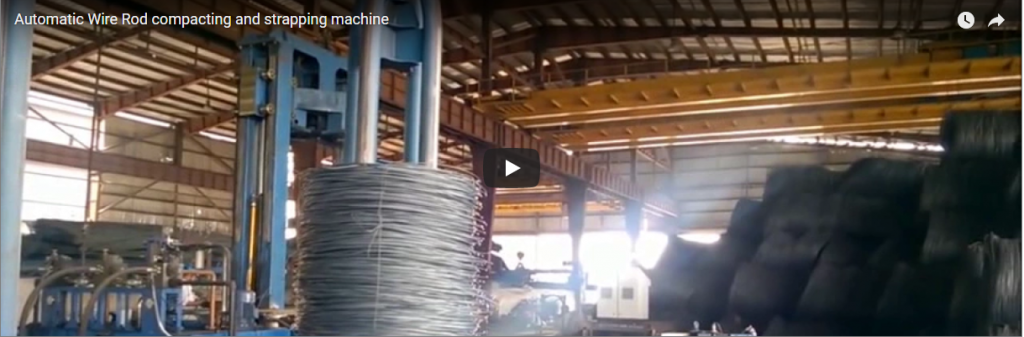
कार्यकारी सारांश This clip shows our wire coil strapping lines in a large wire plant. Many lines run side by side; on each, wire coils travel along yellow roller conveyors through strapping stations that band them, then move on to the line end. With many drawing machines, each strapping line serves a group of them.
विषय - सूची
- क्लिप में क्या दिखाया गया है
- Why many short lines
- How many lines
- हम प्रति पौधे के हिसाब से क्या निर्धारित करते हैं
- चयन चेकलिस्ट
- सुरक्षा
- इंजीनियरिंग से संबंधित अक्सर पूछे जाने वाले प्रश्न
- अगला कदम
- संबंधित पढ़ने
- सूत्रों का कहना है
क्लिप में क्या दिखाया गया है
| स्टेप | आपने क्या देखा |
|---|---|
| हॉल | Many coil lines side by side in a large wire plant |
| संदेश | Coils travel on yellow roller conveyors |
| चाबुक की मार | Strapping stations band each coil |
| ऑपरेटरों | Staff move between lines |
| बाहर का खाना | Strapped coils reach the line end |
Why many short lines
- Short routes. Each line sits near its drawing machines.
- No single choke point. One line stopping does not stop the plant.
- Shared design. All lines share spare parts.
- Step-by-step growth. Add lines as you add drawing machines.
How many lines
उदाहरण सहित (उदाहरण के तौर पर)।
| मद | वैल्यू |
|---|---|
| Plant output (illustrative) | 600 कॉइल प्रति घंटा |
| One strapping line (illustrative) | 80 कॉइल प्रति घंटा |
| Lines needed, 600 ÷ 80 | 7.5, so 8 lines |
| Coils per line at 8 lines, 600 ÷ 8 | 75 कॉइल प्रति घंटा |
| कुंडल का वजन (उदाहरण के लिए) | 1,000 किलो |
| Tonnes per line, 75 × 1,000 kg | 75 t per hour |
हम प्रति पौधे के हिसाब से क्या निर्धारित करते हैं
| की स्थापना | निर्भर करता है |
|---|---|
| प्रति कॉइल पट्टियाँ | Coil weight and transport |
| पट्टा | पीईटी या स्टील |
| कन्वेयर | Coil size and layout |
| पंक्ति गिनती | Plant output |
चयन चेकलिस्ट
- कॉइल का बाहरी व्यास (OD), आंतरिक व्यास (ID), ऊंचाई और वजन।
- प्रति कॉइल स्ट्रैप्स।
- Plant output.
- Drawing machines per line.
- Floor layout.
- पीईटी या स्टील का पट्टा।
सुरक्षा
- Keep clear of strapping heads while they move.
- Stay off roller conveyors.
- स्ट्रैप जाम को हटाने से पहले लॉक आउट करें।
- CE बाजारों के लिए, मशीन को ISO 12100 और EN 415-10 के अनुसार डिजाइन किया गया है।
इंजीनियरिंग से संबंधित अक्सर पूछे जाने वाले प्रश्न
Q: Why many lines instead of one? A: Short routes, no single choke point, and lines grow with the plant.
Q: How many lines does a plant need? A: Plant output divided by line rate; 8 lines in the worked example.
Q: What strap is used? A: PET or steel, chosen by coil weight and transport.
Q: Can lines be added later? A: Yes, as drawing machines are added.
Q: Do lines share parts? A: Yes, all lines use the same design and spares.
प्रश्न: कौन से मानक लागू होते हैं? उत्तर: सीई बाजारों के लिए, आईएसओ 12100 और ईएन 415-10।
अगला कदम
We match wire coil strapping lines in three steps:
- अपना लेआउट ड्राइंग जमा करें with coil sizes, plant output and layout, to info@fhopepack.com.
- 48 घंटों के भीतर प्रस्ताव प्राप्त करें मशीन के डेटा और लेआउट के साथ।
- साइट सर्वे बुक करें so we confirm the plant layout.
संबंधित पढ़ने
- स्टील वायर कॉइल रैपिंग, अपेंडिंग और स्टैकिंग लाइन
- Rebar and Rod Bundle Wire Tying Machine
- छोटे कॉइल्स के लिए फुल रैपिंग-थ्रू मशीन
- कुंडल पैकिंग मशीन
सूत्रों का कहना है
- मशीन सामग्री: एफएचओपीई इंजीनियरिंग टीम, 2026-10-10
- क्लिप: यूट्यूब पर वीडियो
- Line count: our worked example, illustrative values
- मानक का दायरा: आईएसओ 12100:2010; एन एक्सएनयूएमएक्स-एक्सएनयूएमएक्स: एक्सएनयूएमएक्स
- प्रस्ताव जमा करने की समय सीमा: स्वीकृत सदन सीटीए (प्रस्ताव 48 घंटों के भीतर)
अंतिम समीक्षा तिथि: 2026-10-10