Résumé: This review covers the manufacturer clip behind “Eliminating Edge Damage and Telescoping Defects: An Engineering Deep-Dive into Tilting Mechanisms for Slit Coils”. The footage shows a slit coil packing line: a vertical coil-handling station, an active film-wrapping run, and coils secured with bands. It shows no tilt cycle, no edge-damage test and no telescoping check. The answer to the title’s promise is a document, not more footage.
https://www.fhopepack.com/Automatic-Coil-Packing-Line/
Who this is for: plant engineers, maintenance leads and packaging buyers who run slit coil or similar coils and are weighing an automatic tilting and coil-handling setup against manual work. It separates what this clip puts on screen from what only the supplier’s engineering documents can settle.
How this review was made: The clip runs about 73 seconds (1 minute 13 seconds). Thirty-seven stills were sampled every two seconds, plus four frames that were re-checked a second time. Each still was read on its own by a local vision model at temperature zero, then cross-checked by hand, one still at a time. Still frames show what was on screen at that instant; they cannot establish motion, sequence or timing.
Dans cette critique : Ce que montre la vidéo · Notes d'observation directe · Ce que la vidéo ne montre pas · Claims vs footage · étape par étape · Why tilting matters · Liste de contrôle de vérification · QFP · Lecture connexe · Suivant
Ce que montre la vidéo
This clip is a roughly 73-second walk through one coil packing line. Three things appear clearly enough to state:
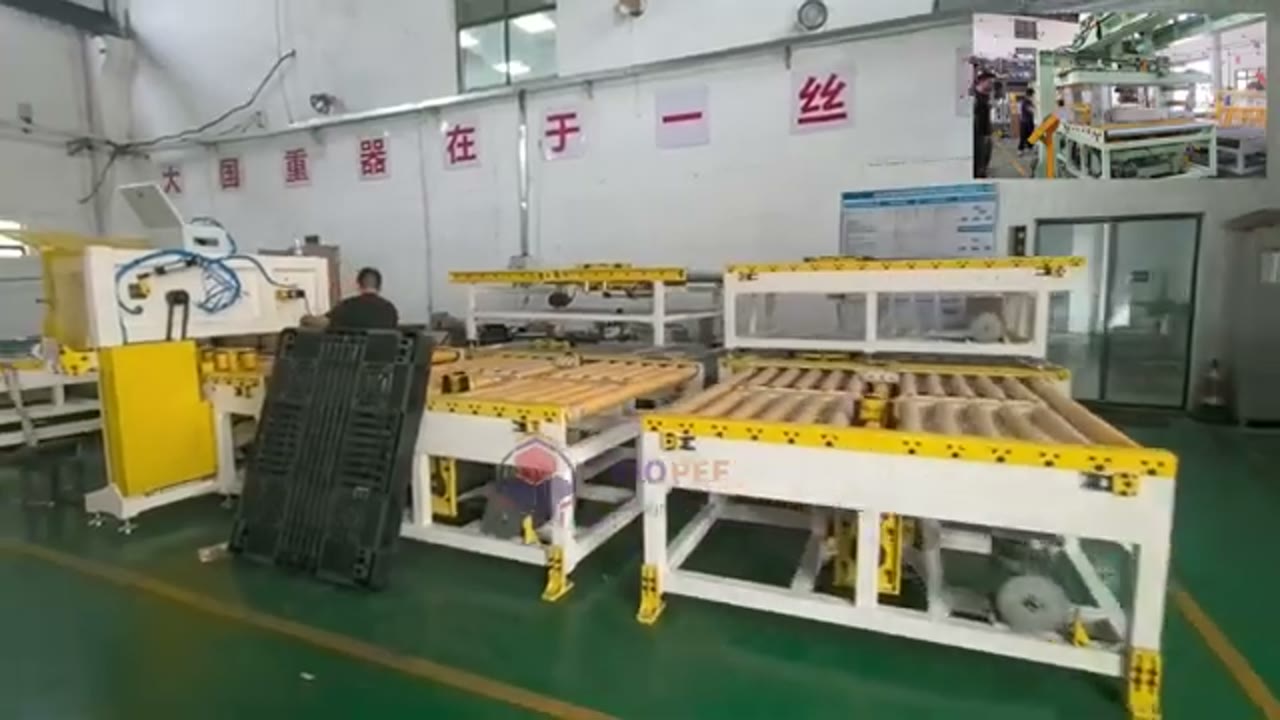
- The line handles coils in two orientations, vertical and horizontal, with powered roller conveyors linking the stations.
- Film wrapping is running during the clip: clear film is dispensed around a coil body and wrapped coils recur in later frames.
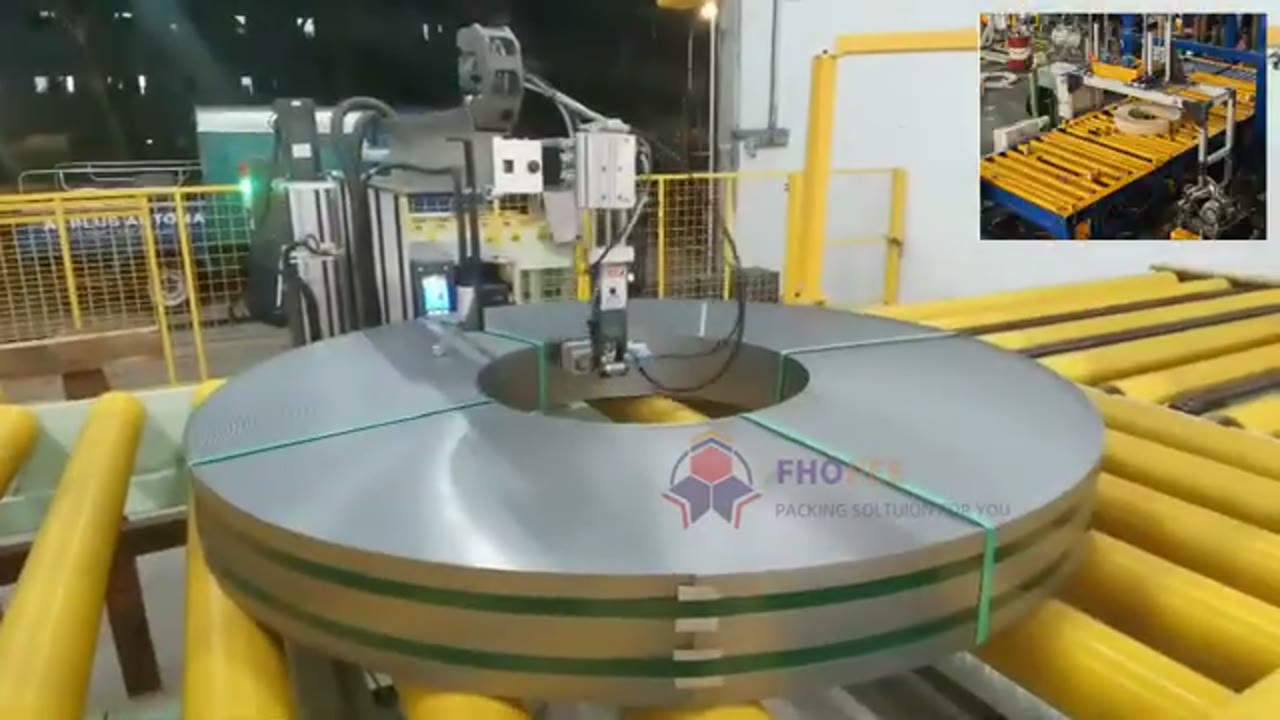
- Strapping bands sit on the coil bodies at the end of the clip, and the band reads as rigid metal rather than soft film.
What the clip never puts on screen is a number. There is no tilt-angle readout, no edge test, no telescoping check and no measured cycle. So this review answers the question the footage can answer, which is what the machinery looks like, and leaves the engineering claim where it belongs: in writing.
Notes d'observation directe
So that nothing is filled in by assumption:
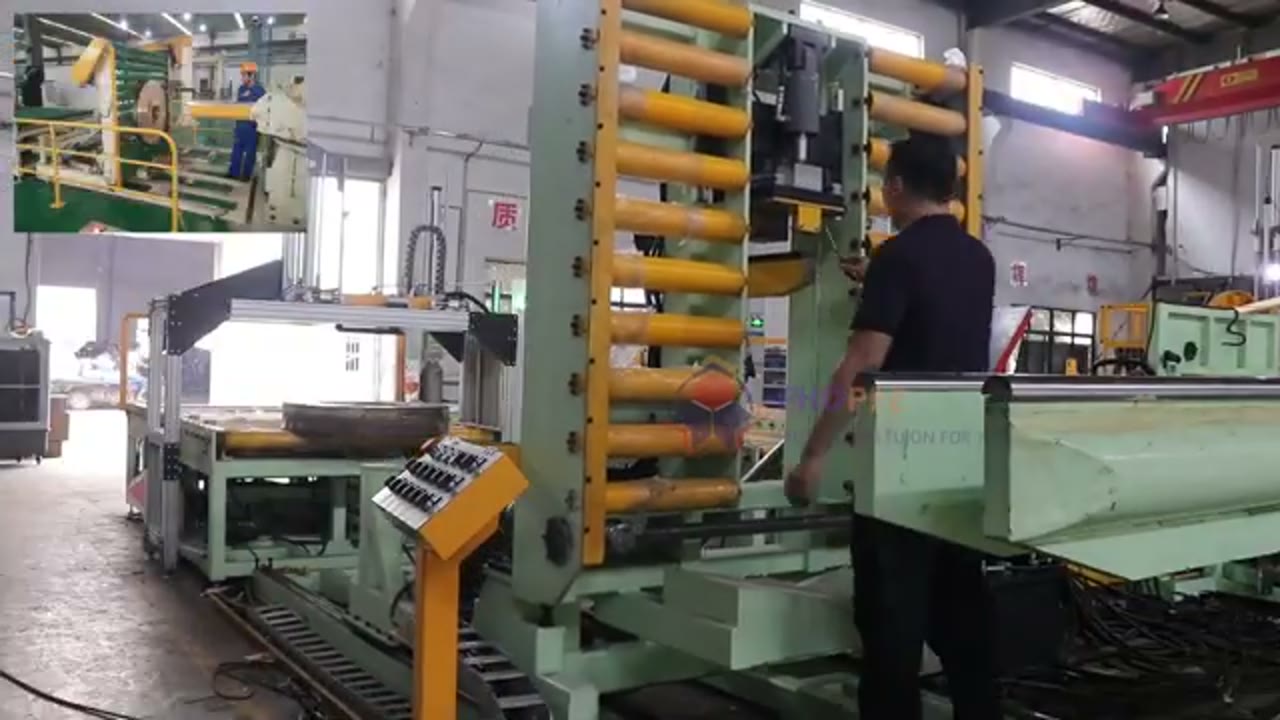
- Material and orientation. Coils read as steel coil in both orientations. The vertical handling section shows the station, its V-shaped rollers and panels, and an inset view of a coil in a vertical orientation with an operator at the machine.
- Film wrapping, active. Film is dispensed from the wrapping station mid-clip, and coils with a wrapped film finish come back in several later frames.
- Strapping band, at the end. Thin reflective bands sit on coil bodies near the end of the clip, and the band reads as a rigid metal strap rather than soft film. Strapping tension is never stated.
- Horizontal handling. Most later frames show a horizontal coil on a powered roller conveyor, under overhead arms and rotating platforms.
- No instrumentation anywhere. Across all sampled frames, no tilt-angle readout, no edge-damage test, no telescoping check and no load, speed or output figure appears. Panel faces are too small or too far away to read.
- Lettering is factory décor. On-screen lettering is mangled FHOPE-family signage and wall text, not a machine identification. No clean nameplate, model or capacity plate is readable in any frame.
- Stacking does not appear. Every sampled coil sits on rollers or a platform on its own. A finished-coil stack read in one inset was overruled on re-check, which found a single coil.
Ce que la vidéo ne montre pas
For a purchase decision this size, the gaps decide the case:
- Any tilt angle, tilt mechanism design, pivot arrangement or coil-support method.
- Any edge-damage test result, damaged-edge limit or tolerance figure.
- Any telescoping check, acceptance limit or detection method.
- Strapping tension, strap width, strap material or the number of bands per coil.
- Coil envelope: outer diameter, bore, strip width, thickness, weight or grade.
- Throughput, cycle time, line speed, and staffing for normal running.
- Which stations are wired together as one line, and the control architecture behind them.
Each of these exists as a document, a drawing or a measured trial. None of them exists inside a 73-second promotional clip, and no still frame can carry them.
Ce que le titre affirme contre ce que les images prouvent
| Réclamer | What the clip supports | Statut |
|---|---|---|
| Vertical coil handling | A coil presented upright on V-shaped rollers, with panels and an operator | Shown as a station |
| Tilting mechanism operating | No continuous upend or tilt cycle appears on screen | Cycle and angle not shown |
| Eliminating edge damage | No edge test, no damaged-edge limit, no edge inspection | Editorial claim only |
| Eliminating telescoping defects | No telescoping check or measurement of any kind | Editorial claim only |
| Labeling (video title) | No label printer or applicator head appears in any frame | Pas observé |
The word “eliminating” carries the whole page. Elimination is a test result, and a test result is a page of data: sample coils, measured edge condition, telescoping limits, a pass or fail line. The clip supplies the machine, not the result.
How the stages appear on screen
Read as a walkthrough, not as a proven process order:
- First ten seconds. A wide view of the hall and several stations, with few coils visible and a quality-inspection-style wall sign. In the sampled frames, the earliest left-hand frame shows no coil at all.
- Roughly 12 to 28 seconds. The vertical coil-handling station. A coil is presented in or near a vertical orientation on V-shaped rollers, with control panels and an operator working the station in the inset view. This is the clip’s most tilting-relevant section, and it is shown statically.
- Roughly 30 to 66 seconds. Horizontal coils on powered roller conveyors under overhead arms and rotating platforms. Film wrapping runs mid-section, and wrapped coils recur afterwards.
- About 70 seconds to the end. Bands on the coil bodies: thin, reflective and green-tinted in the raw view, read as rigid metal strapping.
Treat this order as the shooting order of a promotional edit. One uncut cycle on a single camera with a visible clock is the only footage that can prove sequence, cycle time and integration.
Why tilting matters for slit coil edges
A tilting or upender station exists for one practical reason: coils arrive eye-horizontal, and downstream wrapping, strapping and dispatch often want the coil eye-up or eye-vertical. Turning a coil means the full weight rests on a support surface, and any sliding contact at that moment lands on the coil edge. Slit coil stacks many narrow edges together, which puts more edge at risk than one wide strip does.
That is the engineering case behind the title, and it is a fair case. The two variables that decide the outcome are the coil-support method and how the coil is held while it turns. Neither variable carries a number in this clip.
So the practical reading of the vertical station is modest and useful: it shows how this line receives and supports a coil in the vertical plane. It does not show the turn, the cycle time or the edge result.
Liste de vérification de l'acheteur
| # | Demandez au fournisseur | Ce que cela règle |
|---|---|---|
| 1 | Tilt mechanism design: support method, angle range, drive, and how the coil is restrained while it turns | The edge-contact risk this title is about |
| 2 | Edge-damage test results on coils of your width and thickness, with the pass limit | The word “eliminating”, as a number |
| 3 | Telescoping check: method, acceptance limit, and what the line does at the limit | Whether telescoping is managed or assumed |
| 4 | Strapping and film specification: strap tension target, strap width and material, film type and prestretch | Load security and consumable cost per coil |
| 5 | Coil envelope and measured throughput at your coil size, with staffing | Whether your coils fit and what the line really delivers |
| 6 | One uncut cycle on a single camera with a visible clock | The only footage that can support sequence and timing |
Then work the list in writing:
- Our heaviest and narrowest coils sit inside the quoted envelope.
- The edge-damage result names the test method and the pass limit.
- The tilting design shows how the coil is supported while it turns.
- Telescope detection is documented, with the limit and the response.
- Strap tension and film consumption are quoted per coil.
- We hold one uncut cycle and one layout drawing.
QFP
Does the clip prove that this line eliminates edge damage and telescoping? No. The clip shows coil handling, an active film-wrapping run and strapped coils, and no edge-damage test or telescoping measurement appears anywhere. Write that requirement into the specification and ask for measured results on coils like yours.
Is the vertical coil-handling station a tilt upender? The station presents a coil upright on V-shaped rollers, with control panels and operator access beside it. The footage shows the station, so the machine class is plausible and the mechanism stays unproven. Ask for the design, the angle range and the support method.
What should I request instead of more video? Four documents: the tilt mechanism design, the edge-damage test result on your coil range, the telescoping check with its limit, and the strap and film specification with consumption per coil. Add one uncut cycle with a visible clock when you want sequence and timing.
Lecture connexe
- Ligne automatique d'emballage de bobines — the line family this clip belongs to.
- Redresseur de bobine — the re-orientation station behind the title’s tilting question.
- Hydraulic upender and tilter drives — the drive side of the same handling step.
- Machine d'emballage de bobines d'acier — the film-wrapping stage shown on the conveyor.
- machines de cerclage de bobines d'acier — the band visible on the coils at the end of the clip.
- Cercleuse automatique — strapping equipment of the same class.
Suivant
Send the supplier your coil mix: outer diameters, bores, strip widths, thicknesses, grades and daily volumes. Every figure is yours to supply, because the clip supplies none.
Ask for the tilting design, the edge-damage result on your coil range, the telescoping check and its limit, and the strap and film specification with consumption per coil. Add measured output and staffing from a reference installation. Then ask for one uncut cycle with the clock running, and a demonstration on one of your own coils. Use the page contact to start that exchange.
Dernière révision : 2026-09-21
Publié le : 20 avril 2026