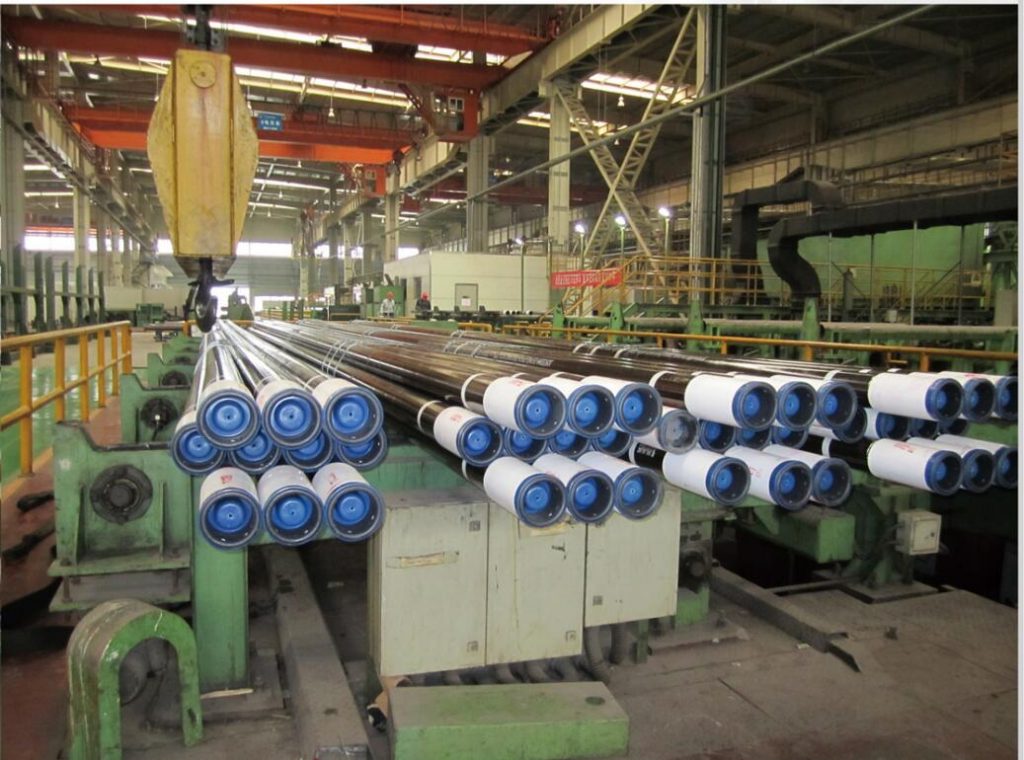
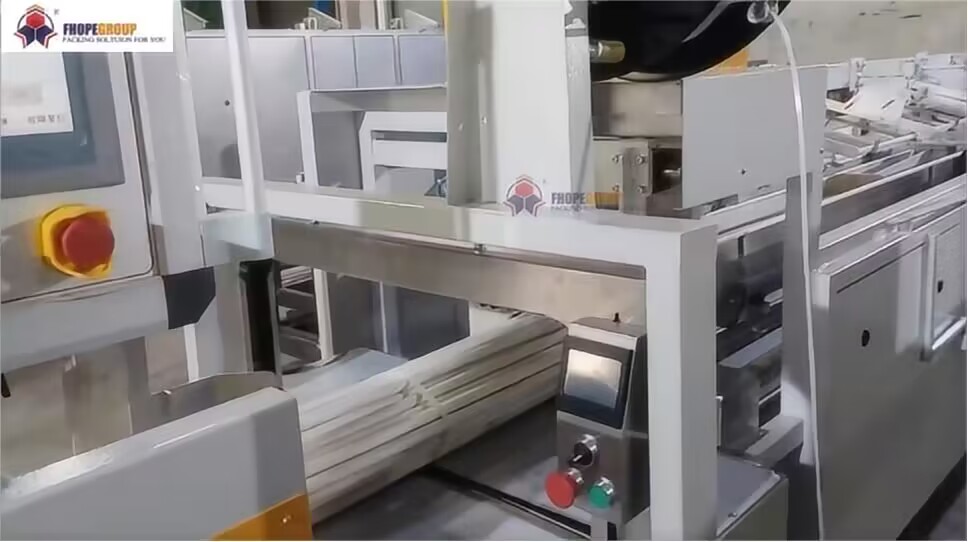
خلاصه اجرایی A high-capacity steel tube bundle packing line automates the end-of-line cycle from the mill run-out table to finished storage. It counts finished round, square, or rectangular tubes into pre-calculated rows, forms them into tightly interlocked hexagonal or square bundles, clamps them under calibrated hydraulic pressure, and applies circumferential steel strapping for secure maritime or flatbed transport. The featured installation handles heavy-wall round tubes from 114.3 to 323.9 mm OD, profile tubes up to 250 × 250 mm, and delivers finished bundle packs up to 16 m in length weighing up to 13,000 kg.
فهرست مندرجات
- Process Breakdown & Motion Sequence
- Stations of a Tube Bundle Packing Line
- Technical Specifications & Engineering Envelope
- Line Balancing and Takt Calculation
- چک لیست انتخاب مهندسی
- System Controls, Machine Safety & Guarding
- سوالات متداول مهندسی
- System Sizing & Project Consultation
- خواندن مرتبط
- منابع و مراجع
Process Breakdown & Motion Sequence
The packing line is constructed on a reinforced structural steel frame finished in industrial safety polyurethane coatings, incorporating dual-drive roller conveyors, hardened lateral guide stops, and high-load hydraulic/pneumatic actuation cylinders. An integrated PLC console with visual status towers coordinates motion interlocks along the entire packaging envelope.
+-------------------------------------------------------------------------------------------------------+
|                                    TUBE BUNDLE MOTION SEQUENCE                                        |
+-------------------+      +-------------------+      +-------------------+      +--------------------+
| 1. Infeed Run-Out | ---> | 2. Layer Charging | ---> | 3. Hexagon Form   | ---> | 4. Auto Strapping  |
| Roller indexing & |      | Overhead transfer |      | V-bed closing &   |      | Circumferential    |
| tube rejection    |      | into accumulation |      | hydraulic clamp   |      | index & outfeed    |
+-------------------+ +-------------------+ +-------------------+ +--------------------+- 0 to 15 s (Infeed & Buffer Staging). Long-length finished tubes enter the lateral accumulation magazine on the feed ramp. Heavy-duty indexing arms isolate individual tubes while baseline quality sensors verify alignment against mechanical reference stops.
- 20 to 30 s (Overhead Transfer & Layer Grouping). A heavy-wall hollow structural section is engaged by the overhead transfer carriage. The overhead gantry transverses smoothly across the primary machine centerline, indexing the tube into the accumulation pocket.
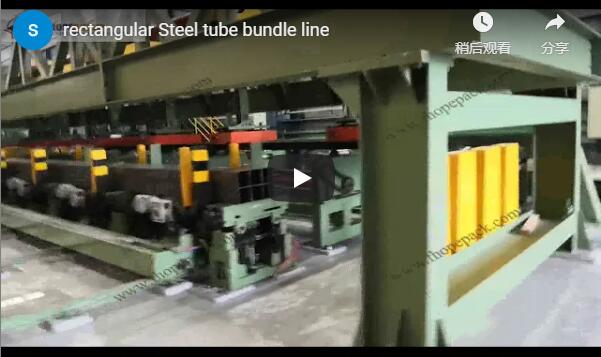
- 35 to 50 s (Metering and Cross-Feed Indexing). The mechanical conveyor bed indexes forward via segmented, grooved rollers. Pneumatic kickers meter tubes row by row under chevron-striped retaining arms to eliminate surface-to-surface impact scarring and prevent tube overlapping.
- 55 to 75 s (Buffer Stabilization & Sensor Verification). Infeed accumulation racks balance the cycle between the continuous upstream tube mill and batch packing stations. Laser through-beam sensors scan tube presence across the full bed width.
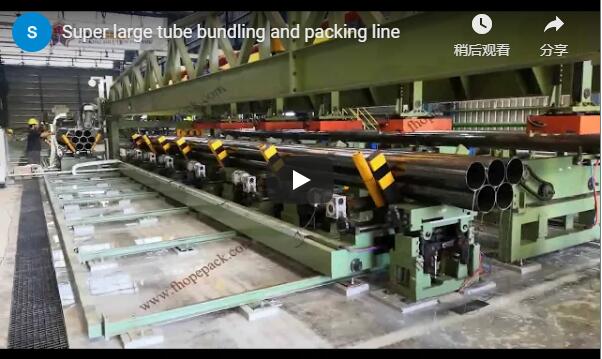
- 75 to 95 s (Long-Span Roller Conveyance). Heavy tubular products advance along blue structural steel support trestles. Lateral guide rollers maintain axial tracking across spans up to 16 m, preventing lateral fish-tailing and excessive sag.
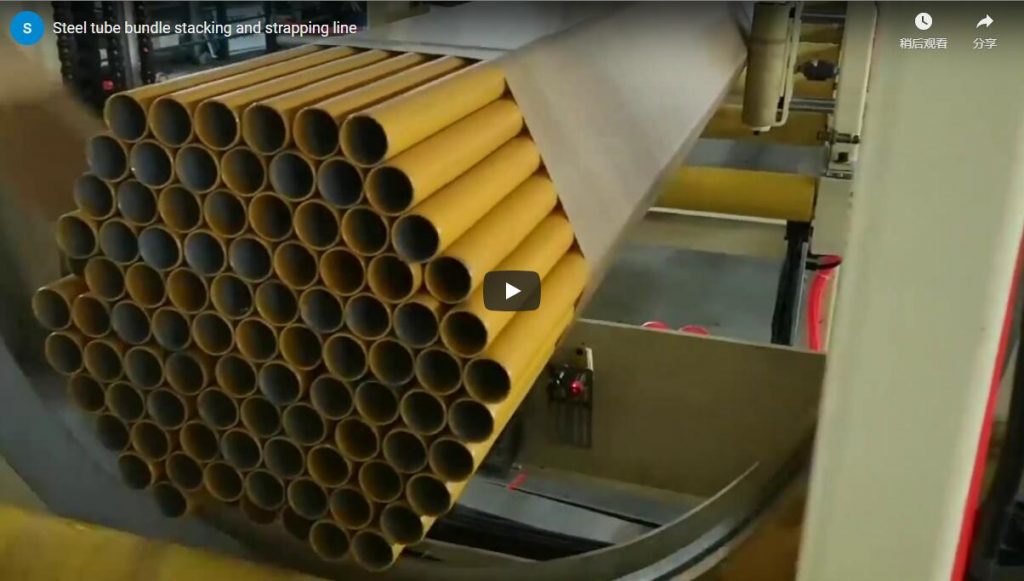
- 100 to 135 s (Hexagonal Formation Bed Entry). Counted tube layers transition from the horizontal accumulation tier down into the heavy-duty, roller-lined V-shaped forming pocket, naturally settling into a dense, nested hexagonal pattern.
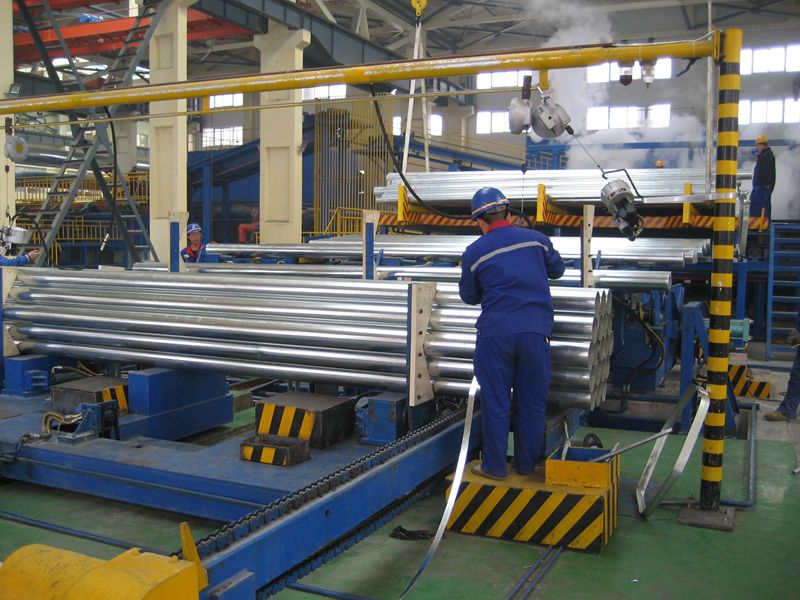
- 140 to 145 s (Pre-Clamping Alignment). The nested bundle rests within the adjustable V-station. Technicians verify mechanical boundary clearances and tube end flushness before high-pressure hydraulic side and top clamps engage.
- 150 to 155 s (Hydraulic Squeeze & Bundle Compaction). Opposed hydraulic forming arms swing inward at controlled speed. The dual cylinders exert uniform radial pressure to lock the loose tube geometry into an unyielding, rigid structural cluster.
- 160 to 165 s (End-Face Finalization & Strapping Clearance). With the clamping jaws locked at dead-center hydraulic pressure, the compact bundle passes final end-face verification before transferring downstream to the automatic high-tension steel strapping machine.
Stations of a Tube Bundle Packing Line
Tubes discharge continuously from the mill cooling bed or cut-off station onto the run-out roller table. The automated packing line transforms individual pieces into dense, rigid bundles optimized for single-pick crane lifting and damage-free transit.
| ماژول ایستگاه | Primary Function & Operating Mechanism |
|---|---|
| Run-Out Conveyor & Reject Station | Receives uncut or single lengths from the mill; integrated pneumatic kickers divert off-spec tubes to reject bins. |
| Pick-Up & ID Air Blowdown | Singulates tubes with polyurethane indexing fingers; dual-side compressed air nozzles evacuate internal water and scale. |
| End Alignment & Optical Counting | Roller tables drive tubes against a solid carbide end-stop to achieve flush end faces; optical sensors count tubes into programmable recipes. |
| Electromagnetic Layer Stacking | Heavy-duty electro-permanent magnetic Chuck beams pick complete rows and lower them into the pocket with controlled acceleration. |
| V-Shaped Bundle Forming Bed | Adjustable angled beds form symmetric hexagonal, square, or rectangular profiles with heavy hydraulic side-confinement arms. |
| High-Tension Steel Strapping | Fully automated indexing strapping heads apply 25 mm or 32 mm high-tensile steel straps with double-notched seal or sealless joints. |
| Outfeed Chain Stacker & Buffer | Lateral drag-chain conveyor transfers finished bundles to an automated 5-tier crane pickup magazine. |
The bundle forming cradle incorporates motorized lead-screw adjustment to switch between hexagonal configurations (e.g., 3-4-5-4-3 or 4-5-6-5-4 nests) and rectangular matrices via PLC recipe selection.
Technical Specifications & Engineering Envelope
| پارامتر های فنی | Engineering Range & Machine Capacity |
|---|---|
| Applicable Cross Sections | Round hollow sections, square, and rectangular structural tubing |
| Round Tube Outer Diameter (OD) | 114.3 میلی متر تا 323.9 میلی متر (4.50 اینچ تا 12.75 اینچ) |
| Square Tube Dimensions | 90 × 90 میلیمتر تا 250 × 250 میلیمتر |
| Rectangular Tube Dimensions | 80 × 100 میلیمتر تا 200 × 300 میلیمتر |
| ضخامت دیوار لوله | 3.0 میلی متر تا 12.7 میلی متر (0.12 اینچ تا 0.50 اینچ) |
| Hexagonal Bundle Envelope | Width: 450 to 1,100 mm; Height: 350 to 1,000 mm |
| Square/Rectangular Bundle Envelope | Width: 350 to 950 mm; Height: 300 to 800 mm |
| Individual Tube Length | 4.5 m to 16.0 m (14.7 ft to 52.5 ft) |
| Maximum Total Bundle Weight | کیلوگرم 13,000 (28,660 پوند) |
| Total Outfeed Footprint | Approximately 43 m (including strapping zone and accumulation beds) |
| نوع سر تسمه دار | Automatic heavy-duty heads for 25 mm and 32 mm high-tensile steel straps |
| معماری اتوماسیون | Siemens S7-1500 / Allen-Bradley ControlLogix PLC with 15-inch color HMI |
Line Balancing and Takt Calculation
The throughput capacity of the packaging line is engineered to match or exceed the maximum production output of upstream high-frequency welding (HFW) or seamless sizing mills.
           Upstream Mill Output: 10 tubes / min
                           │
                           ▼
          Bundle Target Size: 60 tubes / bundle
                           │
   ┌───────────────────────┴───────────────────────┐
   │                                               │
   ▼                                               ▼
Batch Filling Cycle:                           Station Time Budget:
60 ÷ 10 = 6.0 min (360 s)                      < 360 s (Independent)
For an operational baseline with an upstream mill output rate of 10 tubes per minute building bundles of 60 tubes:
- Net Bundle Formation Takt:
60 tubes ÷ 10 tubes/min = 6.0 minutes (360 s)
Because each processing module operates simultaneously on consecutive bundles, each sub-cycle must complete well within this 360-second window:
- Layer Building & Infeed: ~140–180 seconds (continuous cycle).
- Bundle Forming & Hydraulic Clamping: ~45–60 seconds.
- Multipoint Circumferential Strapping: For a 12 m bundle requiring 5 strapping locations, strap cycle time runs ~22 s per band plus indexing travel, consuming ~150–180 seconds total.
Decoupling the strapping machine onto the extended 43 m exit roller conveyor ensures the strapping operation never bottlenecks the V-bed layer charging. The subsequent 5-bundle chain buffer provides up to 30 minutes of operational cushion during overhead crane logistics.
چک لیست انتخاب مهندسی
- Incoming Tube Envelope: Specify minimum/maximum OD, wall thickness range, material grade, and cut lengths (4.5 to 16 m).
- Bundle Geometry: Define nest pattern (hexagonal row count, square, or flat rectangle), target tube count, and maximum gross pack weight (up to 13,000 kg).
- Upstream Process Coupling: Confirm mill cycle rate (tubes/minute), cut-off conveyor line height, and operational duty cycle.
- مشخصات تسمه: Number of straps per bundle, strap pitch centers, strap dimension (25 mm vs. 32 mm), and seal method (sealless punch vs. crimped seal).
- End-Face Alignment Tolerance: Permissible axial tube overhang variation (standard: ±5 mm with automated end-pushers).
- Facility Logistics & Footprint: Available clear floor length (minimum 43 m linear run recommended), transfer side (drive side vs. operator side), and overhead crane approach zones.
System Controls, Machine Safety & Guarding
Handling bundles weighing up to 13,000 kg with hydraulic side-clamping arms creates severe pinch and crush hazards. Manual intervention inside the clamping cradle while cylinders are energized presents severe risks that must be engineered out of normal production.
   [ Mill Discharge ]
           │
  (Optical Perimeter Light Curtains - Category 4 / PL e)
           │
           ▼
   [ Fully Interlocked Enclosure: Automatic Forming & Squeeze Zone ]
           │
  (Key-Exchange Trapped Interlock System / Category 0 E-Stop)
           │
           ▼
[ Automated Outfeed & Strapping Station ]- Perimeter Physical Guarding: The entire V-forming and clamping area must be enclosed behind 2,000 mm wire-mesh guarding conforming to EN ISO 14120, equipped with Category 4 / PL e safety light curtains and interlocked access gates (EN ISO 14119).
- Hydraulic Safety Architecture: Forming clamping cylinders are fitted with dual-channel pilot-operated check valves and mechanical lock-pins to prevent jaw descent during pressure loss, meeting ISO-13849 1، architecture requirements.
- Zero Energy Lockout (LOTO): Maintenance entry for cradle adjustment, mechanical maintenance, or tube squaring requires total electrical and hydraulic isolation following standard OSHA 29 CFR 1910.147 پروتکل ها
- Automated Squaring Alternative: To eliminate manual end-face adjustment within the clamp zone, the line includes an automated hydraulic end-squaring ram that aligns pipe ends before clamping arms close.
- استانداردهای قابل اجرا: CE conformity is verified under ISO 12100: 2010 (ارزیابی ریسک) و EN 415-10: 2014 (General Requirements for Packaging Machines).
سوالات متداول مهندسی
Q: What tube diameters and wall thicknesses can this bundling system accommodate? A: The system handles round tubes from 114.3 to 323.9 mm OD, square hollow sections from 90 × 90 to 250 × 250 mm, and rectangular profiles from 80 × 100 to 200 × 300 mm. The heavy structural bed accommodates wall thicknesses from 3.0 up to 12.7 mm.
Q: What are the maximum overall dimensions and weight limits for packed bundles? A: Hexagonal bundles can span up to 1,100 mm in width and 1,000 mm in height. Square or rectangular packs reach up to 950 mm in width by 800 mm in height. Maximum tube length is 16 m, with bundle weights supported up to 13,000 kg.
Q: How does the system prevent surface damage on sensitive, coated, or high-finish pipes? A: Conveyor rolls and lateral guide arms are coated with vulcanized polyurethane or ultra-high-molecular-weight polyethylene (UHMW-PE). Infeed transfer relies on electro-permanent magnetic Chuck beams or servo-controlled lowering arms that eliminate free-fall drop impacts.
Q: Can the line run mixed production of round, square, and rectangular tubing? A: Yes. The PLC memory stores multiple recipe profiles. The V-bed forming geometry adjusts automatically via motor-driven positioning screws, switching from hexagonal nesting for round tubes to flat-bottom configurations for square and rectangular profiles without physical tooling teardown.
System Sizing & Project Consultation
Fhopepack custom-engineers complete tube bundle handling and strapping lines tailored to factory footprints and mill speeds:
- Submit Facility Layout & Product Mix: Send your mill layout, tube dimensions (OD, wall, lengths), bundle configurations, and mill line speeds to info@fhopepack.com.
- Receive 48-Hour Technical Proposal: Our mechanical applications team will deliver a comprehensive proposal including cycle-time simulations, footprint dimensions, and equipment bill-of-materials within 48 hours.
- بررسی مهندسی سایت و بررسی رابط کاربری: Our systems engineers evaluate existing run-out tables, bay crane clearances, and utility hookups to confirm seamless physical and electrical integration.
خواندن مرتبط
- خط بسته بندی اتوماتیک برای بسته بندی لوله و پروفیل فولادی
- Automatic Steel Pipe Bundling and Packing Line Solutions
- Heavy-Duty Automatic Steel Tube Strapping Systems
- Field Commissioning Case Study: Slit Coil and Long-Bar Handling Systems
منابع و مراجع
- Line Technical Architecture & Operating Parameters: Fhopepack Tube & Profile Bundling Systems
- Industrial Packaging Machine Safety: ISO 12100:2010 ایمنی ماشین آلات
- Specific Packaging Machine Guarding: EN 415-10:2014 Safety Requirements
- Video Demonstration & Motion Reference: Fhopepack Tube Handling Operations on YouTube
آخرین بررسی: 2026-10-05