خلاصه اجرایی
An automated rectangular steel tube bundle line transfers hollow structural sections directly from the mill run-out conveyor, counts them, verifies individual profile orientation, rotates each tube flat side down (wide face resting horizontally), builds uniform layers into square or rectangular bundles, and executes multi-radial steel strapping under closed-loop hydraulic tension control. Designed for heavy structural mills, this packaging system accommodates rectangular tubes from 80 × 100 mm up to 200 × 300 mm, handling bundles up to 13,000 kg and 16 m in length. The reference engineering calculations below illustrate the packaging process for a 32-tube, 8.7-tonne structural bundle.
فهرست مندرجات
- Why Rectangular Tubes Demand Dedicated Bundling Logic
- System Architecture: Station-by-Station Workflow
- Bundle Stacking and Compaction Kinematics
- Technical Specifications and Capacity Matrix
- Hydraulic Steel Strapping Parameters
- Engineering Calculation: 32-Tube Rectangular Bundle
- Mill Integration and Selection Checklist
- Industrial Safety Standards: EN 415-10 and ISO 12100
- سوالات متداول مهندسی
- Project RFQ and Technical Consultation
- Related Tube Packaging Solutions
- Engineering Standards and References
Why Rectangular Tubes Demand Dedicated Bundling Logic
Unlike circular hollow sections that naturally settle into a stable hexagonal nest through self-alignment, rectangular hollow sections (RHS) have asymmetrical geometry. When exiting the flying cutoff saw, tubes land randomly on either their narrow or wide faces. Stacking unaligned profiles results in interlocking failures, irregular row heights, internal void spaces, and inconsistent perimeter circumferences that cause strapping tension loss during transit.
Manual bundle bench preparation requires operators to physically rotate heavy tubes using pipe wrenches or crane toggles—creating serious ergonomic strain and severe throughput bottlenecks.
An automated rectangular tube packaging line utilizes optical or laser displacement profiling to detect tube orientation on the fly. Pneumatic or servo-driven mechanical flip arms then rotate upright tubes by 90° to ensure all units sit wide face down. Every layer achieves consistent planar flatness, ensuring that strapping tension delivers uniform compressive force directly through the tube sidewalls without causing package skewing.
System Architecture: Station-by-Station Workflow
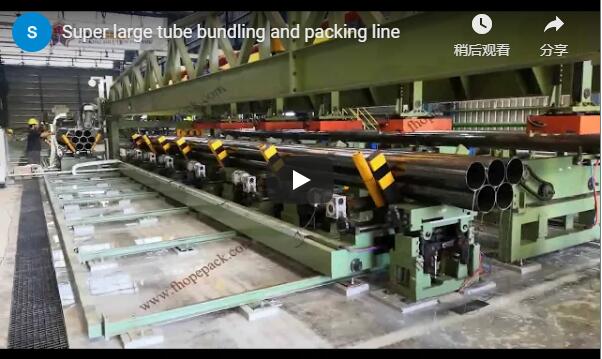
The bundling system integrates downstream from the sizing and cut-off line, synchronizing profile transfer across seven automated stations:
[1. Mill Run-Out & Reject]
         │
         ▼
[2. Tube Separation & Air Purge]
         │
         ▼
[3. Alignment, Counting & 90° Turnover]
         │
         ▼
[4. Layer Pre-Storage & Staging]
         │
         ▼
[5. Overhead Electromagnetic Stacker]
         │
         ▼
[6. Bundle Indexing Car & Strapping Machine]
         │
         ▼
[7. Transverse Outfeed & Buffer Storage]-
Run-Out Infeed and Quality Reject Station Heavy-duty grooved or polyurethane-coated roller conveyors accept cut lengths directly from the mill. Tubes exceeding dimensional or length tolerances are automatically routed to an offload sorting pocket to prevent jam conditions in the stacking cradle.
-
Indexing Pick-Up and Internal Air Purge Walking beam or indexing chain transfers singulate incoming profiles. High-pressure compressed air nozzles blow across internal bores and external profiles to eliminate residual water soluble coolants, scale flakes, and saw shavings, preventing surface corrosion and improving magnetic hoist contact.
-
Servo Alignment, Optical Counting, and 90° Turnover Driven vertical rollers align tube ends against a datum stop. Overhead laser displacement sensors verify profile height versus width. Tubes resting on their narrow face are engaged by servo-driven rotating hooks, turning them 90° so the wide horizontal face forms the base plane.
-
Layer Collation and Pre-Storage Station Tubes accumulate on low-friction transfer beds until the preset row count is achieved. Pneumatic edge aligners square the ends of the row prior to pickup.
-
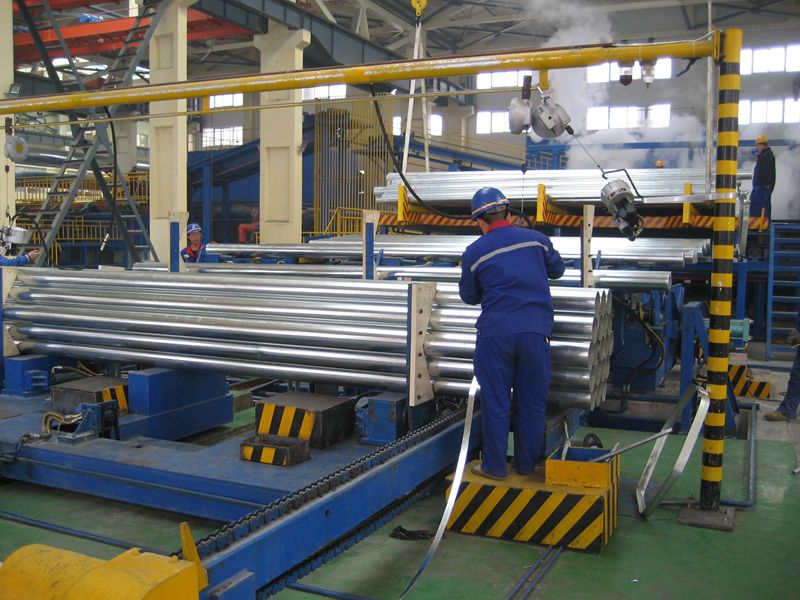
Overhead Electromagnetic Gantry Stacker A rigid gantry crane equipped with continuous electromagnetic chuck plates lifts the complete pre-collated layer. The hoist features closed-loop variable frequency drive (VFD) positioning to smoothly lower each layer into the bundle forming cradle without surface scratching or high-impact shock.
-
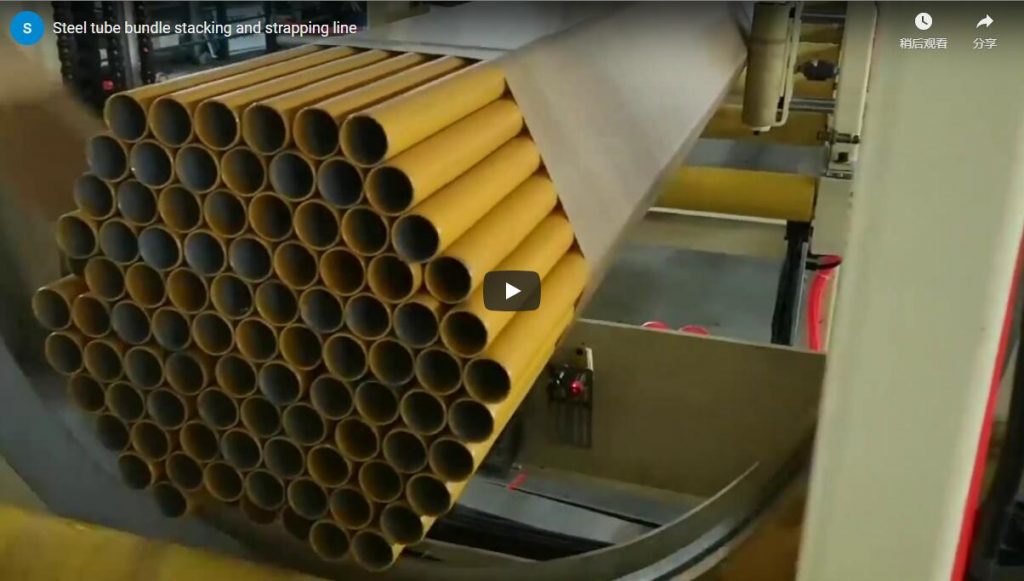
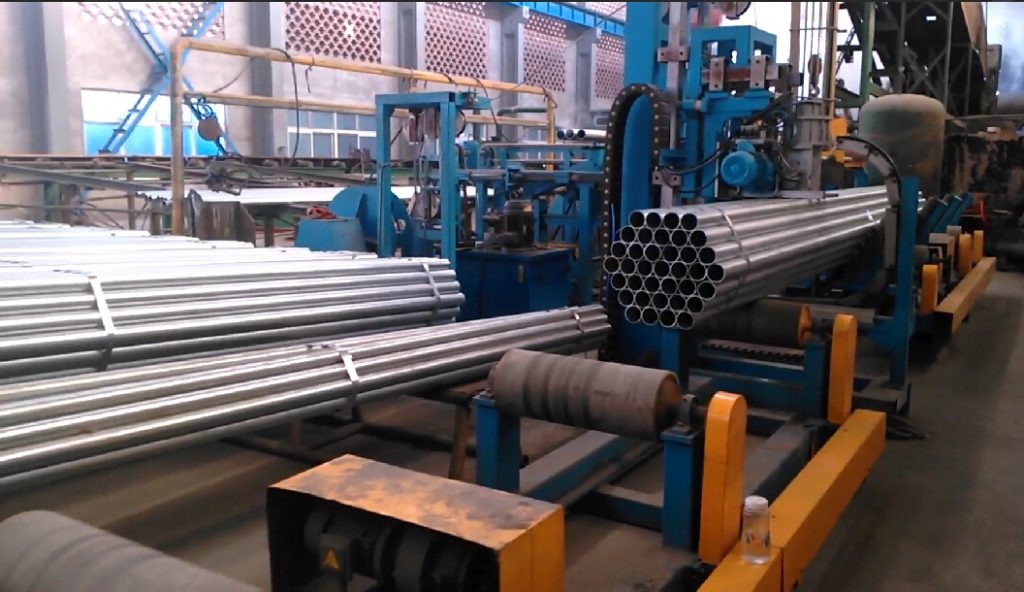
Hydraulic Steel Strapping Station The formed bundle is transferred onto an automated indexing car that moves step-by-step through a stationary heavy-duty strapping head. High-tensile steel strapping is applied, tensioned, notched, and sealed at predetermined intervals.
-
Transverse Bundle Evacuation and Chain Accumulation Strapped bundles are lifted by walking chain transfers onto an external multi-tier storage rack (accommodating up to 5 complete master bundles) awaiting overhead crane dispatch.
The entire cell runs through a centralized PLC architecture with an industrial touch-panel HMI supporting fully automatic, recipe-driven, and manual maintenance modes.
Bundle Stacking and Compaction Kinematics
The bundle forming cradle provides multi-axis mechanical containment to maintain bundle squareness throughout the stacking cycle:
- Lateral Alignment: Dual motorized side-forming guides adjust symmetrically according to the recipe width, clamping each incoming layer with controlled side pressure to eliminate gaps between adjacent tubes.
- Vertical Indexing: Telescoping fork arms or a lowering lift table receive the row directly from the electromagnetic crane. Once the layer is securely released, the stack descends by exactly one profile height.
- Compaction Clamping: Before the strapping cycle commences, hydraulic overhead down-pressure platens and lateral compactor stoppers lock the stacked array under high clamp force, eliminating internal friction slip before the steel straps are applied.
Technical Specifications and Capacity Matrix
| پارامتر | مشخصات متریک | یادداشت های مهندسی |
|---|---|---|
| Rectangular Tube Outer Dimensions | 80 × 100 میلیمتر تا 200 × 300 میلیمتر | Wide-side down packaging configuration |
| ابعاد لوله مربعی | 90 × 90 میلیمتر تا 250 × 250 میلیمتر | Symmetrical layer configurations |
| Round Pipe Capabilities | Ø 114.3 mm to Ø 323.9 mm | Requires auxiliary modular hexagon nesting guides |
| ضخامت دیوار لوله | 3.0-12.7 میلی متر | Suitable for structural and line pipe grades |
| محدوده طول لوله | 4.5-16.0 متر | Outfeed carriage equipped with multiple idle support bogies |
| Max. Bundle Cross Section | 950 میلیمتر (W) × 800 میلیمتر (بالا) | Rectangular / square finished master bundle |
| Max. Hexagon Bundle Envelope | 1,100 میلیمتر (W) × 1,000 میلیمتر (بالا) | For round pipe packaging setups |
| Maximum Master Bundle Weight | ۲۰۰۰ کیلوگرم (۲ تن) | Heavy-duty steel chain conveyor design rating |
| Main Outfeed Conveyor Run | تقریبا. 43 متر | Integrated with traversing indexing strapping carriage |
Hydraulic Steel Strapping Parameters
Master bundles are bound by high-tensile steel strapping to resist dynamic rail and maritime transit loads:
| جزء | تنظیمات استاندارد | Dynamic Range / Option |
|---|---|---|
| Strap Material & Width | High-tensile steel, 32 mm | گزینههای ۸۰۰ میلیمتر یا ۱۰۰۰ میلیمتر |
| ضخامت بند | 0.8-1.0 میلی متر | Standard cold-rolled strapping stock |
| Strap Joint Mechanism | Double-notch crimp seal | Seal efficiency ≥ 85% of strap break load |
| Tensioning Force Range | 7,000-18,000 نیوتن | Closed-loop hydraulic proportional valve control |
| Strap Feed / Retract Speed | 2.0-3.0 متر بر ثانیه | Low-friction hardened strap shoot track |
| Primary Hydraulic System | Working pressure: 8.0–9.0 MPa | Maximum pump relief setting: 10.0 MPa (100 bar) |
| Hydraulic Cooling Media | Integrated water-cooled heat exchanger | Oil temperature maintained at ≤ 45 °C |
The stationary strapping station applies straps along the length of the package as the servo-driven bundle carrier indexes the bundle through the strapping portal.
Engineering Calculation: 32-Tube Rectangular Bundle
Tube Baseline Parameters
- سطح مقطع: 200 mm (wide face) × 100 mm (narrow face)
- Nominal Wall Thickness (t): ۶۰ میلیمتر
- طول (L): 12.0 متر
- گرایش: Flat side down (200 mm horizontal base)
Structural Mechanics and Mass Verification
| گام | Design Formula / Logic | Computed Result |
|---|---|---|
| Effective Cross-Section Area (A) | A ≈ 2 × t × [(W – t) + (H – t)] | 2 × 5 × (195 + 95) = 2,900 mm² |
| Linear Mass (m’) | m’ = A × ρ_steel (ρ = 7,850 kg/m³) | 2,900 × 10^-6 × 7,850 ≈ 22.77 kg/m |
| Single Tube Net Weight (m_tube) | m_tube = m’ × L | 22.77 × 12 ≈ 273.2 kg |
| پیکربندی ردیف | 4 tubes wide × 200 mm base | Finished row width: 800 mm |
| Column Layering | 8 rows high × 100 mm vertical height | Finished stack height: 800 mm |
| ماتریس بسته | 4 columns × 8 layers | 32 total tubes per master bundle |
| Gross Bundle Mass (M_gross) | M_gross = 32 × 273.2 kg | ۲۰۰۰ کیلوگرم (۲ تن) |
                       800 mm wide
         ┌──────┬──────┬──────┬──────┐
 Layer 8 │ 200  │ 200  │ 200  │ 200  │ 100 mm
         ├──────┼──────┼──────┼──────┤
 Layer 7 │      │      │      │      │ 100 mm
         ├──────┼──────┼──────┼──────┤
           ...    ...    ...    ...
         ├──────┼──────┼──────┼──────┤
 Layer 1 │      │      │      │      │ 100 mm
         └──────┴──────┴──────┴──────┘
                  800 mm high
تحلیل مکانیکی: The resulting 800 × 800 mm bundle envelope with a total weight of 8,742 kg sits safely within the system limit of 950 × 800 mm cross section and 13,000 kg total payload.
Crucially, because all tubes are confirmed flat side down, every layer sits flush at exactly 100 mm increments. A single uncorrected vertical profile (resting on its 100 mm side) would create an uneven 200 mm point load in that layer, generating a step discontinuity that prevents the 32 mm steel strap from applying uniform compressive preload across adjacent tubes.
Mill Integration and Selection Checklist
When engineering an automated bundle line for a high-frequency ERW or structural hollow-section mill, provide the following operational parameters:
- Profile Geometry Spectrum: Full matrix of square, rectangular, and round ODs; nominal wall thickness range (t_min to t_max); and steel grades (yield strength affects spring-back during strapping).
- Product Length Distribution: Minimum and maximum mill cut lengths, including off-line test sampling frequencies.
- Master Packaging Geometries: Desired layer configurations (e.g., 3 × 3, 4 × 6, 4 × 8), tube counts, and maximum single-bundle weights.
- مشخصات تسمه: Preferred strap gauge (25 mm vs. 32 mm), target strap count per pack, and minimum edge distance for the leading/trailing strap bands.
- Continuous Mill Speed: Nominal output rate in tubes per minute at the shortest cut length to ensure line cycle-time compatibility.
- Downstream Integration Requirements: Inclusion of protective film wrapping, automatic weight scale integration, barcode tag printing and welding, or multi-bundle stacking tables.
Industrial Safety Standards: EN 415-10 and ISO 12100
Automated steel tube bundling installations present serious mechanical, hydraulic, and pinch hazards. The system is engineered to satisfy the following safety mandates:
- انطباق با EN 415-10: Governs safety for strapping machines and associated handling systems. Covers safety interlocks on strap shoot tracks, dual-channel emergency hydraulic dump valves, and zero-energy pneumatic lockouts.
- ISO 12100 Risk Assessment: Mitigates mechanical crush risks posed by traveling electromagnetic stackers, clamping jaws, and indexing carriages. The line is enclosed by perimeter interlocked safety mesh fencing (2,000 mm height) with safety light curtains at the outfeed stations.
- جداسازی عملگرها: Routine operating tasks are handled via the central control console. All maintenance access gates incorporate trapped-key interlocks conforming to ISO 13849-1 (Category 4, PL e) with integrated lockout-tagout (LOTO) isolation points.
سوالات متداول مهندسی
Q: How does the system detect whether an incoming profile is positioned horizontally or vertically? A: A multi-point laser triangulation sensor array positioned above the roller alignment bed continuously measures profile height and top surface width. When the sensor registers a narrow edge profile (H > W), the PLC triggers a set of rotating flip arms to turn the profile 90° flat side down before the tube enters the layer collation buffer.
Q: Can this packaging line handle standard round tube bundles? A: Yes. The cradle side-forming guides incorporate modular bolt-on 60° angular nesting shoes that support hexagonal packing arrays for round tubes ranging from Ø 114.3 mm to Ø 323.9 mm. Recipes switch automatically via HMI profile selection.
Q: Why is double-notch crimping specified over seal-less friction or micro-welded joints? A: Double-notch crimp seals provide robust resistance against dynamic shock loads and environmental exposure encountered during heavy intermodal transport. In heavy structural bundling applications (up to 13,000 kg), notched seals ensure joint integrity up to 85% of parent strap break strength without the heat-affected zone embrittlement risks that can occur with welded strap methods.
Q: What machine standard governs line certification for overseas shipment? A: The system is designed and certified under EN-415 10، (packaging and strapping equipment safety), with system-wide mechanical risk evaluations meeting ISO 12100 and electrical architectures built to IEC-60204 1.
Project RFQ and Technical Consultation
To integrate an automated bundling and strapping cell into your structural mill line:
- Submit Mill Data: Send dimensional matrices, length variations, target bundle recipes, and mill cycle times to info@fhopepack.com.
- بررسی برنامه: FHOPE engineering will run a dynamic cycle-time simulation and calculate equipment layout footprints.
- Turnkey Proposal: A technical proposal, 2D/3D plant footprint drawing, and detailed line quotation will be delivered within 24 to 48 hours.
Related Tube Packaging Solutions
- Automatic Steel Tube Bundle Packing Line
- Automatic Steel Tube Strapping Machine System
- Horizontal Orbital Wrapping System for Bundled Profiles
- Heavy-Duty 32 mm Steel Strap Application Portal
Engineering Standards and References
- EN 415-10: Safety of Packaging Machines – Part 10: General Requirements
- ISO 12100: 2010: Safety of Machinery – Basic Concepts and General Principles for Design
- ASTM A500 / EN 10219: Cold-Formed Welded Structural Hollow Sections
- FHOPE Design Manual: Automatic Pipe Bundling & Hydraulic Strapping Systems (2026 Edition)
Last Technical Review: 2026-10-19