خلاصه اجرایی This engineering guide outlines an automated packing line architecture designed for narrow non-ferrous slit coils, including copper, aluminium, and brass alloys. Utilizing a heavy-duty indexing turnstile table, an overhead eye-through gantry grab, an automated radial PET strapping head, a high-speed orbital wrapping ring, and a pallet stacking module, this system prevents surface scuffing, edge crushing, and telescoping. Every contact face is shielded with Shore 85A polyurethane, and all dynamic motions utilize S-curve speed profiling to safeguard delicate strip surfaces while sustaining high line throughput.
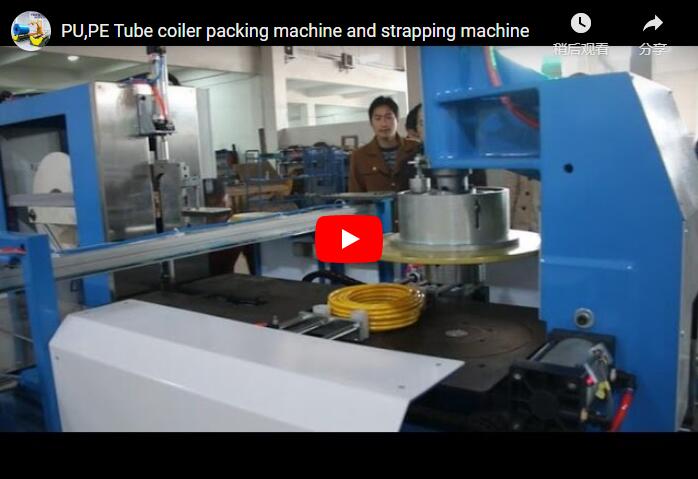
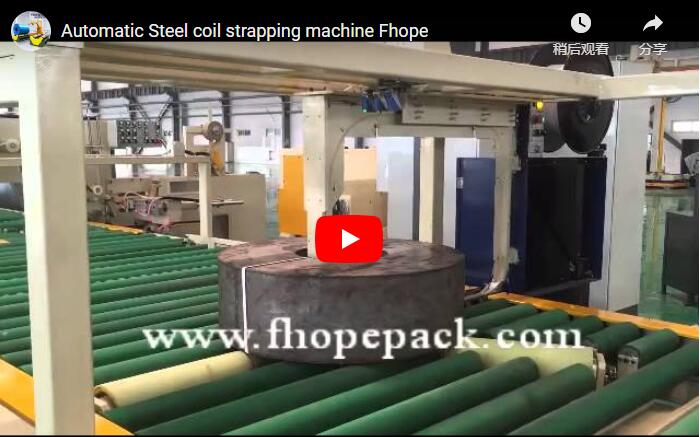
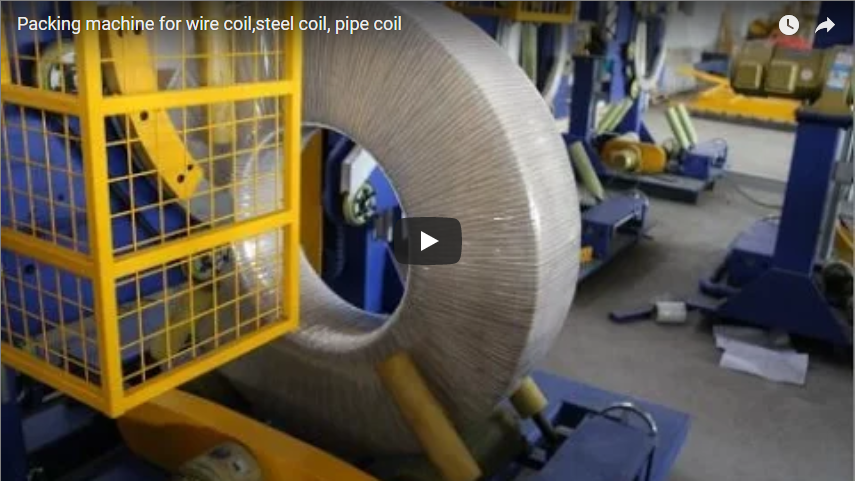
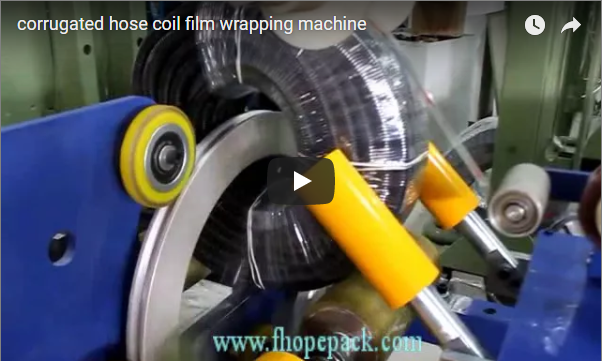
توجه داشته باشید: The video above demonstrates the core mechanical framework — turnstile buffering, gantry transfer, radial strapping, and orbital eye-through stretch wrapping. For non-ferrous coil processing, this architecture is customized with low-friction polyurethane rollers, digital strap-tension regulation (300–850 N), and soft-clamping grippers to protect sensitive metal surfaces.
Why Non-Ferrous Coils Need a Dedicated Packing Line
Slit coils of copper, brass, and aluminium possess distinct mechanical characteristics that make conventional carbon-steel packaging lines unsuitable:
- High Surface Vulnerability: Soft strip surfaces and mirror-finish cold-rolled gauges scratch or gall under direct steel-to-metal contact.
- Low Yield Strength at Strip Edges: High-tension strapping heads built for heavy steel coils readily crush the outer wraps of annealed copper or thin aluminium, rendering the coil ends unusable.
- Telescoping and Ovality Risks: Without controlled lateral clamping and smooth S-curve acceleration, narrow slit coils easily telescope or shift out of round during indexing.
A dedicated non-ferrous packaging system replaces rigid carbon-steel contact points with Shore 85A polyurethane (PU) or UHMW-PE liners, lowers strapping tension through closed-loop servo feedback, and maintains an eye-vertical (eye-to-sky) orientation throughout the line to ensure complete geometric and aesthetic integrity.
[Slitter Recoiler Exit]
          │
          ▼
[Indexing Turnstile Buffer] (PU-Padded Horns / S-Curve Drive)
          │
          ▼
[Gantry Crane Pick & Place] (PU-Lined Expanding Mandrel / Eye-to-Sky Transfer)
          │
          ▼
[Radial Strapping Station] (Servo-Tensioned PET / 350–850 N Limit)
          │
          ▼
[Orbital Ring Stretch Wrapper] (Eye-Through Helical Wrap / 150–200% Pre-Stretch)
          │
          ▼
[Scissor-Lift Pallet Stacking] (Padded OD Centering / Automated Wood Spacer Insertion)
          │
          ▼
[Wrapped Pallet Discharge]
Non-Ferrous Material Characteristics & Machine Parameters
Processing different alloys requires tailored handling parameters to prevent scrap deductions:
| ماده | Alloy Grade (Typical) | قدرت تسلیم (MPa) | حساسیت سطحی | Strapping Tension (N) | پوشش سطح تماس |
|---|---|---|---|---|---|
| مس الکترولیتی | C11000 (Annealed) | 60 - 120 | Critical (edge crush, galling) | 350 - 550 | Shore 85A Polyurethane |
| کارتریج برنجی | C26000 (Half-hard) | 200 - 350 | High (scratching, staining) | 500 - 750 | Vulcanized NBR / PU |
| آلومینیوم خالص | 1050 / 1100-O | 35 - 85 | Extreme (denting, ovalization) | 300 - 450 | Soft Cast PU / Felt Buffer |
| آلیاژ آلومینیوم | 6061-T6 / 5052-H32 | 190 - 275 | Medium-High (scuffing) | 600 - 850 | UHMW-PE / PU Rollers |
| Nickel Silver / CuNi | C75200 / C70600 | 150 - 300 | High (pickup, edge damage) | 500 - 800 | Shore 90A Polyurethane |
Because high-grade copper coil commands high material value per ton, surface damage that results in downgrading or remelting can cause a direct loss of 10% to 20% of product value. Controlled strap tension and non-marking contact surfaces prevent these losses.
Industrial Market Applications
Non-ferrous coils processed through this automated turnstile packaging line serve critical industrial supply chains:
- برق و قدرت: High-conductivity busbars, transformer foil windings, generator laminations.
- Electronics & EV: Lithium-ion battery tabs, connector terminals, lead frames, shielding enclosures.
- معماری: Zinc and copper roofing strips, architectural facade cassettes, rainwater gutters.
- مدیریت حرارتی: Compact automotive radiator fins, HVAC heat exchanger coils, continuous tube strip.
Each downstream manufacturing process demands coils with perfectly flat edges, zero surface oxide contamination, and uniform inner diameters for smooth payoff reel uncoiling.
How the Automated Packing Line Works
The line layout processes narrow slit coils directly from the slitter exit in an eye-to-sky (vertical-axis) position.
       [Radial Strapping Station]
                  │
[Turnstile] ──► [Roller Conveyor] ──► [Orbital Wrapper] ──► [Pallet Stacking Station]
     ▲
(Slitter Exit)
Step 1 — Turnstile Indexing & Batch Buffering
Slit coils discharged from the slitter are received onto a heavy-duty, 2-arm or 4-arm rotating turnstile table. Each arm features thick polyurethane wear pads. Driven by an inverter-controlled motor with smooth acceleration ramps, the turnstile indexes batches of coils smoothly into position without relative sliding between strip layers.
Step 2 — Overhead Gantry Transfer
A motorized gantry transfer crane moves over the selected turnstile arm. An expanding inner-diameter (ID) mandrel or non-marking scissor-jaw gripper lowers into the coil eye. The gripper expands against the inside core with regulated pressure, picks the coil without touching the sensitive outer circumference, and smoothly sets it onto the powered roller conveyor line.
Step 3 — Automated Radial PET Strapping
The coil advances to the automated strapping station. An indexing turntable rotates the coil in 90° or 120° increments while an automated strapping head feeds smooth polyester (PET) strapping through the open eye. The closed-loop tensioning drive limits strap pull to 350–850 N (depending on alloy grade) to prevent outer corner crushing.
Step 4 — Eye-Through Orbital Ring Wrapping
The banded coil moves into the high-speed orbital wrapping station. Driven by high-traction PU friction wheels, a vertical rotating ring shuttles stretch film (or VCI anti-corrosion film) through the center bore while the coil turns horizontally on polyurethane-coated cradle rollers. This continuous motion applies a 360° helical wrap around the entire cross-section (ID, OD, and both side faces), sealing the metal against moisture, dust, and transit oxidation.
Step 5 — Scissor-Lift Coil Stacking & Palletizing
The fully wrapped coil advances to the palletizing station. Because the coil remains in the eye-vertical position, no downender tilting is required. An overhead stacking grab picks each coil by its inner bore and deposits it onto a wooden pallet. The PLC calculates the pre-set stack recipe, stacking coils 1 to 6 layers high and automatically allowing operators or pneumatic dispensers to place corrugated or wooden spacer rings between layers.
Step 6 — Finished Pallet Discharge
Completed coil stacks exit onto an accumulation roller conveyor or automated turntable stretch wrapper for full-pallet over-wrapping and labeling, ready for warehouse storage or overseas export container loading.
Surface Protection Mechanisms
| Motion Point | Primary Damage Risk | Engineering Protective Solution |
|---|---|---|
| Turnstile Arm Buffering | Scratches on inner/lower wraps | 10 mm Shore 85A Polyurethane sleeves; variable-frequency S-curve rotational indexing |
| Mandrel Pick & Place | Bore deformation, gouging | Mechanical expanding shoes lined with UHMW-PE; proportional descent speed reduction to ≤ 2 m/min before contact |
| تسمهکشی شعاعی | Edge notch formation, deformation | Digital servo-regulated tension (350–850 N); smooth PET strap replaces sharp steel bands |
| Through-Eye Wrapping | Coil telescoping, core crushing | Low-tension film carriage (150%–200% pre-stretch); dual PU-coated conical support rollers |
| Conveyor Transit | Metal scuffing, friction flats | Heavy-duty steel rollers vulcanized with a 5 mm seamless NBR or polyurethane layer |
Line Throughput & Cycle Time Calculation
The line is engineered to match the cycle times of high-output slitting lines:
| Operation Cycle Step | Standard Time (Seconds) | پارامترهای مهندسی |
|---|---|---|
| Gantry pickup from turnstile | 12 بازدید کنندگان | Proportional descent with laser height verification |
| Conveyor transit to strap station | 8 بازدید کنندگان | Line speed v = 12 m/min, variable acceleration |
| Radial PET strapping (2 radial straps) | 18 بازدید کنندگان | 90° rotational indexing, 9 s per strap band |
| Eye-through orbital stretch wrapping | 20 بازدید کنندگان | Ring speed up to 90 RPM, 55% helical overlap |
| Stacking transfer to pallet | 14 بازدید کنندگان | Automatic stack calculation, soft-touch landing |
| Total cycle time per coil (overlapping) | 45 بازدید کنندگان | Continuous synchronized multi-station flow |
ظرفیت عملیاتی: At 45 seconds net cycle time per coil, output reaches 80 کویل در ساعت. A typical master coil slitting cut yielding 16 narrow coils is cleared, banded, wrapped, and stacked on pallets in approximately دقیقه 12, preventing slitter exit bottlenecks.
Consumable Specifications: Strapping & Stretch Film
1. Polyester (PET) Strapping
PET strap delivers superior shock absorption and elastic recovery compared to rigid steel bands, without staining copper or brass via rust:
- عرض بند: 12.0 میلی متر تا 19.0 میلی متر
- ضخامت بند: 0.60 میلی متر تا 0.85 میلی متر
- Strap Tensile Strength: 4,200 N تا 7,500 N
- ازدیاد طول در نقطه شکستن: 12% to 18% (damps transport shock loads)
- Joint Sealing Method: High-frequency friction weld (joint efficiency ≥ 85%)
2. Orbital Stretch Wrapping Film
- مواد فیلم: 3-layer to 5-layer cast LLDPE or VCI corrosion-inhibiting stretch film
- ضخامت فیلم: 20 میکرومتر تا 35 میکرومتر
- عرض رول فیلم: 100 میلی متر تا 250 میلی متر
- قابلیت پیش کشش: 150% to 250% via motorized power pre-stretch carriage
- Overlap Ratio: Adjustable from 30% to 70% (50% standard for sea freight)
Comparison: Dedicated Non-Ferrous Line vs. Standard Steel Line
| پارامتر طراحی | Standard Steel Coil Line | Non-Ferrous Packing Line |
|---|---|---|
| Primary Strap Type | High-tensile steel band (or heavy PET) | Flexible PET strap only |
| محدوده تنش تسمه کشی | 1,500 نیوتن - 3,500 نیوتن | 300 N – 850 N (closed-loop control) |
| Conveyor Roller Surface | Bare zinc-plated or hardened steel | Seamless Polyurethane or NBR vulcanized |
| Gripper Contact Jaws | Hardened knurled steel teeth | Smooth Shore 85A Polyurethane / UHMW-PE |
| Coil Handling Orientation | Often tilted eye-horizontal to eye-vertical | Maintained Eye-to-sky throughout |
| شتاب دینامیکی | Rapid indexing (high jerk rate) | S-curve acceleration with torque limits |
| حفاظت در برابر اکسیداسیون | Standard stretch film / Kraft paper | VCI anti-corrosion film with eye-through hermetic wrap |
Engineering Selection & RFQ Checklist
When requesting a line proposal, specify the following operating parameters:
- درجه مواد: Copper (OF-Cu, ETP), Brass, Aluminium (1xxx, 3xxx, 5xxx, 6xxx series)
- ابعاد کویل: Inner Diameter (ID), Outer Diameter (OD), Strip Width range (min/max mm)
- Weight Parameters: Minimum and maximum individual slit coil weight (kg)
- Slitting Yield: Number of slit coils produced per slitter parent roll
- الزامات تسمه کشی: Number of radial bands per coil (typically 2, 3, or 4 bands)
- Packaging Layer: Stretch film only, VCI paper + film, or woven composite wrap
- Stacking Matrix: Target pallet dimensions, maximum stack height, and stack weight capacity
- چیدمان کارخانه: Available floor space (length × width), slitter centerline, and power/air drop locations
استانداردهای ایمنی و انطباق
The system incorporates industrial safety interlocks in full compliance with European and international safety directives:
- ISO 12100: 2010: Safety of machinery — General principles for design and risk reduction.
- EN 415-10:2014: Safety of packaging machines — Modular pallet packaging lines.
- EN ISO 13849-1: Safety-related parts of control systems (Category 3, Performance Level d).
- حفاظت محیطی: 2,000 mm steel wire-mesh safety fences with interlocked safety-switch access gates.
- حفاظت از اپراتور: Optical muting light curtains at coil infeed/discharge zones and Category 0 emergency stop pushbuttons at every control station.
سوالات متداول مهندسی
Q: How does the strapping head avoid scratching the outer strip edges?
A: The strapping track uses smooth radius transition guides, and the strap tension is dynamically regulated via an adjustable servo-torque limiter. Contact pads touching the coil face during strap tensioning are fitted with smooth, low-friction polymer cushions.
Q: Can this line handle variable slit widths on the same pallet?
A: Yes. The PLC uses optical laser distance sensors to detect individual coil widths and centerlines dynamically, adjusting the orbital wrapper feed speed and gantry lift stroke automatically without manual changeovers.
Q: Why is the coil kept in the eye-to-sky orientation throughout the packaging line?
A: Transporting and processing narrow slit coils with the eye vertical (axis perpendicular to the floor) eliminates the need for repeated 90° tilting. This removes the risk of strip layer shifting, inner-bore telescoping, and side-drop damage.
Q: Is the system suitable for VCI corrosion-inhibiting film?
A: Yes. The orbital ring carriage accommodates standard 3-inch core film rolls, including stretch VCI film, polyethylene waterproof film, and composite paper-plastic wrap for long-distance maritime export packaging.
Next Step & Technical Proposal
To adapt this turnstile packaging architecture to your plant layout:
- ارسال دادههای تولید: Send your slit coil dimension matrix (ID/OD/Width/Weight) and slitter discharge height to info@fhopepack.com.
- Receive 2D/3D Concept Layout: Our engineering team will supply a complete equipment layout and cycle-time study within 48 hours.
- Site Survey & Integration Review: Coordinate with our automation specialists to verify slitter exit interlocking, floor foundation, and safety fencing requirements.
منابع مهندسی مرتبط
- دستگاه تسمه زنی کویل شکاف دار گردان
- خط بستهبندی کویل مسی دو مرحلهای
- خط تسمه کشی، بسته بندی و انباشت کویل آلومینیومی اتوماتیک
- Slit Coil Automatic Packaging Line
منابع و مراجع صنعتی
- Machine Architecture & Controls: FHOPE Packaging Automation Engineering Department.
- Reference Line Video: YouTube — Slit Coil Automatic Packaging Line.
- Safety Directives: ISO 12100:2010 (Risk Assessment & Reduction); EN 415-10: 2014 (ایمنی ماشین آلات بسته بندی).
- Technical Inquiry Response Window: Standard 48-hour proposal delivery SLA.
- وضعیت سند: Engineering Approved — Release Version v3.4.