خلاصه اجرایی
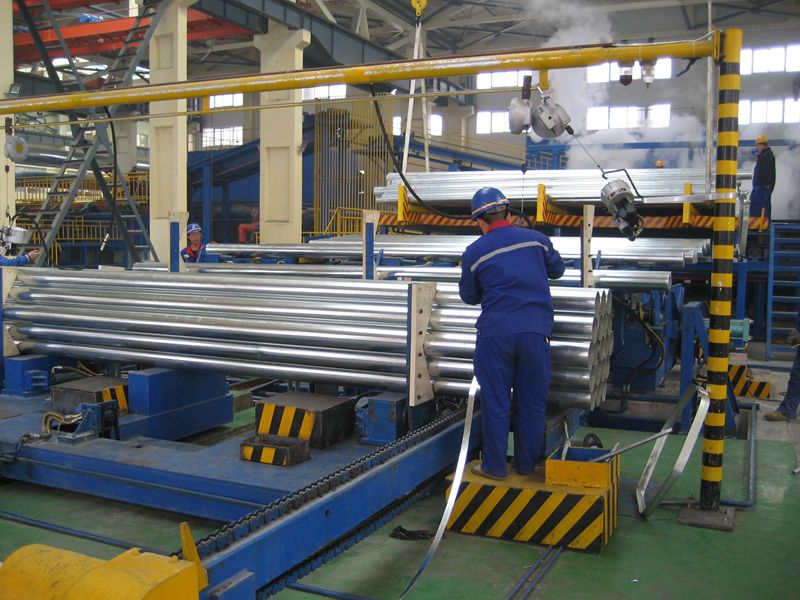
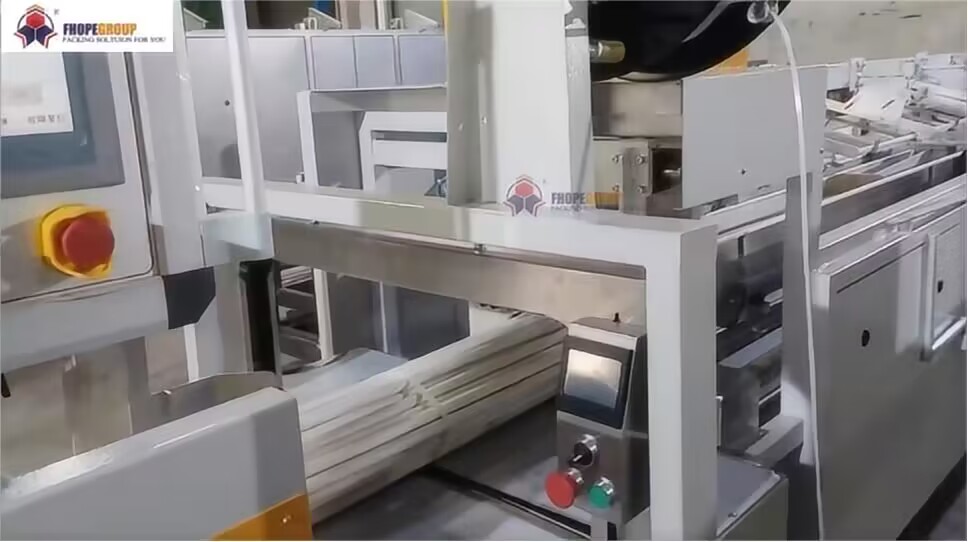
یک خط تسمهکشی لوله چدنی گرهای خودکار، لولههای آماده را میشمارد، آنها را به صورت یک دسته محکم درمیآورد و دسته را در چندین نقطه در امتداد طول آن با تسمههای فولادی میبندد. لوله چدن نشکن سنگین است و پوشش و انتهای نری آن به راحتی آسیب میبیند، بنابراین دسته باید محکم باشد و لولهها نباید روی یکدیگر بغلتند. این صفحه مراحل خط، اندازه تسمه و کشش، طول تسمه و مواردی که قبل از خرید باید بررسی کنید را پوشش میدهد.
فهرست مندرجات
- چرا لوله چدن نشکن را دسته بندی و تسمه بندی کنیم؟
- مراحل خط
- مشخصات دستگاه تسمهکشی
- طول تسمه و زمان تغذیه
- چند تسمه در هر بسته
- چک لیست انتخاب
- ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
چرا لوله چدن نشکن را دسته بندی و تسمه بندی کنیم؟
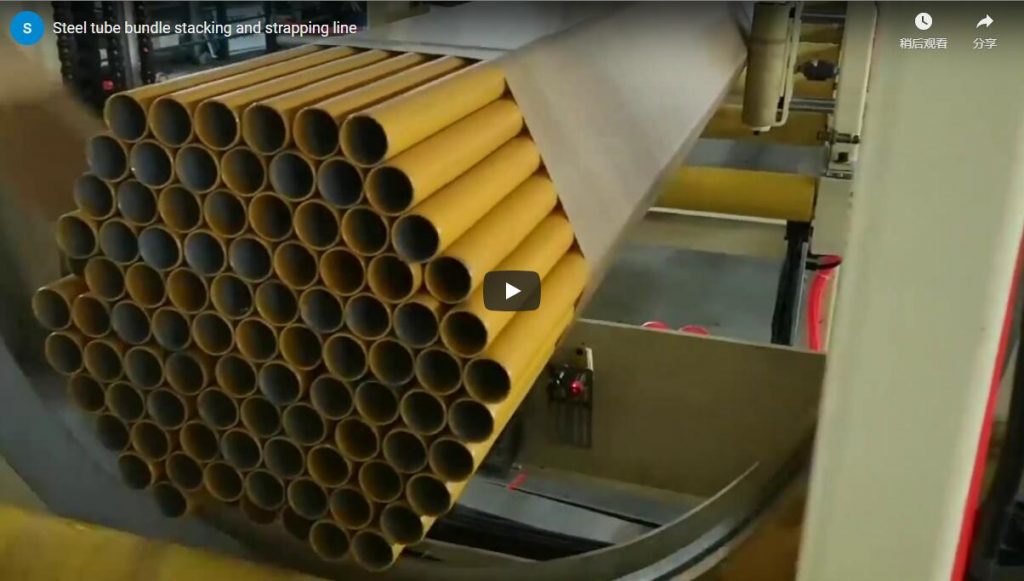
Smaller-bore ductile iron pipe ships in bundles so cranes and trucks handle one unit, not dozens of loose pipes. Loose pipes roll during transit, which chips external zinc or bituminous coatings and dents machined spigot ends.
A counted, formed bundle secured with tensioned steel straps stays mechanically locked from the foundry line to the job-site utility trench. End caps keep dirt and impact damage away from the pipe bore and joints.
For high-speed downstream logistics, bundling lines configure these pipes into stable hexagonal packages. Our bundling stations form bundle widths from 450 mm to 1,100 mm [manufacturer rating], with specific layer configurations confirmed per pipe outer diameter (OD) drawings.
مراحل خط
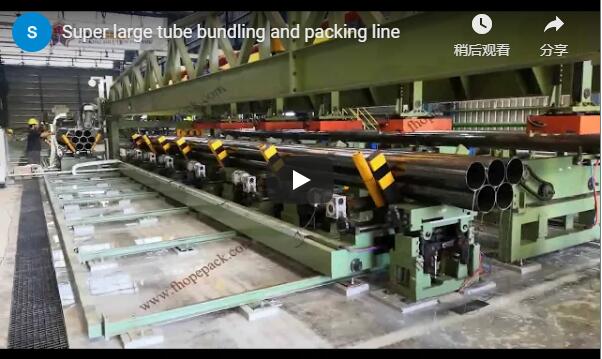
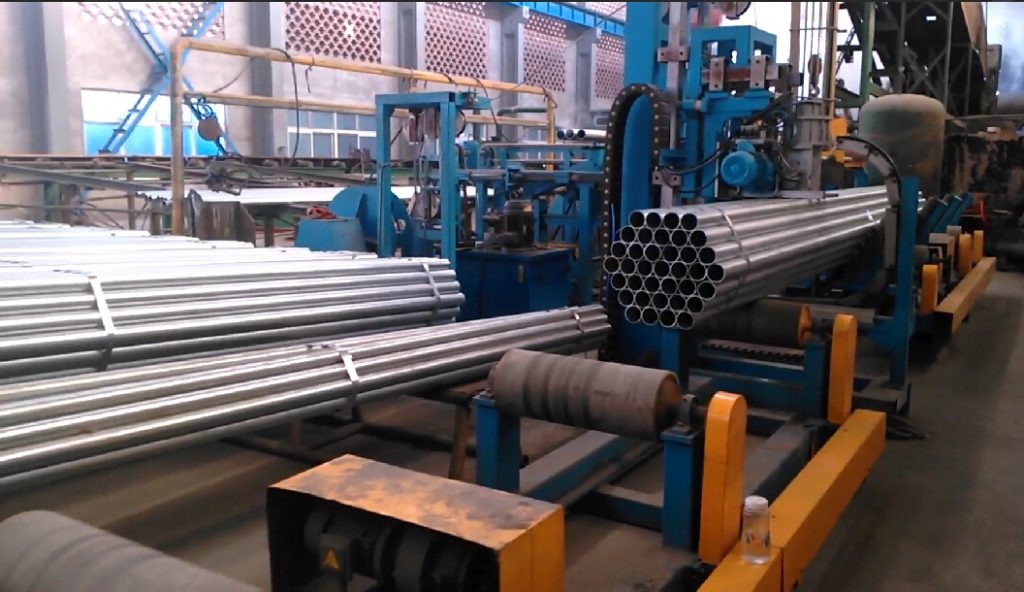
The fully automated finishing and packing cycle proceeds through five synchronized steps:
- بارگذاری و تراز کردن: Individual pipes roll into the storage area; a mechanical striker plate squares and aligns pipe ends to establish a consistent longitudinal datum.
- تعداد: An escapement kick-out mechanism separates and lifts pipes one by one onto the layering index bench, where a fast-response photoelectric sensor counts each pipe to meet the pre-set batch recipe.
- فرم: Counted pipe layers drop into a dedicated forming cradle shaped to the bundle geometry. Lateral stoppers clamp the bundle tight and compress it, eliminating voids.
- بند: The strapping machine remains stationary while a powered bundle carriage indexes the clamped bundle to each programmed strapping position along its length.
- خارج از: The fully strapped bundle transfers to the discharge storage ramp or chain-type bundle stacking magazine for crane or truck pickup.
The complete line is managed through a central touch-screen operator station with automatic, semi-automatic and manual operating modes.
مشخصات دستگاه تسمهکشی
| مورد | Specification [manufacturer rating] |
|---|---|
| مواد تسمه | فولاد کم کربن نورد سرد، آبی و مومکاری شده |
| عرض بند | 25 میلی متر یا 32 میلی متر |
| ضخامت بند | 0.8 میلی متر یا 1.0 میلی متر |
| کشش تسمه | 7,000–18,000 N (continuously adjustable) |
| Seal joint type | Notch type; double seal notch on bundle machines |
| Seal magazine capacity | Approx. 180 seals |
| تسمه تغذیه و سرعت برداشت | 2-3 متر بر ثانیه |
| Strap tensioning speed | 6 متر در دقیقه |
| فشار سیستم هیدرولیک | Design maximum 100 bar, normal working pressure 80–90 bar |
| خنک کننده هیدرولیک | Water-cooled oil circuit heat exchanger |
| تسمه در هر بسته | 5 to 7 straps (standard pattern) |
| پیکربندی ماشین | Stationary strapping head; bundle carriage traverses |
Note: Final bundle configurations, layer geometry, and strapping positions are confirmed upon review of engineering layout drawings.
طول تسمه و زمان تغذیه
Strap length around a hexagonal pipe bundle is calculated as:
Strap length = 6 × (pipes per side − 1) × pipe OD + π × pipe OD
A 19-pipe hexagonal bundle has 3 pipes per side. For a 100 mm OD pipe:
- Straight spans: 6 × (3 − 1) × 100 = 1,200 mm
- Corner arcs: π × 100 ≈ 314 mm
- Loop length: 1,200 + 314 = 1,514 mm per strap (illustrative calculation)
At a feed speed of 2 m/s, that strap is fed in 1.514 ÷ 2 = 0.76 s. Since feeding takes under one second, cycle time is set by bundle indexing, hydraulic tensioning (at 6 m/min) and the double-notch seal stroke, not by feeding.
چند تسمه در هر بسته
The required number of straps across a rigid bundle is determined by length and strapping pitch:
Straps per bundle = bundle length ÷ strap pitch + 1
For example, a 6 m pipe bundle with a standard strap spacing of 1.2 m requires:
6 ÷ 1.2 + 1 = 6 straps
This falls within the 5 to 7 strap range of our bundle machines (illustrative calculation).
پریزها و شیرهای اتصال. Ductile iron pipes have an enlarged bell (socket) end wider than the barrel. Socket-pipe bundles are formed with bells alternating end to end, so the bundle stays parallel and the straps bear on the pipe barrels, not the bells. The forming bed and strap positions are set per pipe drawing.
اتصال و پوشش. A double-notched seal joint retains about 75% of the strap breaking force, so size the strap and band count for the bundle weight with that margin. Where straps bear on zinc, bitumen or polyurethane coatings, cardboard or plastic edge protectors go under the strap; automatic protector applicators are offered on our coil strapping lines, and the option for pipe is confirmed at quote.
The first and last straps sit close to the bundle ends, where bundles spring open first, and the bundle centre stays on the conveyor centre so each strap sits square.
چک لیست انتخاب
Confirm the following six parameters before finalizing an equipment quotation:
- Pipe range: Nominal diameter (DN), actual outer diameter (OD), and barrel length limits.
- Bundle profile: Target pipe count per bundle, grouping pattern, and cross-sectional profile (for example, hexagonal).
- Strap specifications: Preferred steel strap width (25 or 32 mm), thickness (0.8 or 1.0 mm), and target strap pitch.
- Coating and protection: Pipe surface treatment (metallic zinc, bitumen, epoxy, or polyurethane) and requirements for edge protectors.
- ظرفیت خروجی: Target packaging speed in finished pipes per hour or bundles per shift.
- Discharge logistics: Downstream integration with overhead cranes, bundle storage tables, or automated flatbed loading stations.
ایمنی
The line is designed to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for electrical equipment. Primary hazards are moving bundles, the strapping arch and hydraulic tensioning. The line is fenced with guard rails and warning signs, and access is through interlocked gates fitted with emergency stops.
سوالات متداول مهندسی
Q: What strap does the line use? A: Cold-rolled, low-carbon blued and waxed steel strapping, 25 mm or 32 mm wide and 0.8 mm or 1.0 mm thick.
Q: How tight is the strap? A: Strap tension ranges from 7,000 N to 18,000 N, adjusted to the bundle.
Q: How are pipes counted? A: An optical photoelectric switch counts individual pipes as the escapement kick-out arm transfers them to the indexing layer bed.
Q: Does the bundle move or the strapper? A: On standard lines, the strapping machine is stationary while the bundle carriage indexes the bundle through the strapping arch. A stationary head keeps high-pressure hydraulic connections rigid and reliable. A mobile, traveling strapping head option is available for heavy bundle lines where the pipe stack must remain stationary.
مرحله بعدی
- Send your technical project data: Forward pipe DN/OD, pipe lengths, bundle layout patterns, and target line output to info@fhopepack.com.
- پیشنهاد مهندسی: Our engineering team sizes the counting indexer, forming bed, and hydraulic strapping station.
- Formal quotation: We return a complete technical solution and competitive commercial quotation within 24 hours.
خواندن مرتبط
- دستگاه تسمهکشی لوله فولادی خودکار (محصول)
- دستگاه بسته بندی و تسمه کشی لوله فولادی اتوماتیک
- دستگاه تسمهکشی لولههای فولادی (محصول)
منابع
- دستگاه تسمه کش لوله فولادی اتوماتیک
- دستگاه تسمه بند لوله فولادی
- خط بسته بندی اتوماتیک بسته نرم افزاری و پروفیل لوله فولادی
- EN ISO 12100:2010; EN 415-10؛ EN 60204-1
آخرین بررسی: 2026-10-20