خلاصه اجرایی
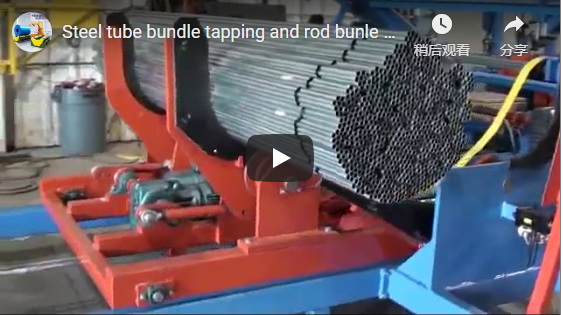
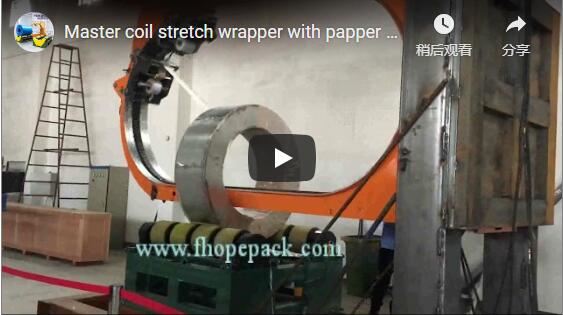
For continuous packaging of linear metal and polymer stock—including steel tubes, structural bars, and extruded profiles—the horizontal orbital stretch wrapper serves as the primary inline protective unit. The bundle advances longitudinally through an orbiting annular ring that applies a tightly tensioned helical stretch film envelope. Engineered for medium-duty industrial bundles, the FHOPE E400 series accommodates cross-sectional outer dimensions of 100–400 mm, lengths exceeding 1,200 mm, and payload capacities of 15–100 kg. System throughput is governed by dual frequency inverters controlling an orbital ring speed of 20–90 r/min and a synchronized conveyor velocity of 6–12 m/min.
During orbital packaging operations, bundled stock traverses the motorized roller beds into the rotating center of the structural ring frame. High-grade polyurethane dual friction wheels ensure vibration-dampened ring rotation, feeding pre-stretched wrapping media uniformly over the product perimeter. Downstream pneumatic clamping and automated cut-off devices operate via dedicated compressed air regulation to ensure clean cycle termination.
فهرست مندرجات
- عملیات گام به گام
- قطعات اصلی بسته بندی
- اپلیکیشنها
- مشخصات E400
- مثال کار شده: بسته لوله ۶ متری
- چک لیست انتخاب
- ایمنی: EN 415-10 و ISO 12100
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
عملیات گام به گام
- Infeed & Alignment. Bundles or individual tubes are transferred onto the powered infeed roller conveyor via crane, manual loading, or integrated upstream handling tables.
- Optical Detection. An industrial optical through-beam/diffuse photocell detects the leading bundle edge, triggering conveyor deceleration and initiating ring start at the programmed index point.
- Synchronized Orbital Wrapping. The ring accelerates smoothly around the linearly advancing bundle. The continuous pitch ratio between horizontal conveyor velocity and orbital rotational speed determines the film overlap, programmable via PLC HMI from 10% to 90%.
- Tail Cut & Clamp. At the trailing bundle edge, the ring completes reinforcing tail revolutions and returns to its home index position. The optional pneumatic cut-and-clamp unit severs the film and holds the leading tail for the next cycle without manual intervention.
- تخلیه خارج از تغذیه. The wrapped bundle transitions to the powered outfeed conveyor for subsequent inline steel/PET strapping, batch staging, or crane offloading.
قطعات اصلی بسته بندی
- Orbital Ring and Drive Transmission. Fabricated from precision-machined solid steel, the ring is driven by heavy-duty dual polyurethane friction drive wheels. The closed-loop mechanical transmission utilizes an inverter-controlled AC motor providing programmable S-curve acceleration/deceleration to eliminate mechanical shock.
- Film Delivery & Tension Carriage. Outfitted with a mechanical friction core brake, the carriage accepts stretch film, VCI anti-corrosion film, crepe paper, or woven PP tape. It accommodates rolls with 100–200 mm web width, 100–200 mm roll outer diameter, and standard 50 mm or 76 mm inner core diameters.
- Conveyor Handling Systems. The machine features standard 2,000 mm infeed and 2,000 mm outfeed motorized roller conveyors driven by independent helical gear motors with VFD synchronization. Roller tubes are encased in polyurethane sleeves or non-marking rubber to protect finished bundle surfaces. For workpieces exceeding 2,000 mm (such as 6 m stock), extended powered conveyors or modular idle roller extension benches must be integrated.
- Pneumatics and Control Architecture. Siemens or Delta PLC architecture paired with an industrial touchscreen interface. Monitors cycle timing, photoelectric positioning, safety interlocking, and system fault diagnostics.
- Civil & Foundation Requirements. Designed for installation directly onto a flat, non-cracking industrial reinforced concrete floor with a minimum bearing capacity of 10 kN/m² (1.0 t/m²).
اپلیکیشنها
| محصول | Primary Packaging Purpose | ملاحظات مهندسی بحرانی |
|---|---|---|
| لوله و تیوب فولادی | Atmospheric rust mitigation, rigid bundling | Linear mass per metre, structural stiffness |
| Solid bars and rods | Surface blemish protection, bundle cohesion | Small cross-section deflection, weight density |
| پروفیل های آلومینیومی | Anodized/powder-coated scratch protection | Non-marking soft roller sleeves, controlled clamping force |
| Plastic/PVC conduits | Dust exclusion, UV shielding, bundle stability | Elastic flexural deflection, low unit mass |
| Panels and flat extrusions | Edge impact protection, face encapsulation | Diagonal envelope matching annular ring opening |
مشخصات E400
| مورد | E400 Standard Parameter |
|---|---|
| Bundle Cross-Section (Envelope OD) | 100-400 میلی متر |
| Minimum Workpiece Length | ≥ 1,200 میلیمتر |
| Bundle Weight Range | 15–100 kg (standard conveyor build) |
| ابعاد نوار نقاله | 2,000 mm infeed + 2,000 mm outfeed (standard motorized) |
| Conveyor Linear Velocity | 6-12 متر بر دقیقه (قابل تنظیم با VFD) |
| سرعت چرخش حلقه مداری | 20–90 r/min (VFD adjustable) |
| محدوده همپوشانی فیلم | 10%–90% (programmable synchronization) |
| برق نصب شده | Approximately 2.5 kW, 380 V 3-Phase 50/60 Hz |
| الزامات تامین پنوماتیک | 0.4–0.6 MPa (filtered, dry plant air) |
| ارتقاء اتوماسیون | Automatic pneumatic film clamp and severing arm |
Note: For bundle profiles ranging from 200–600 mm and bundle loads up to 200 kg, the heavy-duty E600 series integrates pneumatic vertical press-down rollers and lateral guide rollers to stabilize stock during helical rotation.
مثال کار شده: بسته لوله ۶ متری
Consider a bundle of seven (7) cold-finished round steel tubes of dimensions Ø40 mm × 2 mm wall thickness, each 6,000 mm long, packed into a close-nested hexagonal bundle and wrapped using 150 mm film with a target 50% overlap.
| مرحله محاسبه | فرمول مهندسی و ورودی | خروجی کمی |
|---|---|---|
| Tube cross-sectional area | π/4 × (0.040² − 0.036²) | متر مربع 0.000239 |
| Linear weight per tube | 0.000239 m² × 7,850 kg/m³ | 1.87 کیلوگرم بر متر |
| Total weight per single tube | ۰.۲۰ کیلوگرم بر متر مربع × ۱۱.۳ متر مربع | کیلوگرم ۷۳۰۰ |
| Total 7-tube bundle weight | 7×11.22 کیلوگرم | ~ 78.5 کیلوگرم (within E400 15–100 kg rating) |
| Bundle envelope diameter | ۸۸ × Ø۳۰ میلیمتر | ۶۰ میلیمتر (within E400 100–400 mm opening) |
| Linear advance per turn (Pitch) | 150 mm × (1 − 0.50) | 75 میلی متر بر دور |
| Total orbital ring revolutions | 6,000 mm ÷ 75 mm/rev | 80 انقلاب |
| Max permissible conveyor speed | 90 r/min × 0.075 m/rev | 6.75 متر در دقیقه (within 6–12 m/min VFD range) |
| Total cycle wrapping duration | ۲.۰ متر ÷ ۲.۹ متر بر دقیقه | 0.89 min (~53 seconds) |
| Perimeter web length per turn | Outer perimeter approximation | 366 XNUMX میلی متر |
| Film consumed (nominal) | 80 revs × 0.37 m | ~ 29.6 متر (before mechanical pre-stretch) |
ارزیابی مهندسی: The bundle dimensions and mechanical loading fall cleanly within the continuous operating envelop of the E400, completing a single 6-metre cycle in roughly 53 seconds.
Kinematic Overlap Boundary Analysis:
Conveyor linear feed pitch is governed by:
Pitch = V_conveyor / N_ring
Overlap is governed by:
Overlap % = [1 - Pitch / W_film] × 100%
At the lower limit of continuous conveyor operation (6.0 m/min) combined with maximum orbital speed (90 r/min):
Pitch_min = 6,000 mm/min ÷ 90 r/min = 66.7 mm/rev
- With 150 mm film width, maximum continuous overlap is:
1 - (66.7 / 150) = 55.5%. - With 200 mm film width, maximum continuous overlap is:
1 - (66.7 / 200) = 66.7%.
To achieve extreme high-density wraps (>70%–90%) or localized reinforcement wraps at bundle ends, the system PLC executes a momentary conveyor crawl or dwell while the ring maintains rotation.
Weight Limit Verification: If the bundle were comprised of heavier Ø60 mm × 3 mm tubes (linear mass 4.22 kg/m per tube), the 7-tube bundle would reach approximately 177 kg. This exceeds the structural bearing limit of the standard E400 roller assembly; such duties require a reinforced conveyor frame and higher torque reducers, confirmed during application engineering.
چک لیست انتخاب
- Workpiece Dimensions: Minimum/maximum width, height, outer diameter envelope, and total cut length.
- Payload Loading: Mass per linear metre (kg/m) and gross single-bundle weight (kg).
- Consumable Media: Material substrate (PE stretch, VCI, PP woven), roll width, and target overlap ratio.
- Line Rate & Upstream Layout: Required bundles per hour, conveyor passline height, and inline vs. offline feeding interface.
- Cycle Automation Level: Manual trailing edge cut vs. fully automated pneumatic clamp, cut, and wipe.
- Auxiliary Site Utilities: Electrical supply specification (voltage, frequency) and compressed air availability.
ایمنی: EN 415-10 و ISO 12100
All FHOPE orbital wrappers are engineered in strict compliance with EN-415 10، (Safety of Packaging Machines: General requirements for pallet wrappers and orbital wrapping machines) and undergo comprehensive hazard mitigation under ISO 12100: 2010. The high-inertia rotating ring represents the primary operational hazard:
- Enclosed interlocked perimeter fencing or optical light curtains are integrated around the rotating assembly.
- Category 4 / PL e safety interlocks immediately arrest ring momentum via regenerative braking upon perimeter breach.
- Complete CE certification documentation, electrical schematics, and risk assessment files are provided per client installation.
سوالات متداول مهندسی
Q: Does the tube bundle rotate while moving through the machine? A: No. The bundle is carried longitudinally on a non-rotating linear path by the conveyor rollers while the wrapping ring orbits around it.
Q: How is the film overlap percentage regulated during high-speed runs? A: Overlap is controlled by the electronic synchronization ratio between the ring rotation motor (VFD) and the conveyor feed motor (VFD). Adjusting this frequency ratio on the HMI directly modulates the advance pitch per revolution.
Q: What is the primary throughput bottleneck for long linear bundles? A: Rotational ring speed (maximum 90 r/min). At higher overlap settings (e.g., 50% with 150 mm film), the maximum permissible conveyor feed rate is physically constrained to 6.75 m/min to maintain film layer continuity.
Q: Can the E400 wrap individual tubes rather than bundled packs? A: Yes, provided the tube outer diameter meets or exceeds 100 mm. For individual bars or small tubes under 100 mm OD, vertical pneumatic hold-down rollers or smaller frame variants (such as the E300) are required to prevent stock shifting.
مرحله بعدی
- Submit Project Parameters: Forward product cross-sections, bundle weights, and target throughput to
info@fhopepack.com. - بررسی طرح مهندسی: FHOPE packaging engineers simulate the envelope clearance, calculate cycle pitch, and size required conveyor extensions.
- Quotation Delivery: Receive a formal layout drawing, mechanical specification, and commercial quotation within 24 business hours.
خواندن مرتبط
- دستگاه استرچ لفاف افقی E400 (محصول)
- دستگاه بسته بندی استرچ اوربیتال
- دستگاه بسته بندی نوار اتوماتیک
- بسته بندی مواد میله آلومینیومی
- دستگاه بسته بندی اتوماتیک افقی اوربیتال برای لوله ها و بسته ها
منابع
- FHOPE Packaging Machinery Mechanical & Electrical Engineering Manual: E400/E600 Series
- EN 415-10: Safety of Packaging Machines – Wrapping Machines
- ISO 12100:2010: ایمنی ماشین آلات - اصول کلی طراحی - ارزیابی ریسک و کاهش ریسک
آخرین بهروزرسانی: 2026-10-29