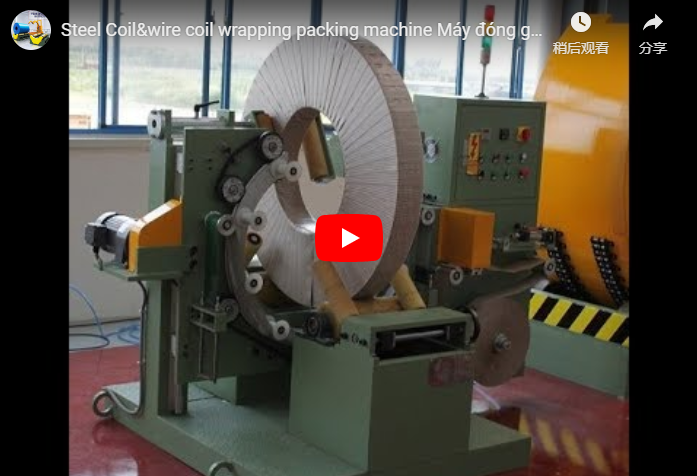
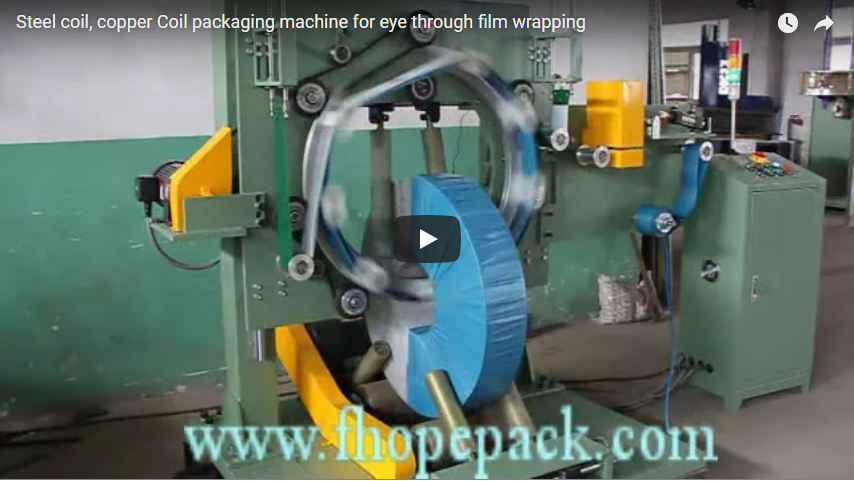
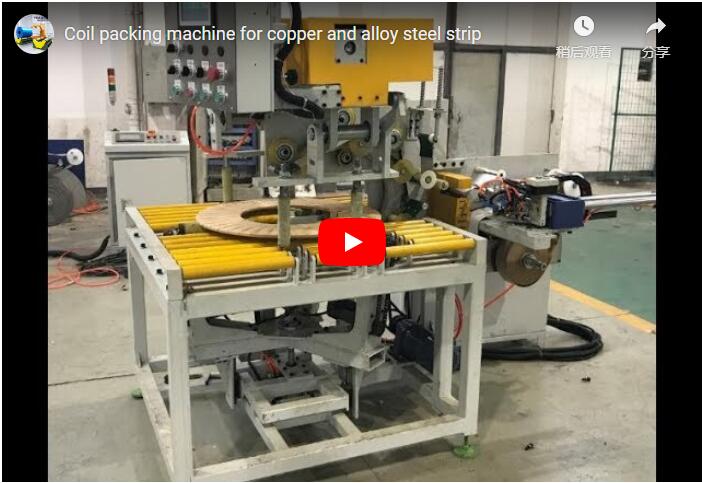
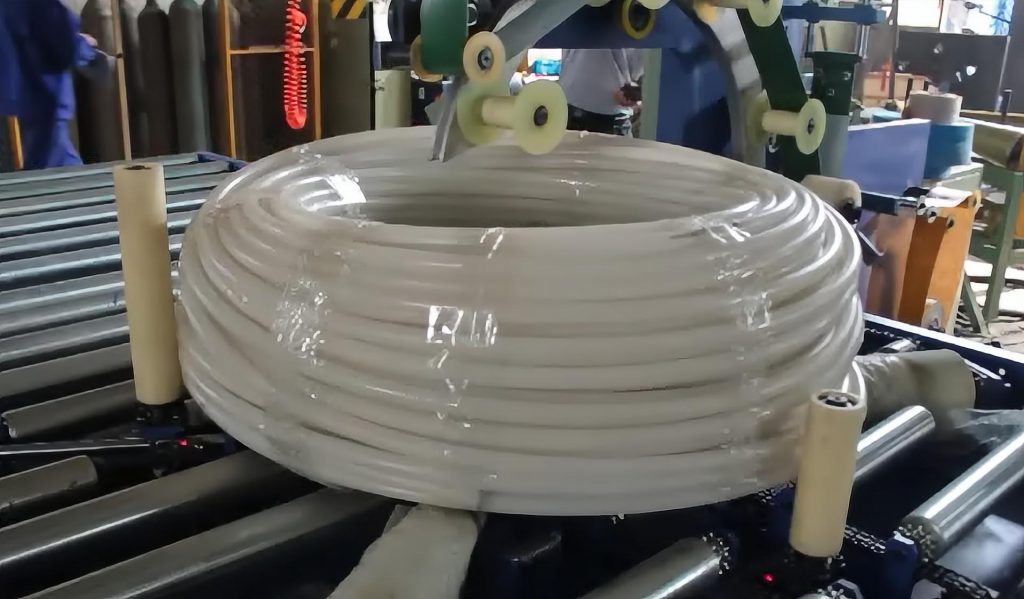
خلاصه اجرایی In this clip of about 50 s, slit coils pass a top-face head station, a gantry stacker builds them onto a pallet, and a second line shows an overhead-arm station run from its own HMI. We judge a line like this on four numbers you can measure yourself: seconds per coil at the slowest station, first-pass label reads, stack quality and film use per coil. Each one has a simple formula, shown below.
فهرست مندرجات
- آنچه کلیپ نشان میدهد
- KPI 1: seconds per coil at the slowest station
- KPI 2: first-pass label reads
- KPI 3: stack quality at the gantry stacker
- KPI 4: film use per coil
- Selection checklist for a coil labelling and stacking line
- کنترلها و ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
آنچه کلیپ نشان میدهد
The clip is about 50 s long and has three scenes. The times are read from the recording.
| زمان کلیپ | ایستگاه | چه اتفاقی می افتد |
|---|---|---|
| 0–18 ثانیه | Top-face head station | Coils lie eye-to-sky on a yellow roller table. Each one stops under an aluminium portal, and a yellow head lowers onto the top face. |
| 21–36 ثانیه | Gantry stacker | A blue gantry gripper picks the coils and lowers them in a stack onto a pallet on the outfeed conveyor. |
| 39–50 ثانیه | Overhead-arm station | On a second line with its own HMI column, an arm with a cable chain works over a coil on a green roller conveyor. |
Operators stand clear and watch. Coils move between stations on rollers or in the gripper.
The four KPIs below are how you check a line like this on your own floor.
KPI 1: seconds per coil at the slowest station
A coil line runs at the pace of its slowest station. Labelling, stacking and wrapping each have their own cycle; the longest one sets output.
Coils per hour = 3600 ÷ seconds per coil at the slowest station.
Measure each station separately with the line running real coils, not a demo. Then compare the result with your slitter output. If the slitter makes coils faster than the slowest packing station can take them, coils queue and the line operator starts making manual decisions.
On our proposals we list a cycle per station, so you can see which one is the limit. A buffer conveyor ahead of the slowest station absorbs short stops but does not raise average output.
KPI 2: first-pass label reads
A label is only useful if the warehouse scanner reads it the first time.
First-pass read rate = labels read at first scan ÷ labels applied.
Three things move this number:
- Label position. A fixed label head puts the label in the same place on every coil, so a scanner or forklift driver finds it.
- دادههای برچسبگذاری. Our coil lines can take coil data from ERP or MES, so the label matches the coil record without retyping.
- سطح The head needs a clean, flat area on the face. We place the labelling station where the coil face is still accessible, before film covers it, or we label the film, depending on your logistics.
Track rejected or re-printed labels per shift. A rising count points to position drift or a print-head issue long before customers complain.
KPI 3: stack quality at the gantry stacker
The gantry stacker in the clip builds a stack of coils on a pallet. Two checks tell you whether stacking is right.
- Centring error: how far each coil sits off the stack axis. An offset stack leans and loads one side of the pallet.
- Re-stack count: stacks an operator had to straighten or rebuild by hand, per shift.
Stacks per hour = coils per hour ÷ coils per stack.
Our coil line quote form allows stacks of up to 6 coils. Your working height comes from coil weight, coil width, the pallet and forklift capacity. We set it with you at layout stage.
KPI 4: film use per coil
Film is a running cost, so measure it per coil, not per month.
Film mass per coil (g) = film length used (m) × film width (mm) × thickness (µm) × density (g/cm³) ÷ 1000. Keep the units exactly as written and the factor of 1000 does the conversion.
Weigh a full film roll, wrap a known number of coils, weigh the roll again, and divide. Do this for each coil size you run. If film use per coil drifts up with no change in coil size, check the tension and overlap settings first.
Our coil line programs store tension and overlap per coil specification, so a size change does not depend on the operator re-tuning by hand.
Selection checklist for a coil labelling and stacking line
- Coil OD, ID, width and weight range, and the heaviest coil on the order.
- Label content, label position (face or film) and the data source: ERP, MES or manual.
- Strapping before stacking: PET or steel strap, and how many straps (see our slit coil strapping and wrapping line).
- Wrap material: stretch film, paper or woven, and the overlap you specify.
- Stack height, pallet type and forklift access to the outfeed.
- Final package direction: eye-to-sky or eye-to-wall.
- Target coils per hour from your slitter, and the station you expect to limit it.
کنترلها و ایمنی
استانداردهایی که اعمال میشوند به بازار مقصد بستگی دارند. برای بازارهای CE، استاندارد ISO 12100 روش ارزیابی ریسک را تعیین میکند و استاندارد EN 415-10 الزامات عمومی برای ماشینهای بستهبندی را پوشش میدهد که شامل حفاظ و ترتیب توقف اضطراری است.
The head stations, the gantry gripper and the overhead arm are the moving hazards. The stacker zone is fenced; label and film changes are done with the station stopped.
سوالات متداول مهندسی
Q: Which KPI should we track first on a new coil packing line? A: Seconds per coil at the slowest station. It sets coils per hour (3600 ÷ that time) and tells you where a buffer or a second machine would pay back.
Q: How do we measure first-pass label reads? A: Divide labels read at the first scan by labels applied, per shift. Re-prints and manual entries count as misses.
Q: Can labels be applied after wrapping? A: Yes. We either label the coil face before the film goes on or label the film itself. The choice depends on where your warehouse scans the coil.
Q: What should we inspect first if film use per coil goes up? A: If film use rises with no change in coil size, check the tension and overlap settings in the coil program first. Measure it by weighing the roll before and after a counted batch.
Q: How high can the gantry stack coils? A: Our quote form takes up to 6 coils per stack. The working height depends on coil weight, width, pallet and forklift.
مرحله بعدی
We size a coil strapping, labelling and stacking line in three steps:
- طرح چیدمان خود را ارسال کنید با قطر خارجی کویل، شناسه، عرض، وزن، محتوای برچسب و هدف خروجی، به info@fhopepack.com.
- دریافت پیشنهاد ظرف ۴۸ ساعت, with a cycle per station so you can see the limiting station.
- رزرو نظرسنجی در سایت بنابراین ما خروجی برشدهنده، جهت خط و دسترسی لیفتراک به پشتهها را تأیید میکنیم.
خواندن مرتبط
- خط بسته بندی اتوماتیک کویل نوار مسی با برچسب گذاری، بسته بندی و انباشت
- دستگاه بسته بندی کویل با قابلیت چسباندن و چاپگر برچسب بارکد
- خط بستهبندی کویل شکافدار برای مراکز خدمات
- خط بستهبندی کویل فولاد ضد زنگ: کج کردن، بستهبندی چشمی، برچسبگذاری و چیدمان
- خط بسته بندی کویل اتوماتیک
منابع
- توالی ایستگاهها و زمان کلیپها: ویدیو در یوتیوب (about 50 s; @Fhopepack)
- Line family, ERP/MES labelling, programs, stacking height on the quote form, strapping and wrap options: خط بسته بندی کویل اتوماتیک
- دامنه استانداردها: ISO 12100:2010؛ EN 415-10: 2014
- زمانبندی ارائه پیشنهاد: تایید طرح پیشنهادی (پیشنهاد ظرف ۴۸ ساعت)
آخرین بررسی: 2026-10-06