> **Resumen ejecutivo**
>
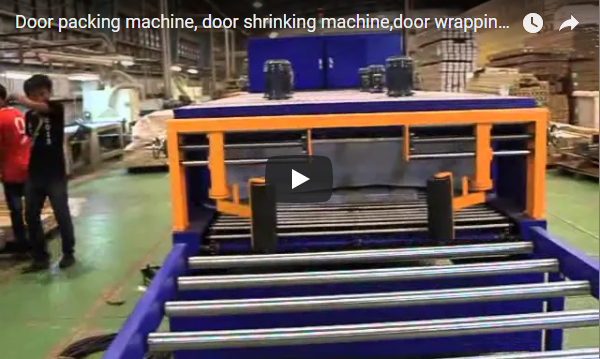
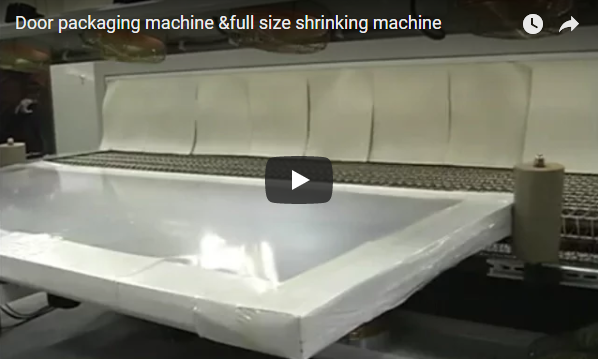
> A shrink packaging machine for carpet rolls closes each roll in PE film and shrinks it tight in a hot air tunnel. The line shown is a sealer with a film reel on top, a seal bar below and a tunnel with a curtain at the entry. Our equivalent solution is a sealing and shrinking line built on our door and panel sealer: PE film 40–100 micron, tunnel temperature 100–220 °C, conveyor up to 8 m/min. For a roll, the tunnel opening and film width are sized to the roll diameter, confirmed at quote.
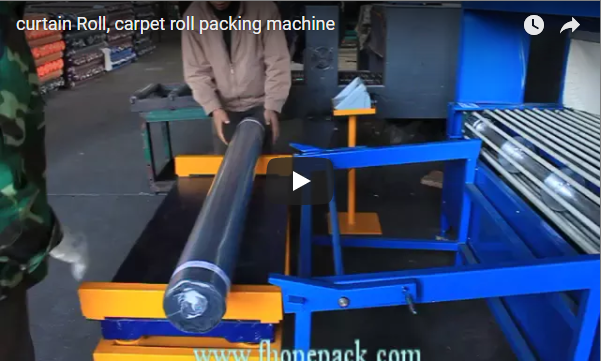
A blue carpet roll lies along the roller conveyor with its axis in the travel direction. Clear film runs down from the reel over the roll, the clamp arms press the film edges together underneath, and the seal bar closes the pack. The roll then rides into a closed tunnel and comes out with the film tight on its surface. The panel carries start, stop and a covered emergency stop button.
Índice
- Stations and what each one does
- Our equivalent solution: data
- Tunnel opening for a round roll
- Worked example: 2 m carpet rolls
- Choosing the film
- Pack defects and their causes
- Lista de verificación de selección
- Seguridad
- Preguntas frecuentes sobre ingeniería
- El próximo paso
- Lectura relacionada
- Fuentes
Stations and what each one does
| Station | Job | Setting that matters |
| :--- | :--- | :--- |
| Film reel and guide rollers | feed PE film over the roll | film tension, so the web stays flat |
| Clamp arms | bring the film edges together under the roll | clamp height to the roll diameter |
| Seal bar | weld and cut the film | blade temperature, kept constant by the controller |
| Shrink tunnel | hot air shrinks the film onto the roll | temperature and conveyor speed |
| Roller conveyor | carries the roll through every station | speed matched between sealer and tunnel |
**How the seams are made.** The film comes down over the roll from above, and the clamp arms bring both edges together under it, so the long seam runs along the roll axis on the underside. The seal bar then cuts and seals across the film at each end of the roll.
The end overhang shrinks onto the roll faces in the tunnel, giving a closed pack; on our door and panel line the edges are also pressed by rollers after shrinking so the film sticks tight.
The seal bar runs permanently heated with a temperature-controlled blade. A cold blade leaves a weak seam that opens in the tunnel; a hot one burns through thin film.
Our equivalent solution: data
The figures below come from our door and panel sealing and shrinking line. The same sealer and tunnel design handles rolls once the opening and film width are set for the roll. In service both sections run at one matched speed, set by the tunnel, so the sealing part's higher top speed is a reserve, not the line speed.
| Item | Sealing part | Shrinking part |
| :--- | :--- | :--- |
| Conveyor speed | about 0–12 m/min | about 0–8 m/min |
| Power | about 5.5 kW | about 30 kW |
| Tunnel size (panel version) | — | L 2,500 × W 1,500 × H 300 mm |
| Temperature | constant-temperature seal bar | 100–220 °C |
| Film | PE, 40–100 micron (30–150 micron possible) | same |
| Working table height | about 800 mm | — |
| Compressed air | 6–8 kgf/cm² | — |
| Power supply | 380 V, 50 Hz, 3 phase | 380 V, 50 Hz, 3 phase |
| Control | PLC | temperature controller with display |
Maximum roll diameter, roll length, roll weight on the rollers and air consumption for a carpet line are confirmed at quote.
Tunnel opening for a round roll
The panel version of the tunnel is 300 mm high, made for flat loads up to 200 mm thick. A roll needs room above it for the hot air to reach the top of the film.
**Rule.** Tunnel clear height ≥ roll diameter + air gap. With an illustrative 100 mm gap, a 350 mm roll needs at least 350 + 100 = 450 mm, so it cannot use the 300 mm panel opening. We build the tunnel opening and the sealer clamp stroke to suit the largest roll.
Worked example: 2 m carpet rolls
Take carpet rolls 350 mm in diameter and 2,000 mm long, about 40 kg each. These are illustrative customer figures.
| Check | Calculation | Result |
| :--- | :--- | :--- |
| Pitch on the conveyor, 500 mm gap | 2,000 + 500 | 2,500 mm |
| Rolls per minute at 6 m/min | 6 ÷ 2.5 | 2.4 |
| Rolls per hour, conveyor limit | 2.4 × 60 | 144 |
| Time any point of the film spends in the 2,500 mm tunnel | 2.5 ÷ 6 × 60 | 25 s |
| Installed power | 5.5 + 30 | 35.5 kW |
**Result.** At 6 m/min the conveyor allows 144 rolls an hour, but the seal cycle, not the conveyor, usually sets the real rate. If the seal cycle is 30 s per roll, an illustrative figure, the line packs 3,600 ÷ 30 = 120 rolls an hour. Slow the conveyor if the film is not tight at the exit; a longer dwell gives more shrink.
Choosing the film
| Roll weight | Film thickness to start with |
| :--- | :--- |
| light rolls, short runs | 40–60 micron |
| heavier rolls, rough handling | 80–100 micron |
| special cases | 30–150 micron available |
The film width must cover the roll and leave a seal flange. For a 350 mm roll the circumference is π × 350 ≈ 1,100 mm; add a 50 mm flange on each side and the film needs 1,100 + 2 × 50 = 1,200 mm in total across the webs.
This width covers the circumference only. Add the end overhang for the roll faces, about half the diameter at each end for a fully closed pack, so 2,000 + 350 = 2,350 mm of film length per roll in the example. Final film width and length are confirmed at quote.
Pack defects and their causes
| Defect | Likely cause | Fix |
| :--- | :--- | :--- |
| Loose film, wrinkles | too little heat or too short a dwell | raise temperature or slow the conveyor |
| Holes or burn-through | too much heat for the film | lower temperature or use thicker film |
| Seam opens in the tunnel | seal bar too cold or dirty | check blade temperature and clean it |
| Air bubbles under the film | trapped air with no escape | add small vent holes in the film |
| Film too tight at roll ends | too much film overhang | reduce overhang so ends shrink evenly |
Lista de verificación de selección
1. Roll diameter, smallest and largest.
2. Roll length range.
3. Roll weight.
4. Rolls per hour.
5. Film type and thickness in use now, if any.
6. Power supply and compressed air at site.
Seguridad
We design to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machinery and EN 60204-1 for the electrical equipment. The hot seal bar, the clamp arms and the hot tunnel are the main hazards. Guards or fences at the clamp area, a covered emergency stop and warning labels on hot surfaces are agreed per project, together with the CE documents.
Preguntas frecuentes sobre ingeniería
Q: Can the same line pack panels and carpet rolls?
A: Yes, if the tunnel opening and clamp stroke cover both. The settings change per product.
Q: How hot does the tunnel run?
A: Between 100 and 220 °C, set to the film thickness and conveyor speed.
P: ¿Qué fuente de alimentación se necesita?
A: 380 V, 50 Hz, 3 phase; other voltages are confirmed at quote.
Q: How many rolls an hour?
A: It depends on roll length and seal cycle; the worked example shows how to estimate it.
Q: Does the line need an operator?
A: One operator loads rolls and watches the pack quality; automatic loading is confirmed at quote.
El próximo paso
1. **Send your roll diameter, length, weight and rolls per hour** to info@fhopepack.com.
2. **We size** the tunnel opening, film width and conveyor speed.
3. **Respondemos en un plazo de 24 horas** con una propuesta y un presupuesto.
Lectura relacionada
- [Carpet roll sealing and shrinking packing machine](https://www.fhopepack.com/videos/carpet-roll-sealing-and-shrinking-packing-machine/)
- [Shrink packaging machine for carpet and curtain rolls](https://www.fhopepack.com/videos/shrink-packaging-machine-for-carpet-curtain-rolls/)
- [Automatic roll packing machine and carpet packing machine](https://www.fhopepack.com/videos/automatic-roll-packing-machine-and-carpet-packing-machine/)
- [Carpet roll shrinking machine](https://www.fhopepack.com/videos/carpet-roll-shrinking-machine/)
- [Fully enclosed rolled carpet shrink packaging](https://www.fhopepack.com/videos/eliminate-transport-damage-fully-enclosed-rolled-carpet-shrink-packaging-systems/)
- [Automatic panel sealing and shrinking machine](https://www.fhopepack.com/videos/automatic-panel-sealing-and-shrinking-machine/)
- [Automatic door shrinking machine (product)](https://www.fhopepack.com/Automatic_door_shrinking_machine.html)
Fuentes
- FHOPE quotation: automatic door panel sealing and shrinking machine, 2021-09-15 (sealing part and shrinking part data)
- EN ISO 12100:2010; EN 415-10; EN 60204-1
- The carpet roll sealing and shrinking line shown above
Última revisión: 19/10/2026