> **Resumen ejecutivo**
> Our slit coil packing line takes narrow coils from the slitter and straps, wraps, weighs, labels and stacks them onto pallets. In narrow-strip setups it packs **25–40 coils per hour**, for coils up to 4,000 kg and 500 mm wide. The line has to keep up with the slitter, so we size it from the strips per mother coil and the slitter cycle. Strapping time per coil usually sets the pace.
Índice
- Estaciones de línea
- Especificaciones
- A juego con la rebanadora
- Tiempo de abrocharse
- Envoltura
- Apilado
- Niveles de automatización
- Controles y servicios públicos
- Seguridad
- Lista de verificación de implementación
- Preguntas frecuentes sobre ingeniería
- El próximo paso
- Lectura relacionada
- Fuentes
Estaciones en una línea de empaquetado de bobinas cortadas
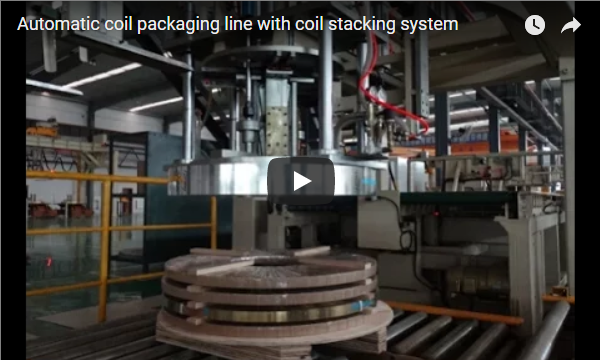
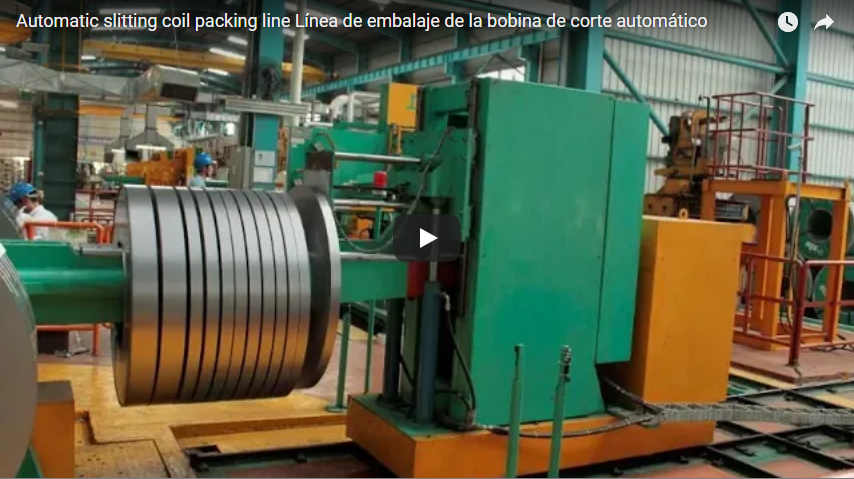
Construimos la línea que se muestra en este video para un centro de servicio de corte longitudinal. Cada bobina estrecha pasa por estas estaciones, mirando hacia el cielo:
1. **Down-ending.** Coils leave the slitter turnstile eye to wall. A down-ender tilts each coil to eye to sky and puts it on the conveyor.
2. **Centring.** A centring station with sensors and a lifting table aligns the coil with the conveyor centre line. A centred coil straps evenly and stacks straight.
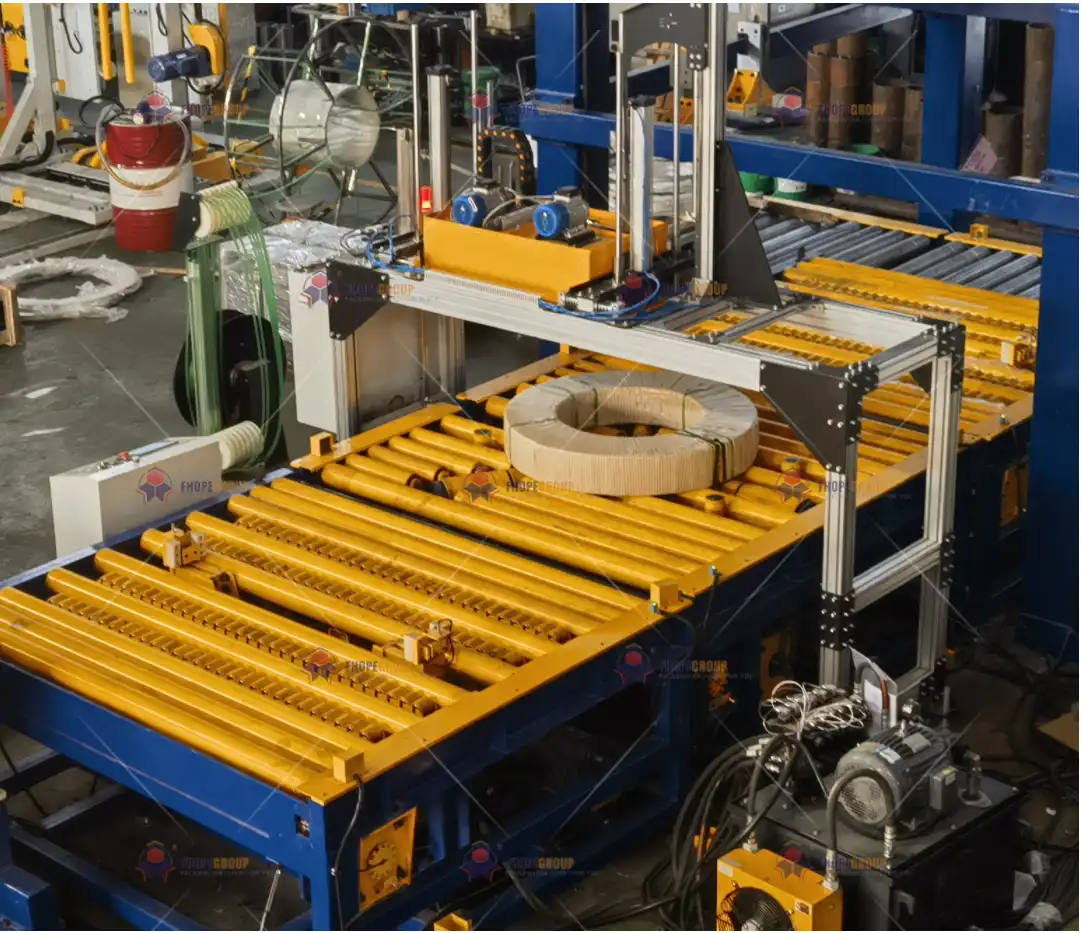
3. **Strapping.** A strapping unit on a rotating platform puts PET or steel straps through the coil eye, at 3, 4 or 6 points.
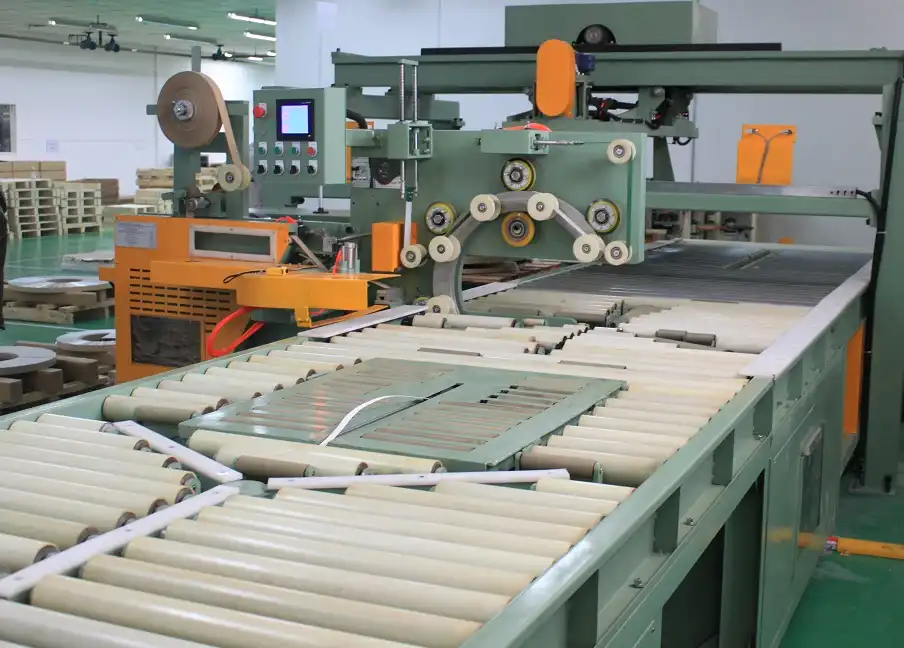
4. **Wrapping.** An orbital wrapper passes paper or stretch film through the eye for full coverage.
5. **Coil weighing and labelling.** An inline scale records each coil's net and gross weight, and the line applies a barcode label for tracking.
6. **Stacking.** A stacker picks the packed coils and stacks them onto a wooden pallet. Timber separators between layers stop the stack shifting in transit.
Tras el embalaje, las cintas transportadoras motorizadas llevan las bobinas a la estación de apilamiento. En esta línea, el brazo apilador gira sobre un gran anillo giratorio para colocar cada bobina en la pila de palés.
Especificaciones de la línea de empaquetado de bobinas ranuradas
| Parameter | Narrow slit coil line |
|---|---|
| Packing capacity | 25–40 coils per hour |
| Coil weight | up to 4,000 kg |
| Coil width | up to 500 mm |
| Coil OD | up to 1,500 mm, customizable to 2,100 mm |
| Coil ID | 508 mm or 610 mm |
| Strapping | PET or steel, 2,000–22,000 N tension |
| Wrapping overlap | 10–90% |
Las bobinas anchas, de 450 a 1,900 mm de ancho, se procesan en una línea más robusta a una velocidad de 5 a 8 bobinas por hora. La precisión de apilamiento en un apilador de pórtico es de ±2 mm.
Adaptar la línea de empaquetado a la cortadora
Una cortadora transforma una bobina madre en muchas bobinas estrechas a la vez. La línea de empaquetado debe retirarlas antes de que llegue la siguiente bobina madre.
- **Time per coil** = 3600 ÷ coils per hour. At 40 coils per hour, the line has 90 s per coil.
- **Time per mother coil** = number of strips × time per coil. With an illustrative 20 strips, packing takes 20 × 90 s = 30 min.
- **Check:** if the slitter needs less than that per mother coil, coils queue on the turnstile. Then we add a buffer, a second strapping head or a faster stacker.
Realizamos esta comprobación del número de tiras y del ciclo de la bobina madre antes de corregir el diseño.
Tiempo de flejado por bobina
El flejado suele ser la estación más lenta, por lo que la revisamos primero. Cada fleje tarda entre 15 y 35 segundos en nuestros cabezales automáticos de PET o acero:
1. **4 straps at 15 s** = 60 s, which fits inside the 90 s budget at 40 coils per hour.
2. **4 straps at 35 s** = 140 s, which limits the line to about 25 coils per hour.
3. **6 straps** on heavy coils take longer again, so heavy coils run at the lower end of the range.
El indexado de la plataforma giratoria y la transferencia mediante cinta transportadora añaden tiempo a los ciclos de transporte. Medimos estos tiempos para su diseño y los incluimos en la verificación del ciclo.
La tensión de la correa se ajusta en la interfaz hombre-máquina (HMI) entre 2,000 N y 22 000 N. Este rango abarca tanto correas de PET como de acero, y se configura según el material de la correa y la bobina. Las correas estrechas y delgadas requieren una tensión menor para evitar que la correa dañe el borde de la bobina.
Envoltura transparente para bobinas ranuradas
La envolvedora orbital pasa papel o film estirable a través del ojo de la bobina mientras esta gira. El PLC ajusta la superposición entre el 10 % y el 90 %. La elección del material depende del envío.
- **Stretch film** for dust and moisture protection in storage.
- **VCI paper** for steel coils that need rust protection at sea.
- **Woven fabric** for a tougher outer layer.
Apilado de bobinas cortadas sobre paletas
La apiladora recoge las bobinas empaquetadas mediante electroimán o vacío y las coloca verticalmente sobre palés de madera. El diámetro exterior y el ancho de la bobina determinan cuántas bobinas caben por palé y la altura de la pila. Los separadores de madera entre las capas mantienen estable la pila.
Los palets terminados salen mediante cintas transportadoras motorizadas hacia la zona de expedición. En las líneas totalmente automatizadas, el palet terminado también se envuelve, pesa y etiqueta por separado de las etiquetas de las bobinas.
Niveles de automatización para centros de servicio de corte longitudinal
Construimos la línea en tres niveles:
| Level | Main equipment |
|---|---|
| Basic compact line | Coiler trolley, 90° tilting down-ender, turntable for semi-auto strapping, jog crane or magnetic stacker |
| Standard automated line | Turnstile pick-up and lifter, inline weighing, automatic or semi-automatic bundling, trolley lifter |
| Fully automated line | Coil car and down-ender, automatic strapping, eye-through wrapping, gantry stacking, pallet wrapping, weighing and labelling |
La línea totalmente automatizada clasifica las bobinas por ancho, diámetro exterior y lógica de apilamiento según el programa. La línea básica reemplaza la manipulación con grúa y gancho por máquinas controladas.
Controles y servicios públicos
La línea funciona con un PLC Siemens S7-1200 o S7-1500F con HMI. La serie F es un PLC a prueba de fallos. Planifique los siguientes servicios en la planta:
- **Power:** 380–480 V, 50/60 Hz, 3 phase.
- **Air:** 5–8 bar for the pneumatic units.
Seguridad en una línea de empaquetado de bobinas cortadas
El movimiento de las bobinas, la apiladora y los cabezales de flejado representan los principales riesgos. Instalamos vallas en las zonas automáticas y colocamos barreras fotoeléctricas y enclavamientos de seguridad en las estaciones de apilamiento y flejado, de modo que la apiladora y los cabezales se detienen cuando entra un operario.
Las normas aplicables dependen del mercado de destino. Para los mercados CE, la norma ISO 12100 establece el método de evaluación de riesgos y la norma EN 415-10 establece los requisitos generales para las máquinas de envasado.
Lista de verificación para la implementación de una línea de empaquetado de bobinas cortadas
- [ ] Coil width, OD, ID and weight range, narrow and wide.
- [ ] Strips per mother coil and slitter cycle time.
- [ ] Number of straps per coil and strap type, PET or steel.
- [ ] Wrapping material: film, VCI paper or woven fabric.
- [ ] Pallet size, stack height and separator use.
- [ ] Weighing, labelling and ERP connection needs.
Preguntas frecuentes sobre ingeniería
Q: How many slit coils per hour can the line pack?
A: 25–40 coils per hour on narrow-strip lines, and 5–8 coils per hour on wide-coil lines. The strapping time per coil usually sets the exact rate.
Q: How many straps does a slit coil need?
A: The program allows 3, 4 or 6 eye-through straps. At 15–35 s per strap, 4 straps take 60–140 s, so heavy coils with 6 straps run slower.
Q: Can the line handle 610 mm ID coils?
A: Yes. The line takes 508 mm and 610 mm ID coils, with OD up to 1,500 mm or 2,100 mm on request.
Q: How do I know the line keeps up with my slitter?
A: Multiply strips per mother coil by seconds per coil. At 40 coils per hour, 20 strips take 30 min, which must be shorter than the slitter cycle.
Q: Which PLC does the line use?
A: Siemens S7-1200 or S7-1500F with HMI. The fail-safe F-series handles the safety functions on fully automated lines.
El próximo paso
Adaptamos la línea de empaquetado de bobinas cortadas a su cortadora en tres pasos:
1. **Submit your layout drawing** with coil sizes, weights, strips per mother coil and slitter cycle to **info@fhopepack.com**.
2. **Receive a line proposal within 48 hours**, with the station list, strapping time check and layout.
3. **Book a site survey** to fit the line between your slitter and warehouse.
Lectura relacionada
- [Automatic coil packing line overview](https://www.fhopepack.com/Automatic-Coil-Packing-Line/)
- [Automatic packing line systems](https://www.fhopepack.com/Automatic-Packing-Line/)
- [Coil packing machine details](https://www.fhopepack.com/Coil_packing_machine.html)
- [Slitting coil packaging line](https://www.fhopepack.com/Show-Room/steel/slitting-coil-packaging-line.html)
- [Video: slit coil packaging line for slitting service center with automatic labeling](https://www.fhopepack.com/videos/slit-coil-packaging-line-for-slitting-service-center-with-automatic-labeling-system-connect-to-erp/)
Fuentes
- Narrow-line specifications, automation levels, controls, utilities, safety: [slitting coil packaging line page](https://www.fhopepack.com/Show-Room/steel/slitting-coil-packaging-line.html)
- Stations, wide-coil range, strap points, wrapping materials, stacking: [slit coil handling and packaging line page](https://www.fhopepack.com/Automatic-Coil-Packing-Line/slit-coil-packing.html)
- Line in action: [our slit coil packing line video on YouTube](https://www.youtube.com/watch?v=bhIOkdPatUw)
- Alcance de las normas: [ISO 12100:2010](https://www.iso.org/standard/51528.html), [EN 415-10:2014](https://www.nen.nl/en/nen-en-415-10-2014-en-191845)
Última revisión: 03/10/2026