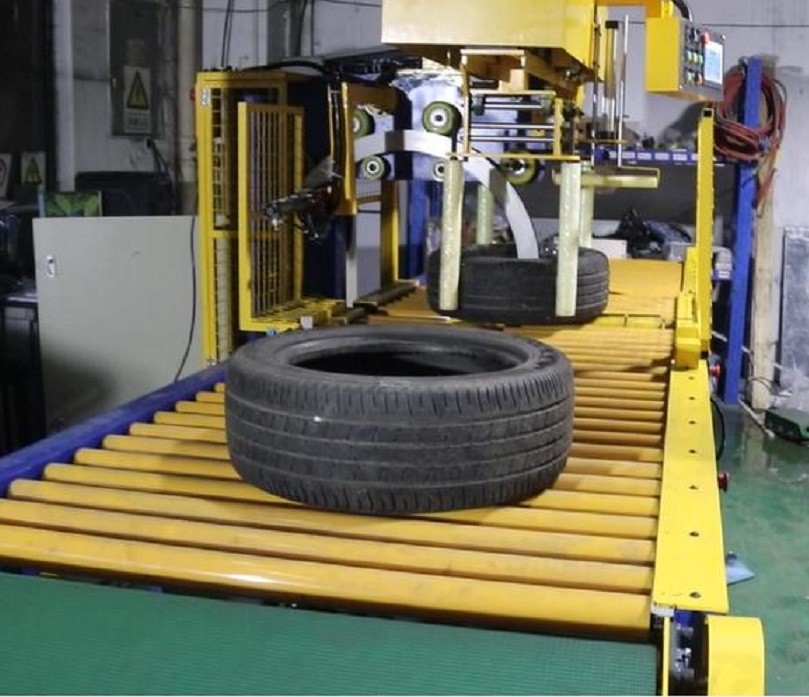
> **Executive summary**
>
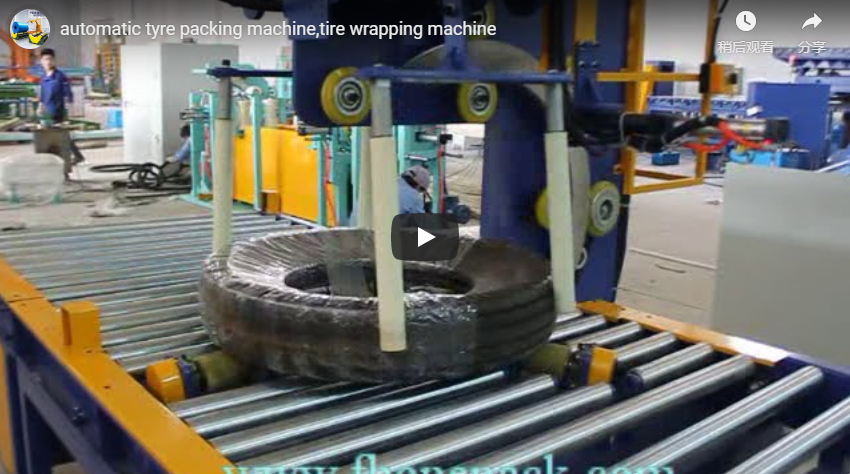
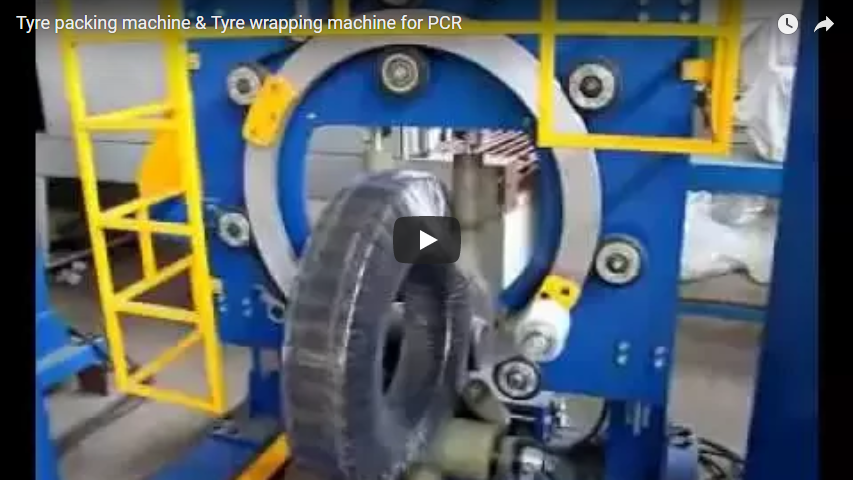
> Designed for single-piece passenger car radial (PCR) and motorcycle tyres, our vertical orbital wrapping machine secures the tyre upright on twin polyurethane-coated drive rollers and applies stretch film, PE woven tape, or protective paper through the bead and across the tread. The C-type open-ring architecture allows fast top loading and vertical unloading without manual threading. An integrated pneumatic stabilization arm suppresses tyre runout and vibration on lightweight casings. Operating at ring rotation speeds up to 120 r/min, the FPT-200 completes a full protective wrapping cycle within 18–30 seconds for tyre outer diameters between 510 mm and 800 mm.
<iframe width="940" height="535" src="https://www.youtube.com/embed/pOD1YeOfgBU" frameborder="0" allow="accelerometer; autoplay; clipboard-write; encrypted-media; gyroscope; picture-in-picture; web-share" referrerpolicy="strict-origin-when-cross-origin" allowfullscreen></iframe>

---

<h2 id="table-of-contents">Table of Contents</h2>

<ul>
<li><a href="#why">Why tyres are wrapped</a></li>
<li><a href="#new">What is new in the design</a></li>
<li><a href="#cycle">The wrapping cycle</a></li>
<li><a href="#specs">FPT-200 and FPT-300 data</a></li>
<li><a href="#example">Worked example: a 225/45R17 tyre</a></li>
<li><a href="#selection-checklist">Selection checklist</a></li>
<li><a href="#safety">Safety: EN 415-10 and ISO 12100</a></li>
<li><a href="#engineering-faq">Engineering FAQ</a></li>
<li><a href="#next-step">Next step</a></li>
<li><a href="#related-reading">Related reading</a></li>
<li><a href="#sources">Sources</a></li>
</ul>

<h2 id="why">Why tyres are wrapped</h2>

High-value replacement tyres, racing slicks, and export shipments require robust surface protection during transit and warehousing. Unprotected tyres accumulate atmospheric dust, suffer bead abrasion during handling, and degrade from prolonged exposure to UV radiation and ozone.

For tyres sold individually to retail distributors, pristine presentation and visible branding are paramount. Manual wrapping requires an operator to pass a packaging roll through the inner bead dozens of times per tyre—an ergonomic hazard that caps throughput at 6 to 10 units per hour while yielding inconsistent tension. Mechanized through-the-eye wrapping encapsulates the bead, sidewall, and tread under controlled tension in under 30 seconds, delivering consistent overlap, moisture defense, and branded presentation.

<h2 id="new">What is new in the design</h2>

- **Top-loading C-frame ring:** The orbital rotating ring features an open C-profile cut-out. Upon cycle completion, the ring automatically halts with the opening oriented upward, enabling operators or overhead hoists to drop tyres in and hoist them out directly from above.
- **Dynamic runout stabilization:** Lightweight motorcycle and low-profile car tyres tend to skip or wobble on bottom rollers under wrapping tension. A top-mounted pneumatic press arm with an adjustable idler roller stabilizes the tyre casing vertically and laterally during high-speed rotation.
- **Synchronous branding tape applicator:** An auxiliary dispenser applies custom-printed corporate logo tape around the outer circumference (tread area) simultaneously with the transparent outer protective film.
- **Absolute home-position indexing:** High-precision proximity sensors and dynamic inverter braking ensure the shuttle ring consistently returns to its exact top-dead-center home position after each cycle.
- **Dual-inverter speed ramps:** Independent variable-frequency drives (VFD) govern both ring rotation and cradle roller drive speeds, allowing programmable acceleration and deceleration curves that prevent film breakage at startup.

<h2 id="cycle">The wrapping cycle</h2>

1. **Loading:** With the ring indexed at the open top-dead-center position, the operator drops the tyre vertically onto the polyurethane drive rollers.
2. **Stabilization:** The pneumatic hold-down arm descends, pressing the upper idler roller against the tyre crown at a pre-set pressure (0.2–0.4 MPa).
3. **Orbital wrapping:** The C-ring rotates orbital-fashion through the tyre eye, while the synchronized drive rollers rotate the tyre around its horizontal center axis, generating an even helical wrap.
4. **Cycle completion & indexing:** Upon completing 360° circumferential coverage plus a programmable tail overlap, the ring slows down and locks at the home position.
5. **Ejection:** The stabilization arm retracts, the film tail is severed, and the finished tyre is lifted vertically from the station.

The machine supports both semi-automatic push-button sequencing and fully automated integration. System diagnostics and cycle alarms are displayed in real time on the HMI touchscreen.

<h2 id="specs">FPT-200 and FPT-300 data</h2>

| Parameter | FPT-200 | FPT-300 |
| :--- | :--- | :--- |
| Tyre Inner Diameter (ID) | 300–700 mm | 500–900 mm |
| Tyre Outer Diameter (OD) | 510–800 mm | 800–1,200 mm |
| Tyre Width (Cross-Section) | 40–250 mm | 80–300 mm |
| Tyre Unit Weight | 10–30 kg | 10–100 kg |
| Ring Rotation Speed | 0–120 r/min (VFD controlled) | 30–110 r/min (VFD controlled) |
| Cycle Time per Tyre | 18–30 s | 25–40 s |
| Film Overlap Ratio | 10%–80% (Continuously adjustable) | 20%–80% (Continuously adjustable) |
| Total Drive Power | 1.5 kW | 2.0 kW |
| Operating Voltage | 380 V, 50 Hz, 3-Phase (or to order) | 380 V, 50 Hz, 3-Phase (or to order) |
| Compatible Materials | PE, stretch film, PP tape, paper, knit belt | PE, stretch film, PP tape, paper, knit belt |

Film tension is mechanically modulated via an adjustable spring-loaded friction brake on the material carriage spool.

<h2 id="example">Worked example: a 225/45R17 tyre</h2>

The following validation calculates the packaging parameters for a standard passenger car tyre (225/45R17), wrapped with 100 mm wide film at a 50% target overlap ratio.

| Engineering Parameter | Formula / Calculation | Value |
| :--- | :--- | :--- |
| Inner Bead Diameter (ID) | 17 in × 25.4 mm/in | 431.8 mm (≈ 432 mm) |
| Outer Tyre Diameter (OD) | 431.8 mm + 2 × (0.45 × 225 mm) | 634.3 mm (≈ 634 mm) |
| Sidewall Section Height (H) | (634 mm − 432 mm) ÷ 2 | 101 mm |
| Cross-Section Width (W) | Nominal section width | 225 mm |
| Dimensional Feasibility | ID 432 mm ≥ 300 mm; OD 634 mm ≤ 800 mm | Passes FPT-200 Envelope |
| Effective Feed Advance per Wrap | Film Width × (1 − Overlap Ratio) = 100 mm × (1 − 0.50) | 50 mm / revolution |
| Ring Rotations per Tyre | (π × OD) ÷ Advance = (3.1416 × 634 mm) ÷ 50 mm | ≈ 39.8 wraps (use 40) |
| Theoretical Ring Run Time | (40 wraps ÷ 120 r/min) × 60 s/min | 20.0 s |
| Envelope Path per Ring Wrap | 2 × (Section Width + Sidewall Height) = 2 × (225 + 101) mm | ≈ 0.652 m |
| Film Consumption per Tyre | 40 wraps × 0.652 m | ≈ 26.1 m |

**Engineering evaluation:**
The 225/45R17 tyre fits securely within the FPT-200 operating range. At full rated ring speed (120 r/min), completing 40 orbital revolutions requires 20 seconds of pure wrapping time, fitting comfortably inside the 18–30 second station cycle.

If the process requires higher moisture sealing via a 70% overlap ratio, the advance rate drops to 30 mm per wrap, requiring 67 ring revolutions. At 120 r/min, this increases active wrapping time to approximately 33.5 seconds. For high-overlap configurations without cycle-time penalties, engineers should specify 120–150 mm material widths.

<h2 id="selection-checklist">Selection checklist</h2>

1. **Tyre envelope dimensions:** Specify minimum and maximum ID, OD, cross-section width, and unit weight (passenger car, commercial light truck, or motorcycle).
2. **Packaging media:** Define roll width, core diameter, and material substrate (LLDPE stretch film, HDPE woven ribbon, neutral crepe paper, or co-extruded logo tape).
3. **Throughput targets:** Target cycle time per unit and shifts per day to verify thermal motor duty cycle.
4. **Loading methodology:** Standalone manual vertical loading via counterbalanced crane or seamless integration with automated infeed/outfeed gravity roller conveyors.
5. **Electrical utility:** Local grid supply voltage, frequency, and safety interlocking tier.

<h2 id="safety">Safety: EN 415-10 and ISO 12100</h2>

All FHOPE orbital tyre wrappers are engineered in strict compliance with **EN 415-10** (Safety of packaging machines: wrapping machines) and risk-assessed per **ISO 12100:2010**.

The primary mechanical hazard zones—the rotating open C-ring and the lower friction drive rollers—are enclosed behind interlocked steel mesh perimeter guards. When top manual loading is utilized, the loading aperture is protected by an integrated Type 4 optical safety light curtain or an electrically interlocked dual-channel safety gate.

If the light curtain is interrupted during operation, an emergency category 0 stop is executed via safe torque off (STO) inverter control. The machine prevents initiation of ring rotation unless the stabilization arm pressure switch confirms the tyre is seated and the operator is outside the hazard perimeter. CE technical documentation and declaration of conformity are provided with each machine.

<h2 id="engineering-faq">Engineering FAQ</h2>

**Q: Can the machine handle narrow motorcycle tyres without tipping?**
A: Yes. The pneumatic stabilization arm utilizes a deep-grooved polyurethane guide roller that secures the tread from the top, mechanically eliminating lateral tipping and axial runout on narrow casings (down to 40 mm width).

**Q: Can we apply continuous branding along the tread perimeter?**
A: Yes. An optional synchronized logo tape dispenser mounts adjacent to the orbital ring, applying pre-printed branded tape directly to the tyre tread circumference while the primary ring wraps the carcass.

**Q: What determines whether an application requires the FPT-200 or FPT-300?**
A: Tyre outer diameter and cross-section weight are the primary criteria. Tyres with an OD up to 800 mm and weight under 30 kg use the FPT-200. Heavy truck, agricultural, or large SUV tyres up to 1,200 mm OD and 100 kg require the heavy-duty chassis and wider roller base of the FPT-300.

**Q: Which harmonized standards govern machine validation?**
A: Machinery Directive compliance is validated against EN 415-10 for orbital wrapping mechanics, EN ISO 13849-1 for safety-related parts of control systems, and ISO 12100 for general hazard mitigation.

<h2 id="next-step">Next step</h2>

1. **Submit your tyre matrix:** Send your dimensional range (min/max ID, OD, section width, weight) and throughput target to **info@fhopepack.com**.
2. **Engineering verification:** Our application team confirms model sizing (FPT-200 vs. FPT-300), overlap ratios, and stabilization tooling.
3. **Formal proposal:** Receive a detailed technical layout, cycle analysis, and quotation within 24 hours.

<h2 id="related-reading">Related reading</h2>

- [Top-loading tyre packing machine, FPT-200 data (product)](https://www.fhopepack.com/Tyre-packing-machine/Tyre-Packing-Machine-FPT-100.html)
- [Tyre packing machine, FPT-300 data (product)](https://www.fhopepack.com/Tyre-packing-machine/Tyre-Packing-Machine-FPT-200.html)
- [Tyre wrapping machine for PCR tyres](https://www.fhopepack.com/videos/tyre-packing-machine-tyre-wrapping-machine-for-pcr/)
- [Online automatic multiple tyres strapping machine](https://www.fhopepack.com/videos/online-automatic-multiple-tires-strapping-machine/)
- [Automatic horizontal tyre stretch wrapper (product)](https://www.fhopepack.com/Tyre-packing-machine/tyre-wrapper.html)

<h2 id="sources">Sources</h2>

- FHOPE technical product specifications: FPT-200 and FPT-300 orbital tyre wrapping series
- Direct engineering validation data from factory test bench video reference
- Tyre geometry standards: ISO 4000-1 (Passenger car tyres and rims)
- International safety standards: EN 415-10:2014; ISO 12100:2010; EN ISO 13849-1:2015

<p><strong>Last reviewed:</strong> 2026-10-19</p>