Резюме An automatic strapping machine takes stacked loads straight from the conveyor, closes a strap around each bundle and releases it without manual handling. The clip shows that cycle running on brick stacks; our equivalent strapping solution is configured per project. Configuration choices, safety references and the quoting steps follow.
Съдържание
- Какво показва видеото
- Къде е подходяща тази машина
- How the strapping cycle runs
- Configured per project
- Selection checklist for a strapping station
- Контроли и безопасност
- Често задавани въпроси за инженерство
- Следваща стъпка
- Свързано четене
- Източници
Какво показва видеото
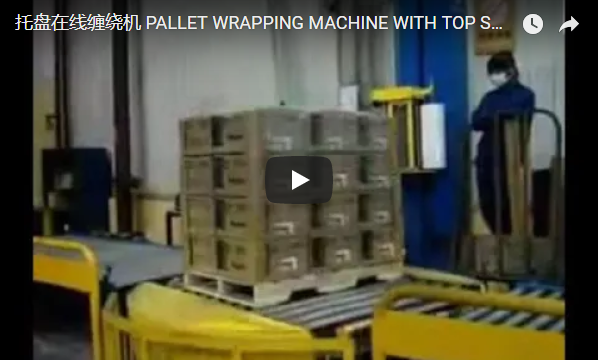
The clip is a single continuous shot: the camera stays with the machine while it works through brick loads. A stack of rectangular blocks sits on the conveyor section inside the machine frame at the start of the video.
A tall stack of red bricks stands on the conveyor inside the yellow strapping arch, and vertical straps appear on the stack as the clip goes on. Brick stacks travel through the strapping arch rather than being handled by hand.
A tall brick stack is secured while it stands under the strapping head. Later in the video, a bundle of bricks is strapped on the conveyor while several people watch from beside the line.
Each stack stays in the arch while the straps are added. People stand beside the machine throughout the clip.
Къде е подходяща тази машина
The station sits between the stacker and the wrap-or-dispatch point. Fired brick, pressed blocks and foundry ingots all leave a stacker as a stable rectangle, and horizontal strap adds the compression the stack lacks on its own.
Because strapping happens in-line, the load moves from the stacker, through the arch and on toward wrapping or loading without being set down and re-handled. Mixed-product lines benefit most: a tall brick stack and a low pallet of blocks can pass through the same station as long as both fit the arch opening.
How the strapping cycle runs
A typical automatic cycle has four beats. The load indexes into the arch and stops in position. The strap is fed around the bundle — over the top, down the sides and under the conveyor section. The clincher tensions the strap to the set level and closes the seal.
With the strap closed, the knife separates the coil from the finished bundle and the conveyor advances. Each bundle gets the same treatment — the same tension setting, the same seal position, the same strap pattern — which is the practical difference between an in-line strapper and hand strapping.
Staff stand close to the machine in every frame; how the cycle is started, and whether any step is manual, are not shown.
Configured per project
Strapping equipment is configured per project rather than sold as a fixed box. The arch opening is sized to your tallest expected stack, the conveyor height matches the joining line, and strap grade and width follow the weight and edge sharpness of the product.
| Точка | Как е настроено | Единица |
|---|---|---|
| Arch opening | Sized to the tallest stack in your layout | mm |
| Височина на конвейера | Matched to the joining line | mm |
| Ширина на лентата | Selected for load weight and edge sharpness | mm |
| Опън на ремъка | Set per load and confirmed at commissioning | N |
| Метод на запечатване | Chosen per strap type and duty | - |
Seal type, tension range and coil size are specified the same way. A layout drawing is what turns those choices into a concrete proposal, because it shows the infeed height, the direction of travel and the space available around the station. Browse the full equipment range at fhopepack.com.
The cycle numbers below are an illustrative customer example, not a measurement of the machine in the clip. At a 12 s cycle the station straps 300 bundles per hour. If the target is 240 bundles per hour, the cycle budget is 15 s.
| Точка | Стойност |
|---|---|
| Example cycle time | 12 ите |
| Output at a 12 s cycle | 300 пакета/ч |
| Example target output | 240 пакета/ч |
| Cycle budget for that target | 15 ите |
Selection checklist for a strapping station
- Largest stack height and width on this line, plus the pallet or bundle footprint.
- Product family: fired brick, pressed blocks, ingots or other bundled goods.
- How the load arrives: conveyor from the stacker, or hand fed to the arch.
- Strap type and coil stock you already buy, or a grade we should pair with the load.
- Conveyor infeed height, discharge height and travel direction.
- Destination market, so the guarding and e-stop layout is reviewed against the right standards.
Контроли и безопасност
The footage was filmed with staff close to the machine, which is normal for a demonstration recording — it is not a model of how the station should be staffed in production. Plan the layout so the strapping area stays clear during the cycle.
If a strap jam, mis-feed or blocked load needs attention, the machine is stopped at the controls and isolated, with lock-out applied per your site procedure, before anyone reaches toward the arch. Never reach into the strapping area while the machine is powered and able to cycle.
Приложимите стандарти зависят от целевия пазар. За пазарите на CE, ISO 12100 определя метода за оценка на риска, а EN 415-10 обхваща общите изисквания за безопасност на опаковъчните машини.
Често задавани въпроси за инженерство
Q: Which products are a poor match for strap bundling? A: Loose items that cannot be compressed and loads that crush at the edges. Anything that leaves the stacker as a stable bundle is a candidate.
Q: Can the station handle more than the product shown in the clip? A: Yes, provided each product fits the arch opening and tolerates compression. The recipe for each product is selected at the controls.
Q: Can the frame match my conveyor height and travel direction? A: Yes — frame, arch and conveyor interface are built around your line. A drawing showing infeed height and direction is enough to size it.
Q: Which safety references apply? A: It depends on where the machine ships. European deliveries work to ISO 12100 and EN 415-10; other regions follow their own rules.
Q: How quickly can I expect a quotation? A: A layout sketch is enough to begin; the quotation step typically completes in 48 hours, with an optional on-site survey to follow.
Следваща стъпка
We specify a strapping station for your line like this:
- Изпратете вашия чертеж на оформлението with the stack sizes and line details, to info@fhopepack.com.
- Получете предложение в рамките на 48 часа, including the strapping station and the conveyor match.
- Резервирайте оглед на обекта so we confirm the infeed height, the line direction and the space around the arch.
Свързано четене
- Автоматична машина за палетно обвързване за конвейерни линии
- Машина за опаковане на палети с бутилки за многослойни пластмасови бутилки
- Линия за опаковане на нарязани рулони за сервизни центрове: обвързване с лента, опаковане през отвор и подреждане
- Автоматична машина за обвързване на стоманени рулони
- Автоматично решение за пакетиране и обвързване на стоманени тръби
- Автоматична машина за обвързване на стоманени рулони
Източници
- Recorded clip: видеото в YouTube (@stretch Wrapper)
- Original video page: automatic-pet-strapping-machine-for-brickingotspallet
- Standards scope: ISO 12100; EN 415-10
- Срок за представяне на предложението: одобрено от къщата CTA (предложение в рамките на 48 часа)
Последен преглед: 21.09.2026 г.