> **ملخص تنفيذي**
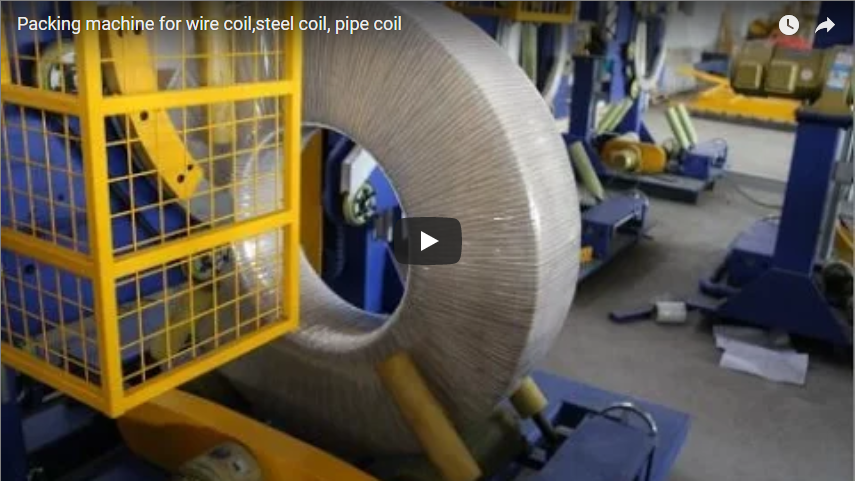
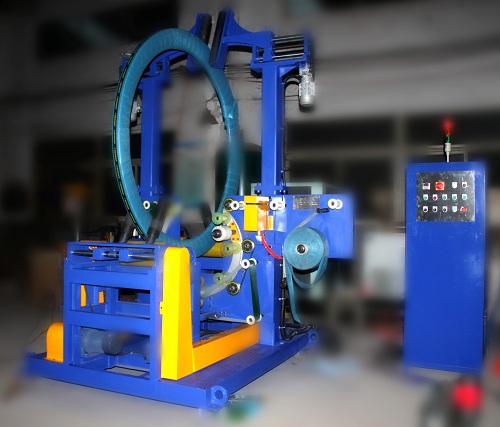
> A two-stage line splits the job in two. Stage one wraps each coil through the eye on a ring wrapper; stage two moves the wrapped coils with an overhead gantry to build stacks. This clip of about one minute shows both stages on our lines. You see a blue ring wrapper with a gantry stacker, a white gantry with a yellow gripper head, and a second ring wrapping a narrow coil.
جدول المحتويات
- الجواب القصير
- ما يُظهره المقطع
- المرحلة الأولى: غلاف الحلقة
- المرحلة الثانية: الجسر العلوي
- ما الذي يحدد وتيرة الخط
- مجموعة لفائف لخطوط التغذية بالناقل
- قائمة التحقق من الاختيارات لخط إنتاج ثنائي المراحل
- الضوابط والسلامة
- أسئلة وأجوبة هندسية
- الخطوة التالية
- القراءة ذات الصلة
- مصادر
الجواب القصير
1. A coil arrives flat on a powered roller conveyor.
2. A ring wrapper passes film through the eye while rollers turn the coil, sealing it all round.
3. The wrapped coil moves on to an overhead gantry.
4. The gantry picks the coil and sets it down on a stack, or on the next station.
5. The finished stack leaves the line on rollers or by forklift.
ما يُظهره المقطع
| Clip time | Scene |
|---|---|
| 0–12 s | A coil lies flat on yellow rollers in a blue vertical ring, which winds clear film through the eye |
| 12–40 s | A blue gantry over the conveyor lowers its gripper arms to a wrapped coil and sets it down |
| 45–55 s | A white gantry with a yellow gripper head travels over a roller platform with yellow fixtures |
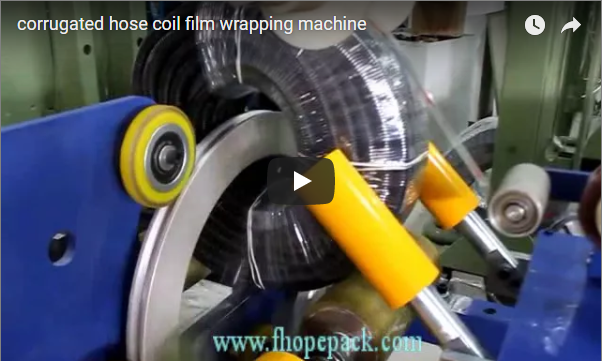
| final seconds | A narrow coil sits in another ring wrapper on green rollers while an operator in an orange hard hat works beside it |
تُؤخذ الأوقات من لقطات مُلتقطة كل 3 ثوانٍ تقريبًا، لذا فإن كل حد تقريبي. المقطع عبارة عن مونتاج، لذا فإن المشاهد مأخوذة من أكثر من سطر.
المرحلة الأولى: غلاف الحلقة
تحمل الحلقة لفة الفيلم وتمرّ عبر فتحة الملف في كل دورة. تقوم بكرات أسفل الملف بتدويره ببطء، بحيث تتداخل كل دورة مع الدورة السابقة. عندما يكمل الملف دورة كاملة، يغطي الفيلم السطح الخارجي والفتحة والجانبين.
في خطوط تعبئة اللفائف لدينا، تقوم برامج PLC/HMI بضبط التمركز والشد والتداخل لكل نوع من أنواع اللفائف. يمكن استخدام غلاف بلاستيكي أو ورقي أو منسوج، ويمكن للخط نفسه إضافة أشرطة PET أو فولاذية وملصق ERP/MES.
المرحلة الثانية: الجسر العلوي
بعد لفّ اللفافة، يجب على خط الإنتاج تحريكها دون إتلاف اللفافة الجديدة. تقوم رافعة جسرية علوية بهذه المهمة من الأعلى، لذا لا تدخل رافعة شوكية أو رافعة عادية إلى خط الإنتاج.
- **The gripper arms close on the outer edge** of the coil, as on the blue gantry in the clip.
- **The carriage lifts the coil straight up**, travels, and lowers it on the stack.
- **The stack grows eye to sky**, up to 6 coils per stack on our automatic coil packing line.
يُظهر الهيكل الأبيض في المقطع لاحقاً رأساً مختلفاً: وحدة ماسكة صفراء تعمل فوق منصة دوارة. صُمم الرأس وفقاً لنطاق اللفائف وطريقة التقاطها، لذا فهو يختلف من مشروع لآخر.
ما الذي يحدد وتيرة الخط
يعمل خط الإنتاج ذو المرحلتين بوتيرة أبطأ محطة فيه. في معظم الخطوط، تكون هذه المحطة إما آلة لف الحلقات، التي تحتاج إلى دورة كاملة للفة، أو الرافعة الجسرية، التي تقوم بعملية رفع وتحرك لكل لفة.
| If the slowest station is | Typical fix |
|---|---|
| ring wrapper | fewer wraps or lower overlap, where the shipment allows |
| gantry stacker | shorter travel, by placing stack positions close to the conveyor |
| outfeed | a buffer conveyor, so the stack can wait for the forklift |
لهذا السبب نطلب عدد اللفات في الساعة في الرسم الأول: فهو يحدد سرعة الحلقة، وحركة الرافعة، وطول المخزن المؤقت معًا.
مجموعة لفائف لخطوط التغذية بالناقل
من جدول نماذج آلات تغليف لفائف الصلب لدينا:
| Model | Coil ID | Coil OD | Coil width | Max coil weight |
|---|---|---|---|---|
| FPCA-1000 | 508 / 610 mm | 700–1600 mm | 20–400 mm | 2000 kg |
| FPCA-1200 | 508–610 mm | 800–1400 mm | 20–500 mm | 2500 kg |
هذه نماذج التحميل على السيور الناقلة للخطوط الآلية. الجدول هو نقطة انطلاق، وليس قائمة كاملة؛ يتم تصميم كل خط وفقًا لنطاق اللفائف للمشروع، لذا قد تتغير الأرقام.
قائمة التحقق من الاختيارات لخط إنتاج ثنائي المراحل
- Coils per hour, including peaks.
- Coil ID, OD, width and weight range.
- Wrap material, overlap and strapping.
- Stack height and stack pattern.
- Space for stack positions and buffer conveyors.
- Labels and data needed for your ERP/MES.
الضوابط والسلامة
تختلف المعايير المطبقة باختلاف السوق المستهدف. ففي أسواق الاستيراد الأوروبي، يحدد معيار ISO 12100 طريقة تقييم المخاطر، بينما يغطي معيار EN 415-10 المتطلبات العامة لآلات التعبئة والتغليف، والتي تحدد إجراءات الحماية وترتيبات إيقاف الطوارئ.
تُشكل الحلقة والرافعة كلاً من المخاطر المتحركة فوق الملف وحوله. وتُحدد دوائر الحماية والإيقاف في تقييم المخاطر لكل تصميم.
أسئلة وأجوبة هندسية
Q: Why use two stages instead of one machine?
A: Because wrapping and stacking can then run at the same time on different coils, and each machine stays simpler.
Q: How many coils go in a stack?
A: Up to 6 coils per stack on our automatic coil packing line, depending on coil weight and handling.
Q: How does the gantry avoid damaging the fresh wrap?
A: Its gripper arms close only on the outer edge and lift the coil straight up, so no forks or slings touch the wrapped faces.
Q: Which coil widths suit a conveyor-fed line?
A: Our FPCA-1000 covers 20–400 mm and the FPCA-1200 covers 20–500 mm.
Q: Can the line label each coil?
A: Yes. ERP/MES labelling is an option on our coil packing lines.
Q: What decides the line speed?
A: The slowest station, usually the ring wrapper or the gantry. Your target coils per hour fixes the cycle time each station must meet.
الخطوة التالية
نخطط لإنشاء خط تعبئة لفائف من مرحلتين في ثلاث خطوات:
1. **Submit your layout drawing** with coils per hour, coil range and stack pattern, to **info@fhopepack.com**.
2. **Receive a proposal within 48 hours**, with the wrapper, gantry and buffer layout.
3. **Book a site survey** so we confirm floor space, stack positions and forklift routes.
القراءة ذات الصلة
- [Slit Coil Stretch Wrapping and Stacking Line: Eye-Through Ring to Gantry Stacker](https://www.fhopepack.com/videos/next-generation-steel-coil-packaging-solutions-integrated-stretch-wrapping-and-stacking-technology/)
- [Two-Stage Copper Coil Packing Line: Eye-Through Wrapping, Then Stacking on Timber Runners](https://www.fhopepack.com/videos/engineering-guide-implementing-a-two-stage-wrapping-stacking-system-for-copper-coils/)
- [Steel Coil Packaging Line from Strapping to Stacking: Five ROI Metrics and a Payback Formula](https://www.fhopepack.com/videos/5-critical-roi-metrics-to-evaluate-a-full-steel-coil-packaging-line-from-strapping-to-stacking-automation/)
- [Automatic coil packing line](https://www.fhopepack.com/Automatic-Coil-Packing-Line/)
مصادر
- Machine in action: [the video on YouTube](https://www.youtube.com/watch?v=VnFMMeGqnSY) (about one minute)
- Up to 6 coils per stack, eye to sky, PLC/HMI centring, tension and overlap, wrap, strap and ERP/MES label options: [Automatic coil packing line](https://www.fhopepack.com/Automatic-Coil-Packing-Line/)
- FPCA-1000 and FPCA-1200 values: [Steel coil wrapping machine](https://www.fhopepack.com/Steel-coil-wrapping-machine/)
- نطاق المعايير: ISO 12100:2010؛ [EN 415-10:2014](https://www.nen.nl/en/nen-en-415-10-2014-en-191845)
- توقيت تقديم المقترح: الموافقة على طلب تعديل المنزل (تقديم المقترح خلال 48 ساعة)
آخر مراجعة: 2026-10-06