ملخص تنفيذي
An automated pallet packaging line integrates vertical strapping, inline document/shipping labelling, and turntable stretch wrapping along a synchronized roller and chain conveyor circuit. The upstream vertical strapper secures loose unstable cylindrical products and their protective carton top caps directly to the pallet structure, while the downstream stretch wrapper applies an environmental barrier against moisture, contamination, and transverse transit shear. Rated at a continuous throughput of 24 loads per hour (with strapper cycles at 15 s per strap), this engineering brief details conveyor elevation matching, right-angle transfer geometry, station takt balancing, film prestretch consumption metrics, and safety interlocks for turnkey project integration.
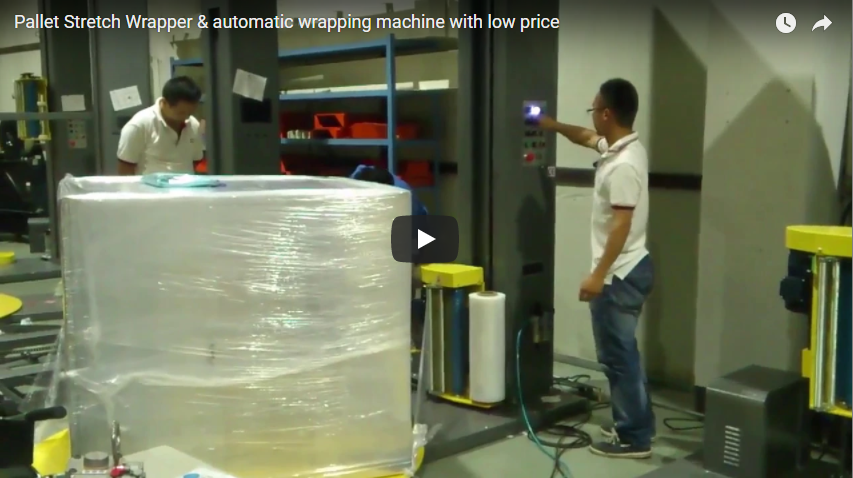
This integrated line processes high-profile cylindrical packages stacked on standard wooden pallets, crowned with rigid protective carton caps. The powered roller bed conveys pallets into a high-tension vertical strapper, diverts loads 90 degrees via an integrated bi-directional chain transfer lift, transitions through an automated data application station, and finishes within an enclosed turntable stretch wrapper cell equipped with automated film clamping, cutting, and heat-wiping systems.
جدول المحتويات
- المحطات، بالترتيب
- بيانات الخط
- لماذا يتم ربط الحزام قبل لفه هنا؟
- عمليات النقل بزاوية قائمة وارتفاع الناقل
- مواعيد المحطات وأسعار الخطوط
- فيلم لكل منصة نقالة بنسبة 250%
- وضع العلامات وإمكانية التتبع
- قائمة التحقق من الاختيار
- سلامة
- أسئلة وأجوبة هندسية
- الخطوة التالية
- القراءة ذات الصلة
- مصادر
المحطات، بالترتيب
- In-feed Powered Roller Conveyor: Accepts unitized loads from upstream production, palletizing cells, or manual loading bays.
- Vertical Pallet Strapper: Drives a strap lance through pallet fork openings or beneath the deck, securing the vertical load stack and top cap under controlled tension.
- Chain Transfer Lift (90° Diverter): Pops up triple-strand chains between drive rollers to change transport direction orthogonally without rotating the pallet.
- Pallet Identification and Labelling Station: Integrates printing, manual inspection, or barcode/RFID print-and-apply applicators.
- Turntable Stretch Wrapper Cell: Enclosed in interlocked safety perimeter fencing; clamps, pre-stretches, wraps, and cuts LLDPE film around the strapped stack.
- Out-feed Accumulation Conveyor: Stages wrapped pallets for forklift retrieval or automated guided vehicle (AGV) transfer.
بيانات الخط
| المواصفات الفنية | Inline Turntable Stretch Wrapper | Vertical Pallet Strapper |
|---|---|---|
| قدرة الخرج | ≥ 24 pallets/hour (continuous) | ~15 s per strap cycle |
| Maximum Load Footprint | 2,200 mm diameter turntable disc | 1,300 mm (W) × 1,800 mm (H) arch |
| Load Weight Rating | 1,800 kg standard (2,000 kg heavy-duty option) | Matched to conveyor design load |
| Conveyor Top of Roller (TOR) | 400 mm nominal datum line | 300–600 mm mechanically adjustable |
| سرعة التشغيل | 0–12 RPM (VFD controlled soft start/stop) | High-speed strap feed at 2.5–4.0 m/s |
| Consumable Specs | LLDPE machine film: 500 mm width, 76 mm core, 17–35 µm | 12–16 mm or 19 mm PET/PP, friction weld |
| نسبة ما قبل التمدد | Powered pre-stretch 250% (options 100% to 300%) | Friction heat-seal joint efficiency ≥ 80% |
| Carriage Vertical Lift Speed | 2.9 m/min via chain/belt hoist | غير قابل للتطبيق |
| الطاقة المركبة للمحرك | Turntable 0.75 kW, rollers 0.75 kW, carriage 0.37 kW, pre-stretch 0.37 kW | 3.0 kW total integrated hydraulic/electric |
| التموين الهوائية | 0.6–0.8 MPa (6–8 kgf/cm²); clean, dried plant air | ضغط النظام 0.6 ميجا باسكال |
لماذا يتم ربط الحزام قبل لفه هنا؟
Strapping prior to stretch wrapping is an engineering requirement for tall, multi-part, or cylindrical product arrays:
- Structural Compaction: The carton top cap and cylindrical products must be compressed and anchored to the structural wooden stringers or blocks before dynamic conveying. Vertical strapping exerts continuous column retention, neutralizing stack shifting during starts and stops.
- Snag-Free Transit: Applying stretch wrap over the finished PET/PP straps encapsulates the strapping bands. This prevents strapping from snagging on conveyor side guides, warehouse racking, or adjacent freight during trailer transit.
- Environmental Encapsulation: A bottom-to-top film wrap seals all open gaps against humidity, airborne contaminants, and road spray, maintaining dry, clean product surfaces beneath the carton cap.
- Sub-Film Traceability: Internal warehouse labels and routing manifests are applied to the carton or stack before wrapping. Trapping labels beneath transparent film prevents abrasion, tampering, and atmospheric degradation while remaining fully scannable by 1D/2D optical readers. Outbound shipping labels requiring direct contact are affixed to the film exterior on the out-feed conveyor.
عمليات النقل بزاوية قائمة وارتفاع الناقل
Conveyor transitions without full circular turntables rely on integrated bi-directional chain transfers:
- Mechanics of Orthogonal Transfer: Pneumatically or electro-mechanically actuated lifting chains sit countersunk below the roller apex. When the pallet trips the photo-eye and halts over the transfer bed, the chains raise 15–25 mm above the roller tangent line, lifting the pallet bottom deck boards and conveying it laterally at 90 degrees.
- Pallet Orientation Compatibility: The transfer chains must support the bottom skid boards perpendicular to the travel direction to avoid deflection or catching. Stringer/block pallet types (GMA, Euro, or industrial four-way) must be mapped during layout engineering to determine chain spacing and quantity (dual, triple, or four-strand).
- Single Datum Line Conveyor Elevation: To eliminate costly drop-sections or incline ramps, all line conveyors share a unified Top of Roller (TOR) elevation of 400 mm. The turntable wrapper frame is engineered for a 400 mm TOR to house internal chain-driven roller cassettes, while the strapper base provides 300–600 mm jacking legs to lock into this 400 mm zero-elevation plane.
مواعيد المحطات وأسعار الخطوط
A line throughput of 24 pallets per hour yields an available gross takt time of 150 seconds per load:
| Station Cycle Component | Time Calculation / Basis | مدة التشغيل |
|---|---|---|
| Gross Available Takt | 3,600 s ÷ 24 pallets/h | 150 ق |
| Vertical Strapper (2 Straps) | 2 bands × 15 s per cycle | 30 s (Wait margin: 120 s) |
| Vertical Strapper (4 Straps + Index) | (4 bands × 15 s) + pallet 90° indexing (15 s) | 75 s (Wait margin: 75 s) |
| Conveyor Transfer & Indexing | In-feed + 90° chain transfer lift and move | 18-25 ثانية |
| Turntable Stretch Wrapper Cycle | Ramp-up (5 s) + 20 revs at 12 RPM (100 s) + cut/wipe (8 s) + ramp-down (5 s) | ~118 ثانية |
| Total Wrapper Station Occupancy | Wrapper cycle (118 s) + pallet load/unload index (20 s) | 138 ق |
Takt Analysis: The inline turntable stretch wrapper is the pacing machine (bottleneck) at 138 seconds total dwell. The vertical strapper completes even a 4-strap reinforcement pattern in 75 seconds, leaving ample buffer capacity. The line comfortably sustains the 24 pallets/hour design target.
فيلم لكل منصة نقالة بنسبة 250%
Consider a standard 1,200 mm × 1,000 mm load, 1,700 mm stack height (within the strapper’s 1,800 mm envelope), using 3 bottom reinforcement wraps and 3 top wraps at 12 RPM. The film carriage travels vertically at 2.9 m/min (48 mm/s). One turntable rotation takes 5.0 s (12 RPM).
| Kinematic & Material Check | Underlying Engineering Formula | القيمة المحسوبة |
|---|---|---|
| Plan Diagonal vs. Turntable | √(1,200² + 1,000²) | 1,562 mm (Fits inside 2,200 mm deck) |
| Vertical Carriage Pitch per Turn | 48 مم/ث × 5.0 ث | 240 mm pitch (52% overlap on 500 mm film) |
| Rotations for Up/Down Pass | 2 × (1,700 mm stack height ÷ 240 mm pitch) | 14.1 turns (rounded to 14 turns) |
| Total Turntable Revolutions | 14 دورات جانبية + 3 دورات سفلية + 3 دورات علوية | 20 ثورة |
| Pallet Perimeter (Mean Path) | 2 × (1.2 م + 1.0 م) | 4.4 m per rotation |
| Total Stretched Film on Load | 20 دورة × 4.4 متر | 88.0 m applied film |
| Pre-Stretch Expansion Ratio | 250% elongation (1.0 m raw = 3.5 m stretched) | Strain factor: 3.50 |
| فيلم خام مأخوذ من لفة | 88.0 m applied film ÷ 3.50 stretch factor | 25.1 م |
| Yield per 1,500 m Film Roll | 1,500 m roll length ÷ 25.1 m per load | ~59 to 60 pallets/roll |
Note: Powered pre-stretch rollers gearing at 250% turn a standard 23 µm film roll into high-tension holding force without neckdown, keeping consumable costs predictable.
وضع العلامات وإمكانية التتبع
The intermediate document and labelling station bridges the strapper and wrapper stations:
- تكامل البيانات: Integrates directly with warehouse management systems (WMS) or programmable logic controllers (PLCs) over Industrial Ethernet (EtherNet/IP, PROFINET). The pallet ticket logs production batch, SKU ID, timestamp, and net weight.
- Sub-Film vs. Outboard Placement: Internal routing slips are applied before the turntable to secure documentation against ambient moisture. If external scanning or courier handoff requires exposed barcodes, a downstream automatic tamp-blown or wipe-on label applicator is positioned at the out-feed roller bed.
قائمة التحقق من الاختيار
Prior to final mechanical sign-off and layout drafting, verify:
- Pallet Matrix: Maximum/minimum width, length, overall height, and total gross load weight.
- Bottom Deck Configuration: Bottom board layout and fork cavity entry (two-way vs. four-way) to configure chain transfer wheel centers.
- تسلسل العملية: Product stability check to justify strap-first or wrap-first order.
- Strap Scheme: Number of straps (2 parallel vs. 4 cross-strapped via turntable index) and band tensile strength (PET vs. PP).
- Layout Envelope: Exact coordinates of line in-feed, right-angle transfer directions, and forklift pick-up stations.
- هدف الإنتاج: Peak and average pallets per hour to size roller VFD drive speeds.
- IT Interface: Barcode label format, data telegram architecture, and ERP/WMS handshaking signals.
سلامة
The complete line is engineered under international packaging machinery safety harmonized standards:
- Machinery Directives & Standards: Designed in compliance with EN ISO 12100:2010 (Risk assessment), EN 415-6 (Pallet wrapping machines), EN 415-8 (Strapping machines), EN 415-10 (Modular packaging lines), and EN 60204-1 (Electrical safety of machinery).
- حراسة المحيط: 2,000 mm high steel wire mesh fencing encloses the turntable rotation radius and vertical strapper lance path. Service access points are equipped with dual-channel category 4 interlock switches.
- Conveyor In-feed/Out-feed Protection: Optical muting light curtains distinguish pallet movement from human personnel intrusion, instantly triggering safety stop circuits (Performance Level d / PLd) without interrupting normal load egress.
- Pinch-Point Mitigation: Chain transfers incorporate full-length internal sheet-metal covers between chains to prevent foot or clothing entrapment.
أسئلة وأجوبة هندسية
Q: Why is vertical strapping completed before stretch wrapping on this line? A: Vertical strapping compacts the carton top cap and vertical product columns securely to the wood pallet. Wrapping afterward seals the entire assembly against weather, eliminates strap snagging during transport, and protects internal barcode documents from being torn.
Q: Can this line handle 30 pallets per hour? A: The turntable wrapper requires ~138 seconds per cycle at 20 turns, capping line throughput at 24–26 pallets/hour. For sustained lines exceeding 30–45 pallets/hour, our engineering team replaces the turntable wrapper with an automatic rotary arm wrapper or rotating ring wrapper.
Q: How do chain transfers navigate Euro pallets vs. industrial GMA pallets? A: The number and spacing of chain strands (typically 2 or 3 strands) are custom-engineered so that the chains lift directly against the flat bottom boards of the pallet rather than the unsupported voids between stringers.
Q: Why maintain a uniform 400 mm conveyor height across all stations? A: A 400 mm Top of Roller (TOR) plane accommodates the structural frame, bearing assemblies, and chain drive transmissions inside both the wrapper turntable and the 90-degree transfer lift without requiring pits in your concrete floor or stepped transitions.
Q: How does the 250% pre-stretch unit reduce operational film costs? A: Dual motorized pre-stretch rollers turn at differential gear ratios, stretching 1.0 meter of film to 3.5 meters before it reaches the pallet. This lowers film consumption to ~25 meters of raw consumable per load compared to manual or core-friction wrapping methods.
الخطوة التالية
- Submit Pallet Specifications: Email your load dimensions (L × W × H), weight range, and target pallets per hour to info@fhopepack.com.
- Layout Engineering: Our packaging systems team will supply an integrated CAD layout drawing matching your floor plan within 24 hours.
- عرض تسليم المفتاح: Receive a full equipment scope, including conveyor drives, strapper lance specs, safety interlocking, and fixed delivery lead times.
القراءة ذات الصلة
- آلة تغليف المنصات الأوتوماتيكية B100 (المنتج)
- آلة ربط المنصات العمودية (المنتج)
- آلة ربط المنصات الأوتوماتيكية في خط التغليف
- آلة تغليف وربط المنصات الأوتوماتيكية من شنغهاي، الصين
- آلة تغليف المنصات الدوارة الأوتوماتيكية
- خط آلات تغليف البليت الأوتوماتيكي بالكامل
مصادر
- FHOPE Equipment Manual: B100 Series Inline Turntable Stretch Wrapper
- FHOPE Engineering Technical Brief: Heavy-Duty Vertical Pallet Strapping Systems
- إن آيزو 12100:2010؛ إن 415-6؛ إن 415-8؛ إن 415-10؛ إن 60204-1