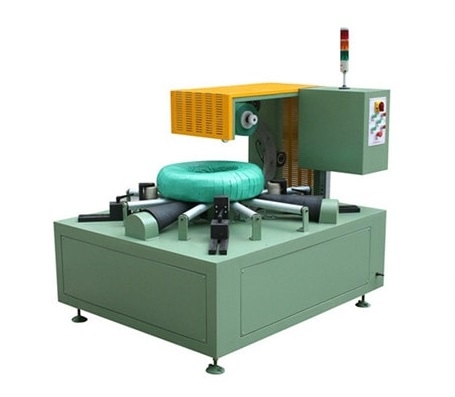
Coil Downender Integration Done Right
Most downender problems are actually misdefined handoffs. This guide treats the downender as an orientation-and-transfer interface, covering arrival state, recovery routes, safety boundary, and acceptance testing.
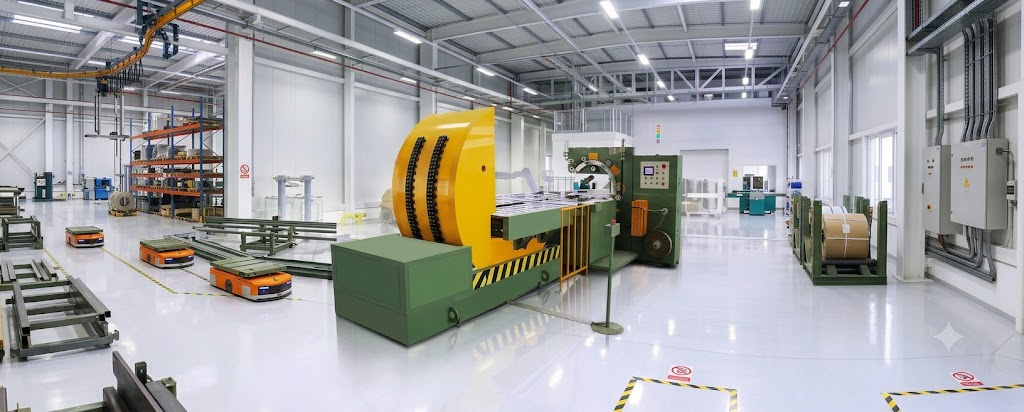
دمج نظام إنزال الملفات: التوجيه والنقل والسلامة
دمج نظام إنزال الملفات: التوجيه والنقل والسلامة
A downender is often described as the device that changes a coil from eye-to-wall to eye-to-sky, or the reverse. That description is true but incomplete. In a real خط تعبئة الملفات الأوتوماتيكي, the difficult part is not only the rotation. It is how the coil arrives, how the orientation change is confirmed, how the next station receives the coil, and how the system stays safe during normal and abnormal conditions.
This guide helps teams define the integration boundary around a coil downender.
Start with the Orientation Requirement
Not every line needs the same orientation at every station. Some coils arrive horizontally and must be packed vertically. Others need the opposite sequence before stacking or shipping. The project should state:
- التوجيه عند الوصول
- Required orientation for the next station
- Product families that follow a different route
- Surface or edge conditions that affect support during turning
Without that map, the downender is chosen before its real process role is understood.
Define the Arrival Condition
The downender only works predictably if the arriving coil is presented in a known position and state. The interface should specify the transfer method, stop position, centering rule, ready signal, and ownership of the coil before the turning action begins.
This matters especially when the coil arrives from a turnstile, conveyor, transfer cart, or crane-assisted handoff. A misaligned arrival becomes a safety and quality issue, not only a cycle loss.
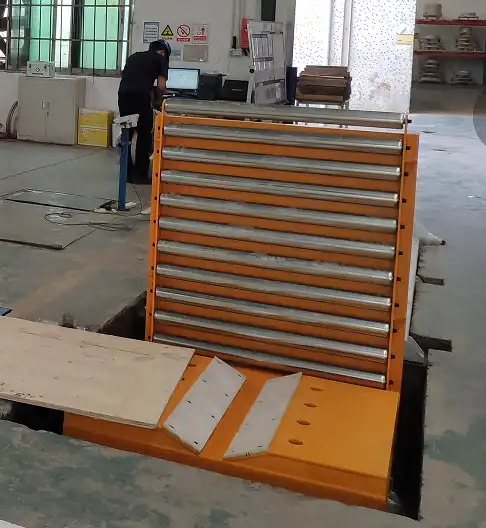
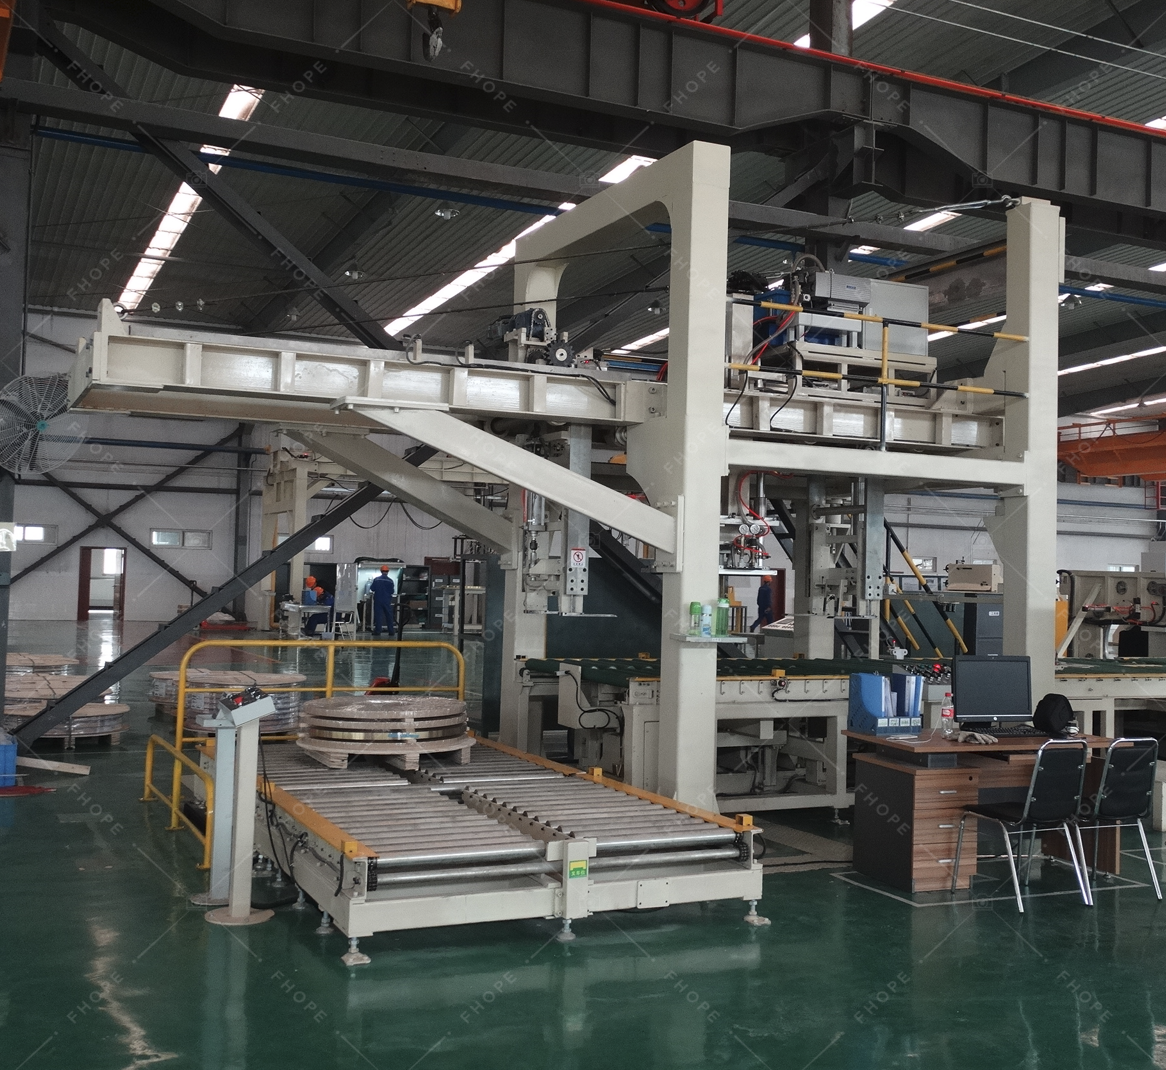
The image shows an upender and tilter with conveyor. Arrival position, centering, and ready signals must be defined before the turning action begins, because the device only works predictably when the coil is presented in a known state.
Confirm the Turned Condition
After the coil is rotated, the line should know more than "motion completed." It should confirm that:
- The coil reached the required orientation
- The coil remains stable on the support surface
- The next station can accept the coil
- No protection layer or sensitive contact point was compromised during turning
That confirmation may include position status, operator checks, or other defined evidence. It should not rely on assumption.

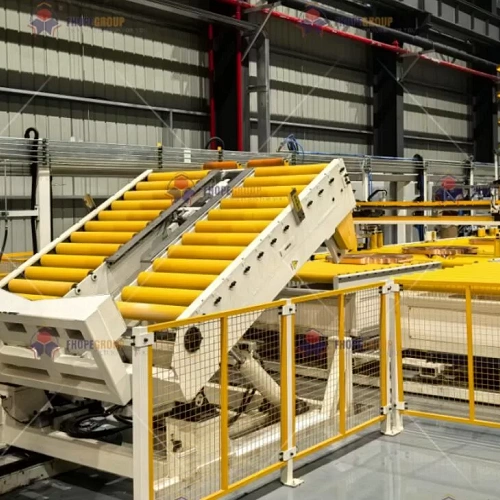
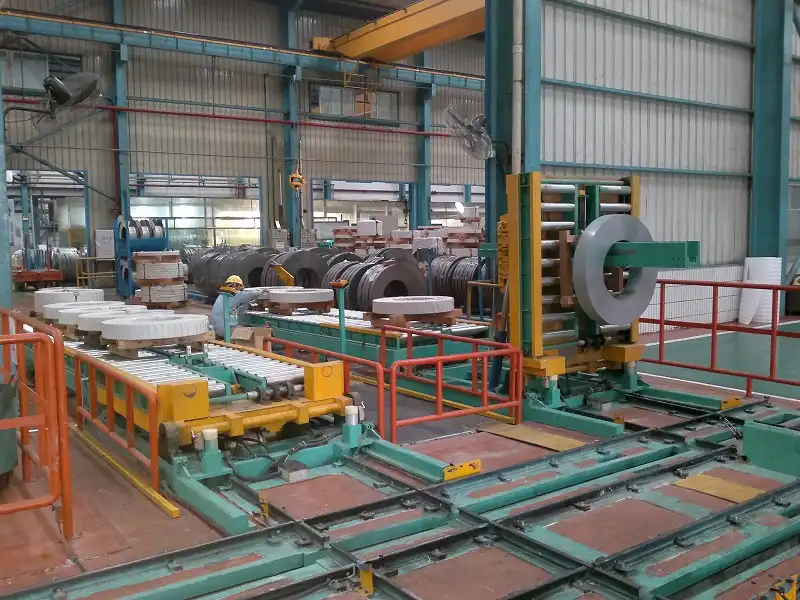
The image shows a steel coil packaging line with vertical handling. After turning, the line must confirm orientation and stability before the coil moves into this downstream handling flow.
Match Transfer on Both Sides
The upstream and downstream stations should be designed with the downender, not after it. Compare support height, loading face, coil centering, clearance, and signal timing at both interfaces. If the turned coil must move into wrapping, strapping, or stacking immediately, the transfer geometry needs to be stable for the full product range.
Many integration problems blamed on the downender are actually misdefined handoffs on either side.
This is why the interface drawing should show not only the turning device, but also the arrival and exit conditions in the same view. Teams make better decisions when they can see the full orientation path instead of three isolated equipment sketches.

The image shows a customized steel coil wrapping line. The turned coil has to enter this downstream station with stable support height, clearance, and signal timing for the full product range.
Watch an automatic heavy-duty steel coil strapping and stretch wrapping line:

Include Surface and Package Protection
The coil may already have a sensitive finish, edge protector, or partial package when it reaches the downender. The integration scope should state whether turning happens before or after certain protective steps, what contact materials are approved, and which product families need additional care.
Turning a coil safely is not enough if the contact method marks the surface or shifts the package build-up.
Make Manual Recovery Deliberate
Downender problems often surface during the rare cases: a coil stops short, a support needs inspection, or the next station rejects the handoff. Those cases should be planned in advance. The document should state how operators approach the area, what isolation or safe state is required, what tools or aids are approved, and who may authorize the return to automatic mode.
If manual recovery is improvised, the line may appear integrated in normal flow and still remain weak where it matters most.
Write the Abnormal Routes
What happens if the coil is not centered, the required orientation cannot be completed, the next station is unavailable, or the line receives a blocked or unidentified coil? Those cases need an explicit route with a safe state, an intervention owner, and a restart condition.
The downender should not become a place where manual judgment replaces system design.
حدد حدود الأمان
Turning changes both the coil position and the hazard envelope. The integration document should identify the protected area, access conditions, interlock behavior, manual recovery method, and restart authority. The safety boundary should cover the shared space around the downender and any adjacent transfer equipment.
A safe design is more than a guarded machine. It is a controlled operating boundary for normal work, recovery, and maintenance.
Test Representative Products and Recoveries
Acceptance should include the normal product families and the more difficult cases: heavier coils, narrower supports, sensitive surfaces, and an interrupted or rejected transfer. Record the arrival condition, turning result, downstream handoff, and controlled recovery evidence.
The test proves the orientation interface, not only the mechanical motion.

The image shows an online slit coil packing line turnkey project. Acceptance for the downender should be tested in this full orientation path, including the difficult products and interrupted transfers that occur in production.
خطوة عملية تالية
Treat the downender as an orientation-and-transfer interface. Write one sheet that defines arrival state, turned state, protection method, abnormal routes, adjacent handoffs, and safety boundary. Review that sheet with operations, engineering, and the supplier before the خط تعبئة الملفات الأوتوماتيكي sequence is frozen.
التفاصيل المرئية

اضغط للتكبير
اضغط للتكبير

اضغط للتكبير
اضغط للتكبير
شاهد كيف يعمل
اكتشف كيف تُحسّن حلول التعبئة والتغليف الآلية لدينا كفاءة خط إنتاجك. يُظهر هذا الفيديو عملية التشغيل السلسة المصممة لتوفير أقصى حماية.
موثوق بها من قبل مصانع الصلب ورواد الصناعة
يعتمد المصنعون العالميون على معدات التعبئة والتغليف الثقيلة من FHOPE


هل أنت مستعد لتحسين خط التعبئة والتغليف الخاص بك؟
احصل على عرض سعر مخصص مع تحليل العائد على الاستثمار. سيرد مهندسونا خلال 24 ساعة.
- تصميم تخطيط مجاني
- دعم التركيب العالمي
- ضمان لمدة سنة متضمن
معلوماتك آمنة ولن تتم مشاركتها أبداً.
الآلات ذات الصلة
خط تغليف لفائف الصلب
عرض التفاصيل →
خط تعبئة ملف عمودي
عرض التفاصيل →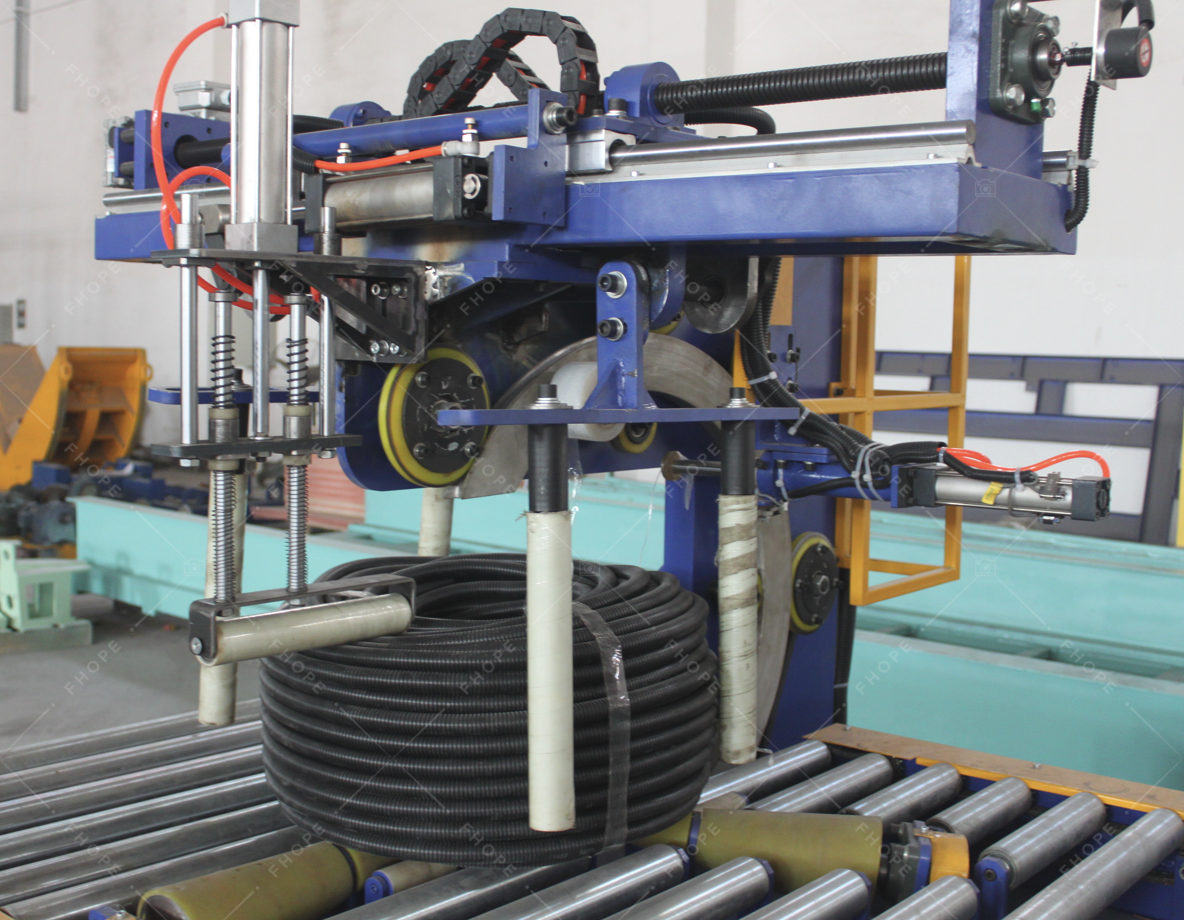
خط تعبئة لفائف الخرطوم
عرض التفاصيل →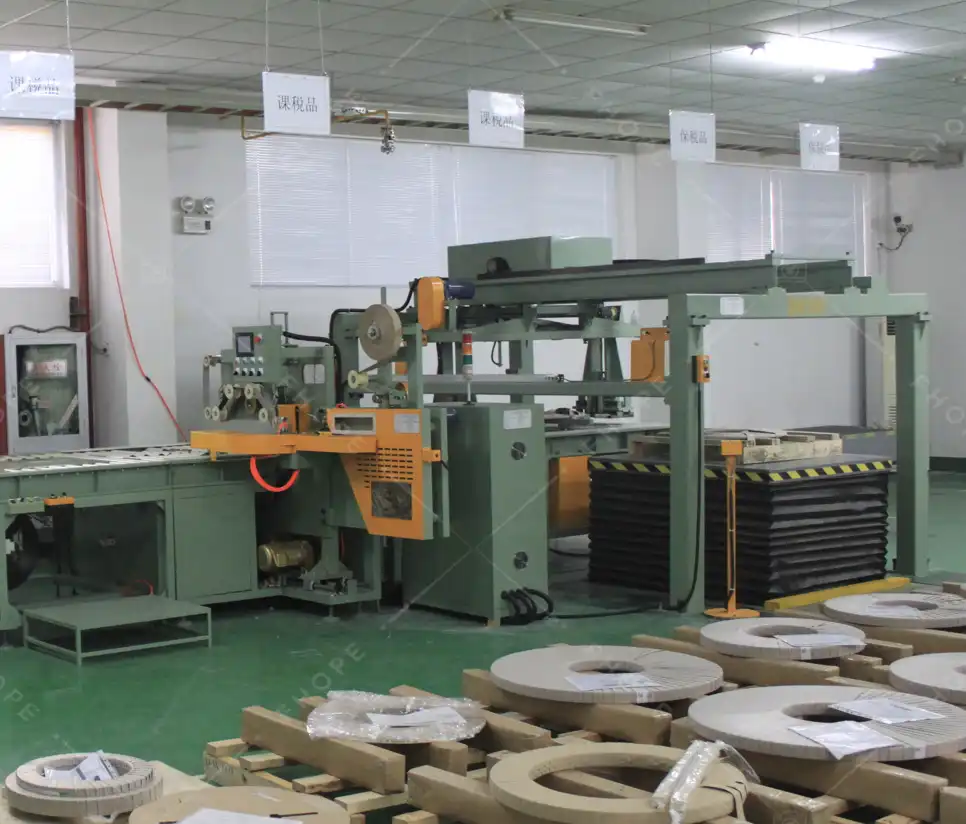
خط تغليف لفائف النحاس
عرض التفاصيل →
خط تغليف لفائف الأسلاك
عرض التفاصيل →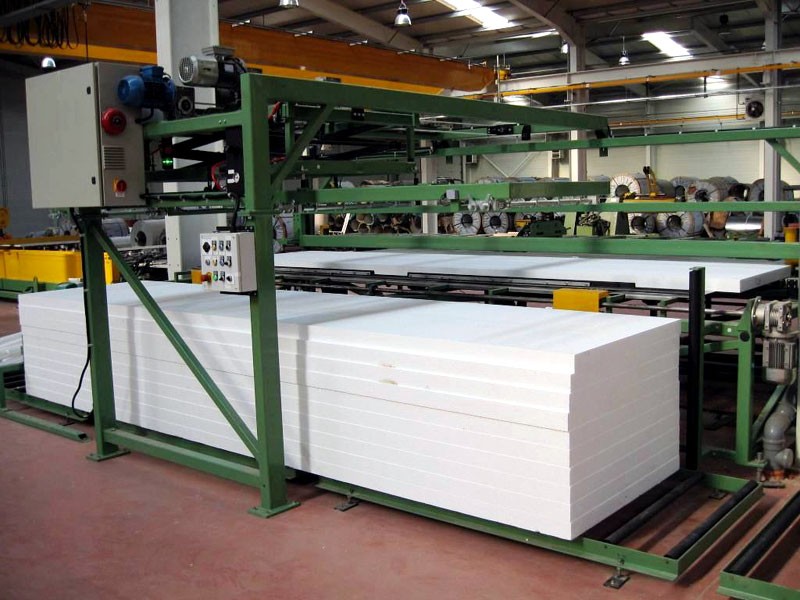
خط تغليف الألواح
عرض التفاصيل →
آلة تعبئة الأنابيب
عرض التفاصيل →
خط تعبئة مقاطع الألمنيوم
عرض التفاصيل →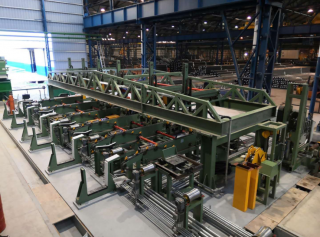
خط تجميع وتغليف مواسير أوتوماتيكي FHOPE
عرض التفاصيل →
خط تجميع وربط الأنابيب الأوتوماتيكي
عرض التفاصيل →
آلة ربط الأنبوب الفولاذي الأوتوماتيكية
عرض التفاصيل →
آلة تعبئة أنابيب الصلب الأوتوماتيكية FHOPE
عرض التفاصيل →
خط تعبئة ربط الأنابيب البلاستيكية الأوتوماتيكي
عرض التفاصيل →
خط تعبئة أوتوماتيكي لأنابيب PPR / PVC
عرض التفاصيل →
آلة تعبئة الأكياس البلاستيكية
عرض التفاصيل →
آلة تعبئة الإطارات FPT-200
عرض التفاصيل →
آلة تعبئة الإطارات FPT-300
عرض التفاصيل →
آلة تعبئة الإطارات FPT-400
عرض التفاصيل →
آلة تغليف ملف الكابلات- FPCA100
عرض التفاصيل →